Conveyor Machine Manufacturers in Maharashtra
- Home
- Conveyor Machine
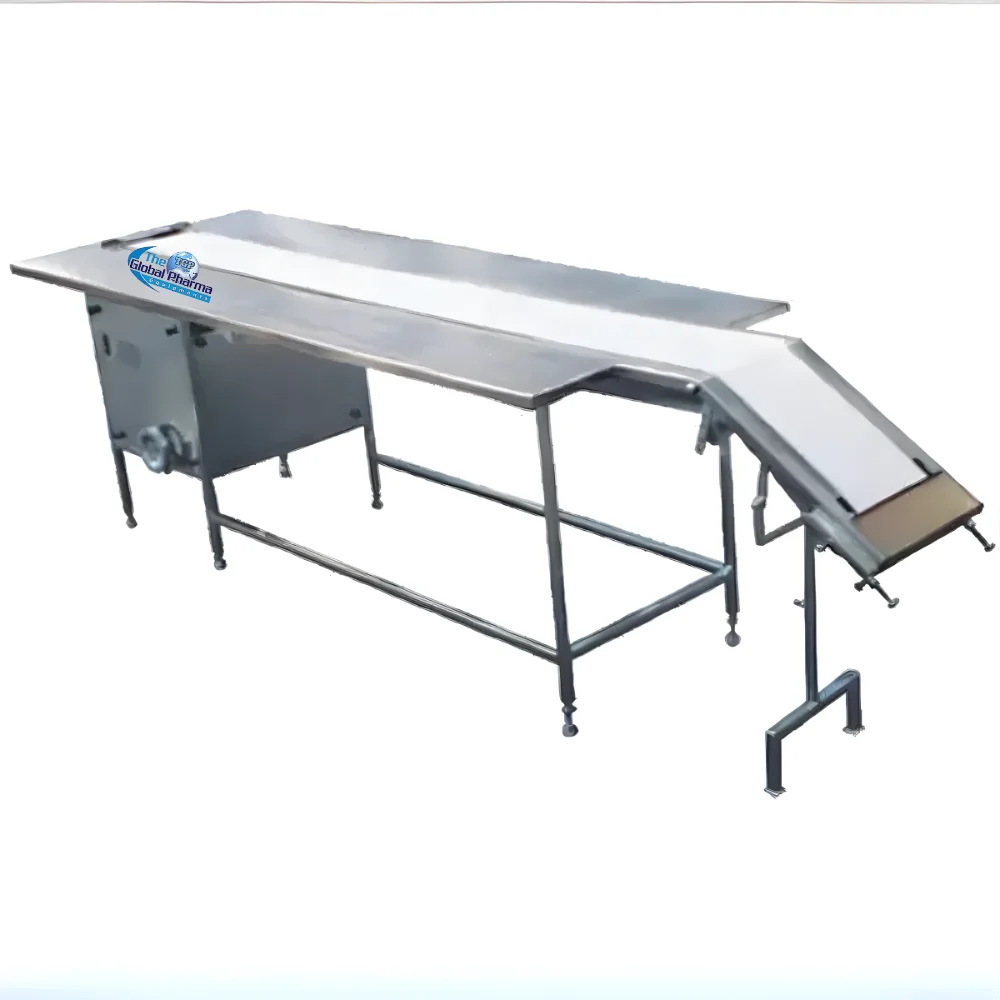
Efficient movement of materials, components, packages, and finished products is essential for maintaining streamlined production and logistics operations. As Conveyor Machine Manufacturers in Maharashtra, we manufacture high-quality conveyor machines designed to simplify material transportation across manufacturing facilities, warehouses, packaging units, processing plants, logistics centers, and industrial workplaces. These machines help reduce manual handling while supporting consistent movement between different operational stages.
Every conveyor machine is manufactured using quality materials, precision engineering, reliable drive components, and sturdy structural frameworks. The equipment can be configured according to material characteristics, load capacity, transportation distance, operating speed, and specific workflow requirements.
Advanced Conveyor Machine Solutions for Streamlined Production
A Conveyor Machine provides an efficient solution for transporting materials between production, processing, packaging, storage, and dispatch areas. Continuous movement helps reduce unnecessary manual transportation while supporting a more organized workflow.
Depending on the application, conveyor machines can incorporate different belt widths, conveyor lengths, drive mechanisms, roller arrangements, frame structures, and operating speeds. These configurations allow the equipment to be adapted to different industrial production and material handling requirements.
Conveyor machines can also be integrated with Pharma Trolleys, Stainless Steel Drum Trolleys, SS Sieve Trolleys, Transfer Trolley Systems, and Mobile Stainless Steel Trolleys to support broader material handling operations.
Dependable Conveyor Machine Suppliers in India for Diverse Industries
As dependable Conveyor Machine Suppliers in India, we provide material transportation equipment for manufacturing companies, warehouses, packaging facilities, food processing units, pharmaceutical industries, logistics centers, engineering plants, and other industrial establishments.
Key advantages include:
- Efficient material transportation
- Continuous operating capability
- Heavy-duty structural construction
- Reliable drive mechanism
- Smooth material movement
- High load-bearing capacity
- Reduced manual handling
- Space-efficient design
- Easy maintenance
- Customized configurations
These advantages make conveyor machines suitable for industrial environments requiring reliable and organized material transportation.
Engineered Conveyor Machines for Continuous Material Flow
Conveyor machines are engineered to simplify the movement of materials across different stages of industrial operations. Their continuous transportation capability helps maintain a consistent workflow while reducing physical effort and unnecessary movement.
The machine configuration can be selected according to available floor space, material characteristics, required transportation distance, load capacity, and production requirements. Suitable belt, roller, drive, and support arrangements can be incorporated according to the intended application.
Experienced Conveyor Machine Exporters in India
As experienced Conveyor Machine Exporters in India, we manufacture conveyor equipment designed for demanding industrial applications. Each machine undergoes systematic quality inspections to verify structural integrity, dimensional accuracy, component alignment, drive performance, and overall functionality.
Quality checks are conducted on the conveyor frame, belt or roller arrangement, drive mechanism, support structure, fasteners, and surface finishing before dispatch. This quality-focused approach helps ensure consistent performance for domestic and international customers.
Different Conveyor Machine Configurations for Industrial Applications
We manufacture a versatile range of conveyor machines suitable for different material transportation requirements.
Our product range includes:
- Belt Conveyor Machines
- Roller Conveyor Machines
- Gravity Conveyor Machines
- Powered Conveyor Machines
- Industrial Conveyor Machines
- Material Handling Conveyor Machines
- Packaging Conveyor Machines
- Inclined Conveyor Machines
- Flat Belt Conveyor Machines
- Customized Conveyor Machines
Each machine can be customized according to conveyor length, belt width, load capacity, operating speed, frame configuration, and material handling requirements.
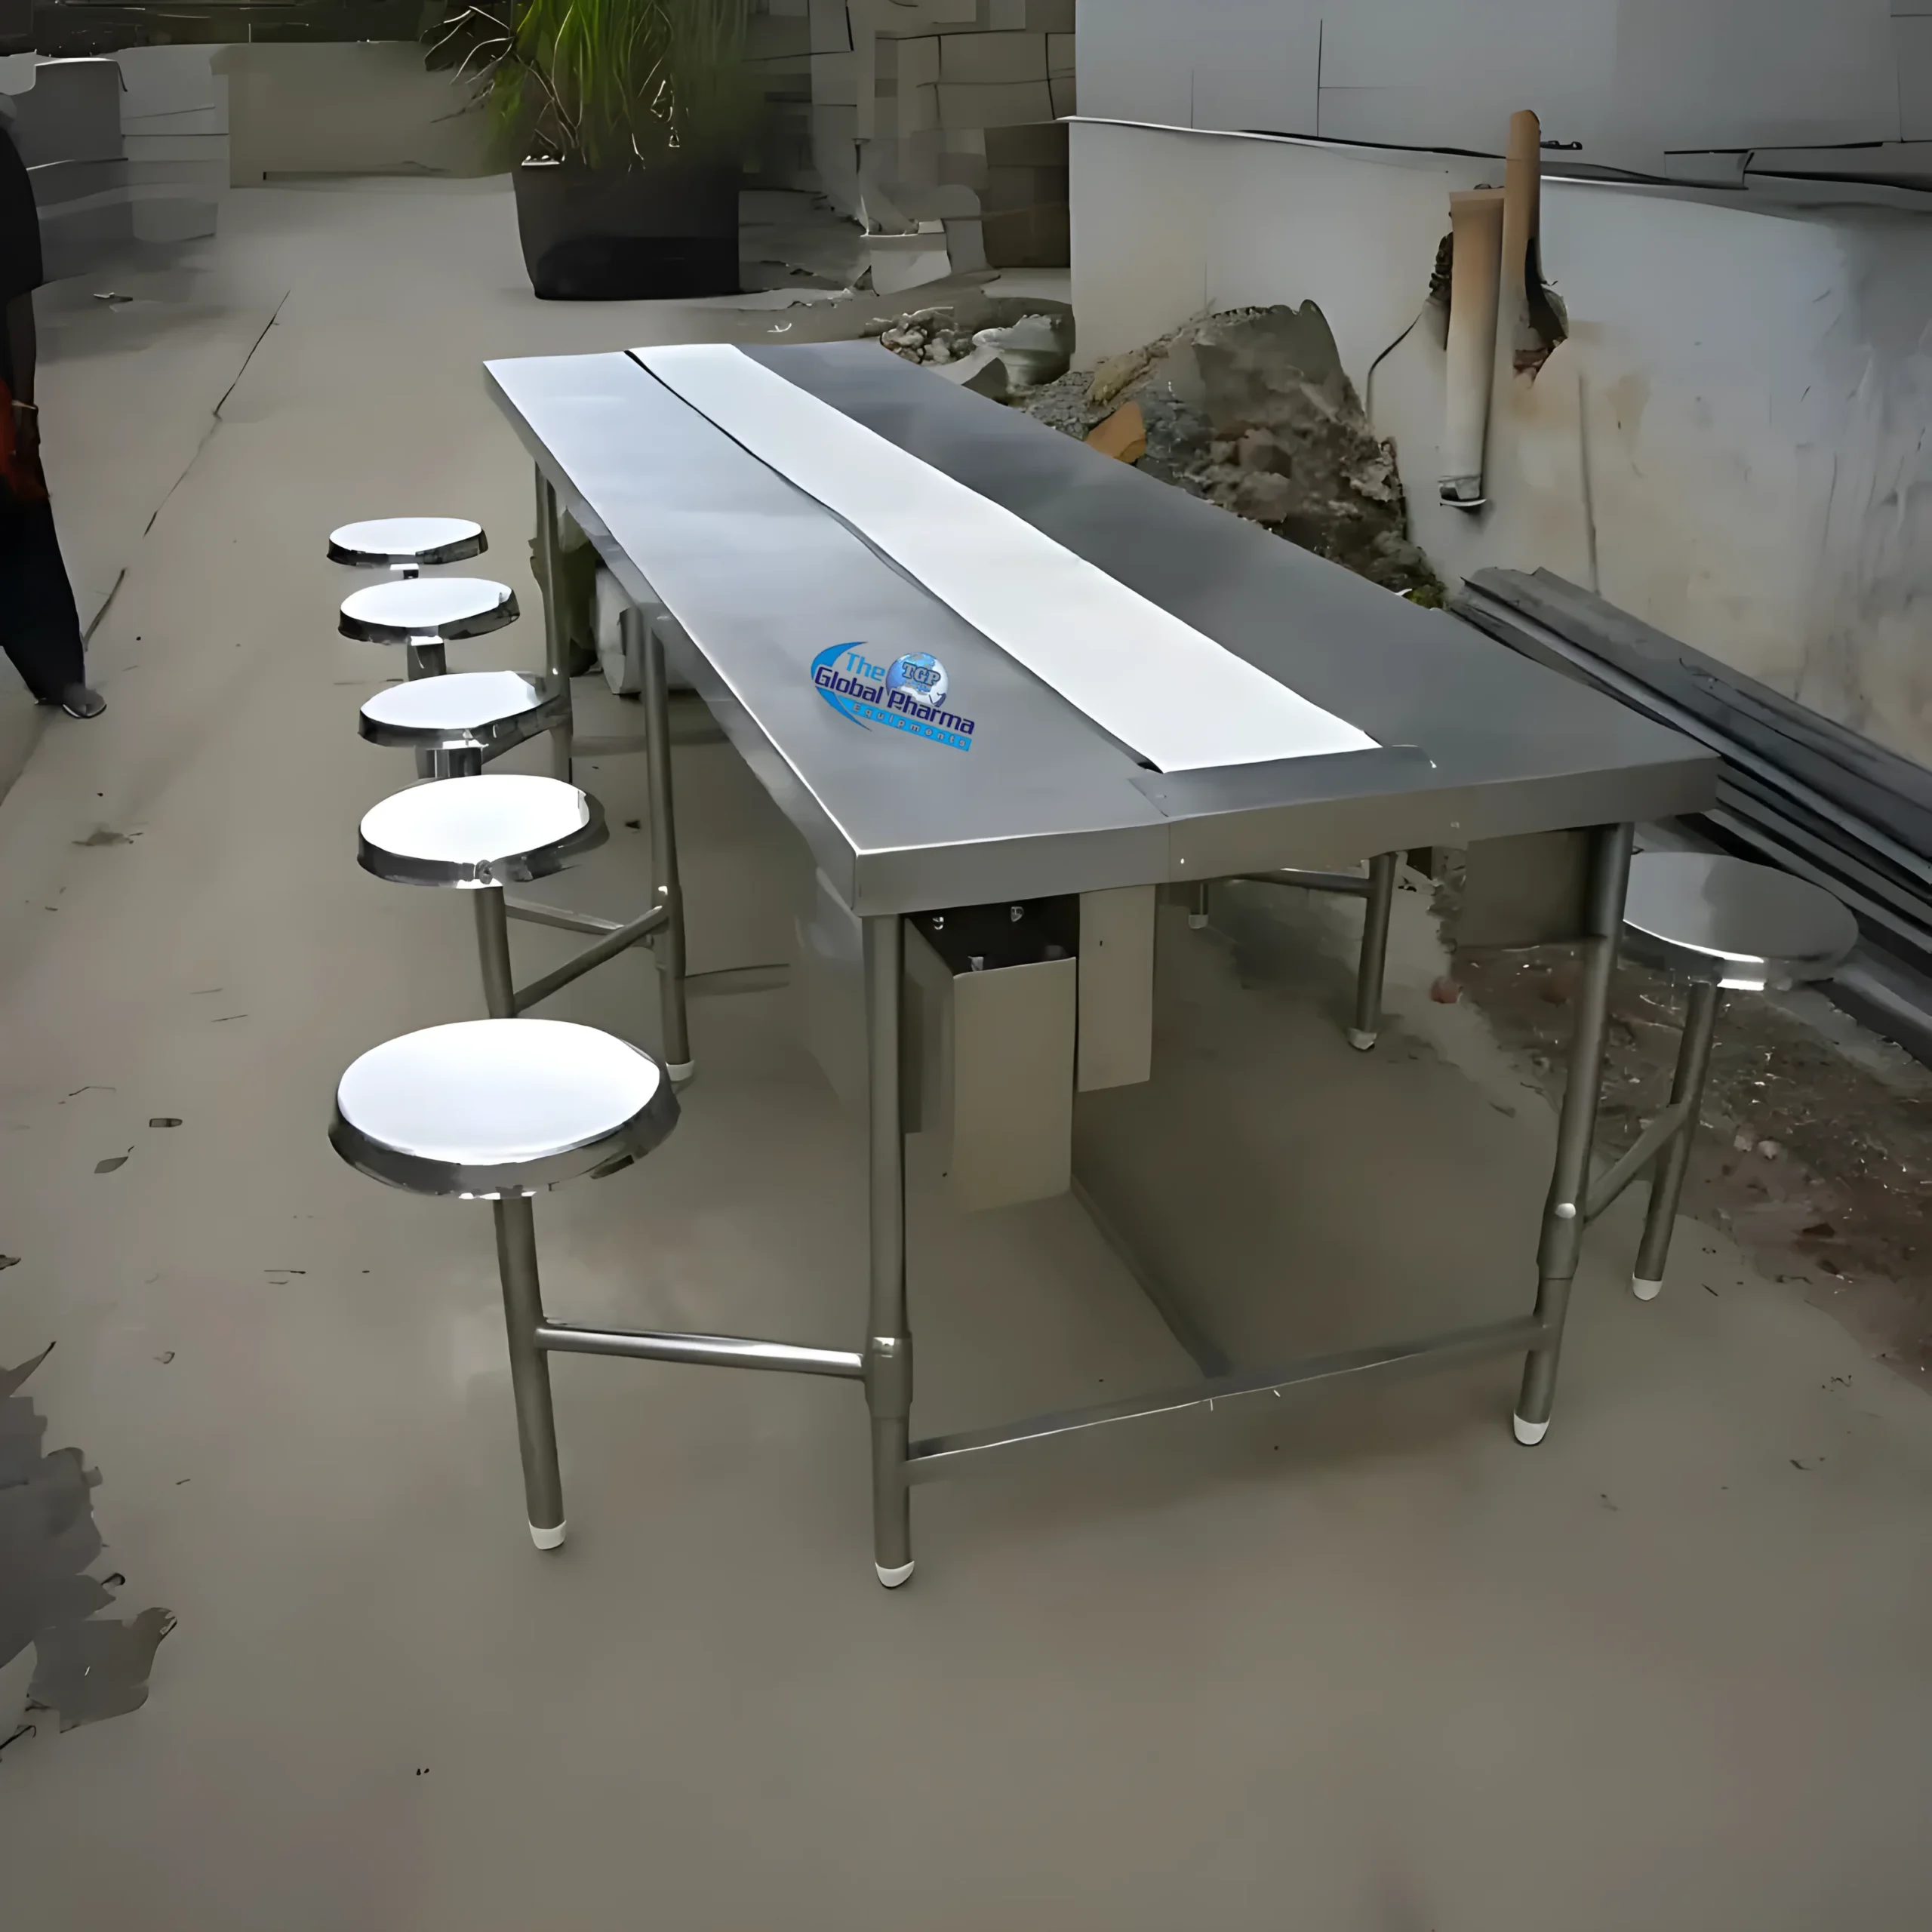
Technical Features Supporting Efficient Conveyor Operation
Every Conveyor Machine is manufactured using quality materials and precision engineering processes to provide dependable performance during regular industrial operations.
Key features include:
- Heavy-duty structural framework
- Durable conveyor belt or roller system
- Reliable drive mechanism
- Smooth material transportation
- High load-bearing capability
- Stable support structure
- Precision component alignment
- Efficient power transmission
- Easy maintenance
- Compact configuration options
- Customized dimensions available
- Long operational lifespan
These features make conveyor machines suitable for manufacturing, packaging, processing, warehousing, logistics, and industrial material handling applications.
Precision-Built Conveyor Machines for Consistent Performance
Every Conveyor Machine is manufactured using quality raw materials, precision fabrication, controlled assembly, and reliable mechanical components. Particular attention is given to frame alignment, belt or roller positioning, drive arrangement, support structure, and dimensional accuracy.
Strict quality control procedures are followed throughout manufacturing to maintain consistent construction and reliable operation. Finished machines are inspected for component alignment, drive functionality, movement, stability, and overall workmanship before dispatch.
Industrial Applications of Conveyor Machine Systems
Conveyor machines are widely used in:
- Manufacturing facilities
- Warehouses
- Packaging units
- Food processing plants
- Pharmaceutical industries
- Logistics and distribution centers
- Engineering industries
- Automotive manufacturing facilities
- Production lines
- Storage facilities
- Material handling areas
- Dispatch and loading areas
Their versatile design allows them to transport raw materials, components, cartons, packages, containers, and finished products across different operational areas.
Reasons to Select Our Conveyor Machine Solutions
- Heavy-duty construction
- Efficient material transportation
- Smooth continuous operation
- High load-bearing capacity
- Reliable drive components
- Precision fabrication
- Customized machine configurations
- Easy maintenance
- Space-efficient designs
- Strict quality inspection
- Competitive pricing
- Long operational lifespan
These advantages make our Conveyor Machine Manufacturers a reliable choice for manufacturing plants, warehouses, packaging facilities, logistics centers, processing units, and industrial organizations.
Maintaining hygiene and ensuring convenient access to medical waste collection c...
Creating a safe and comfortable environment for newborns is essential in hospita...
A well-designed bedside table enhances patient comfort by keeping medicines, mea...

Safe and timely medicine distribution is essential for ensuring quality patient ...
Proper storage is essential for maintaining hygiene, safety, and efficiency in h...
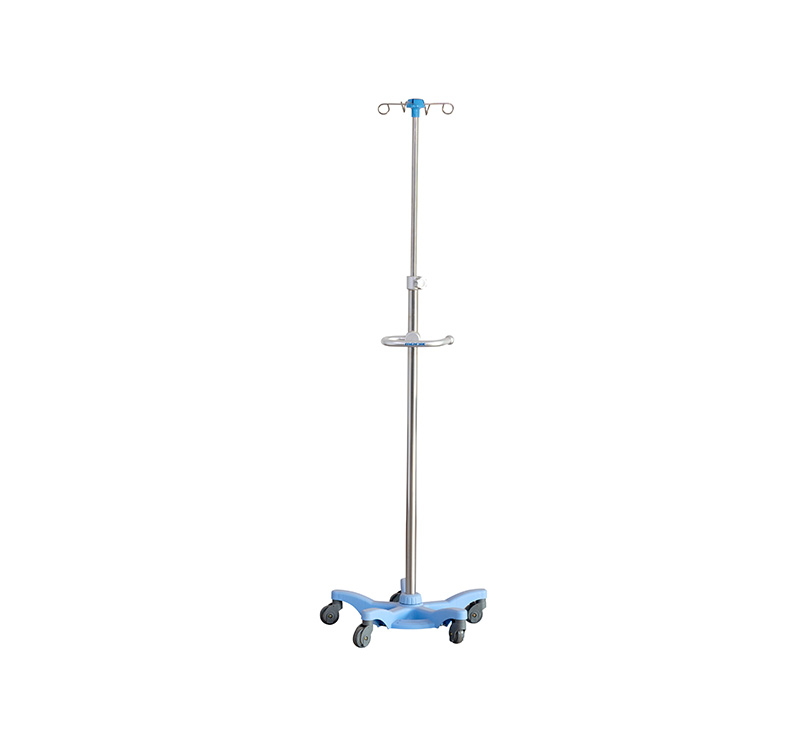
Safe and efficient intravenous therapy requires stable and durable support syste...
Medical instrument trolleys are essential for the safe transportation and organi...
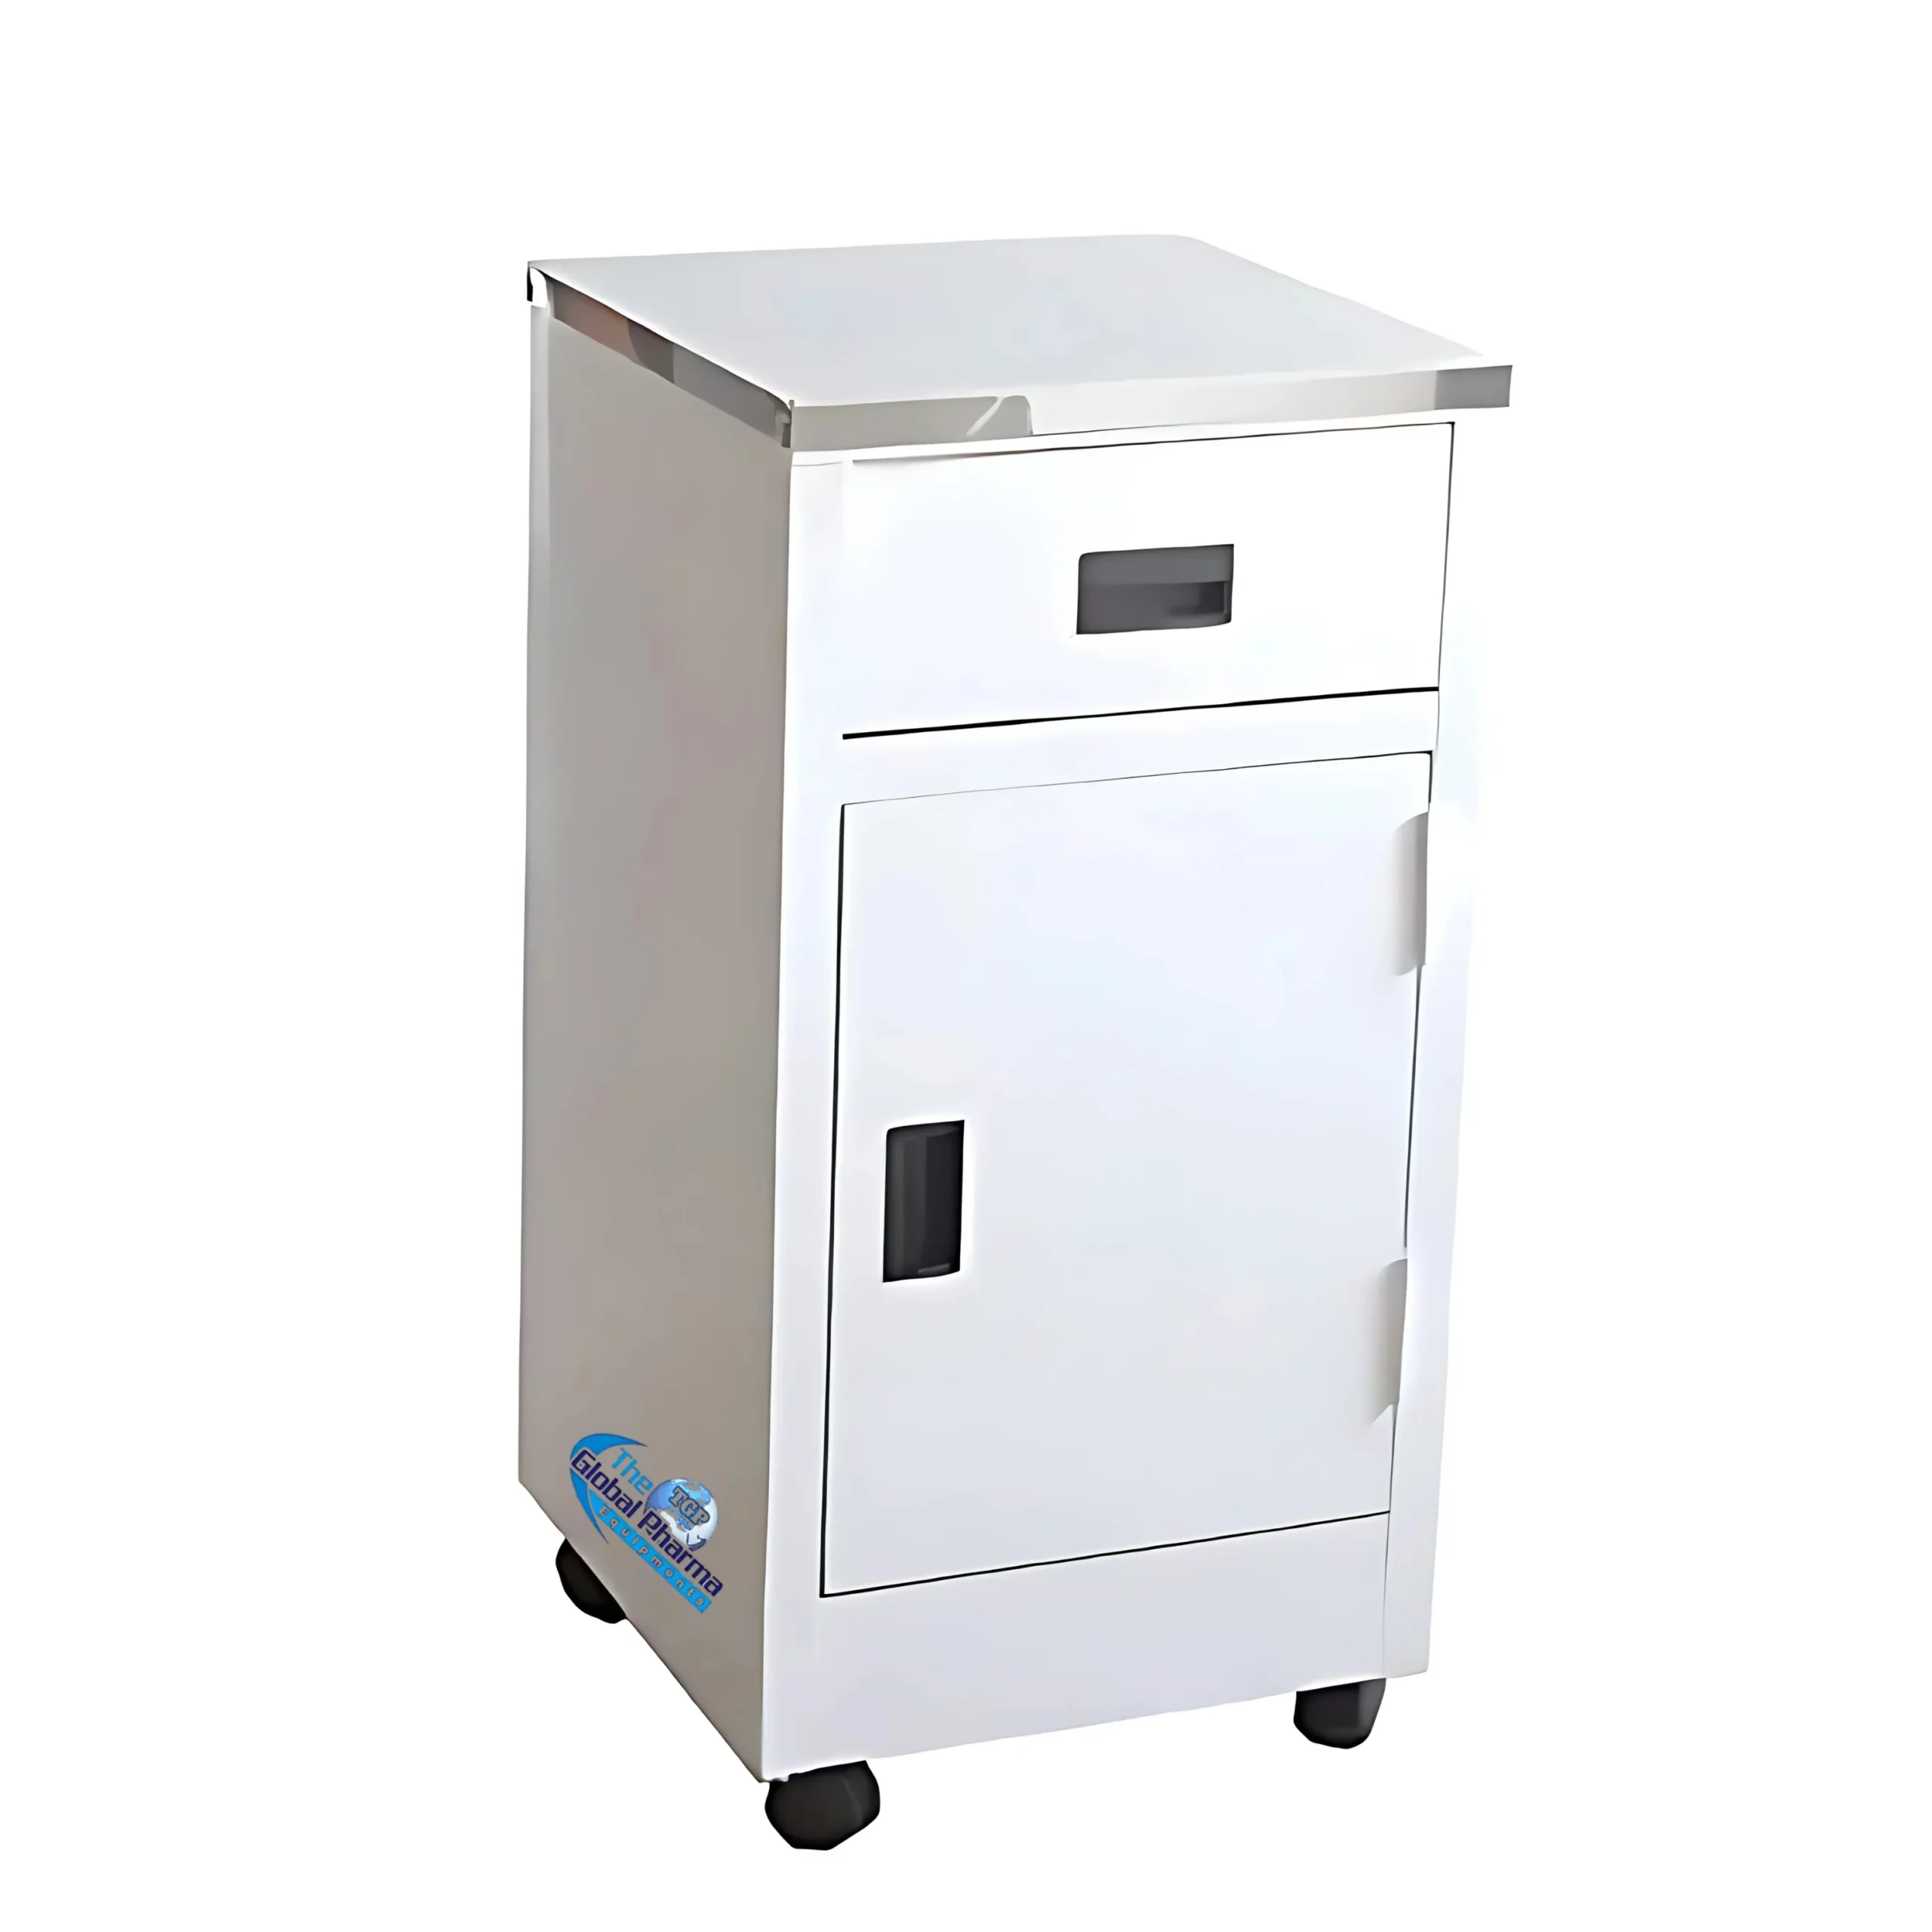
Well-designed bedside lockers help hospitals maintain an organized and comfortab...
Maintaining accurate patient records is essential for smooth hospital operations...
Comfortable and durable hospital beds play a vital role in ensuring proper patie...
Providing a safe and comfortable environment for patients requiring isolation is...
Reliable hospital utility equipment plays a vital role in maintaining hygiene an...
Reliable hospital furniture plays an essential role in supporting patient care a...
Proper storage is essential in hospitals and healthcare facilities to keep perso...
Proper storage of medicines and healthcare supplies is essential for maintaining...
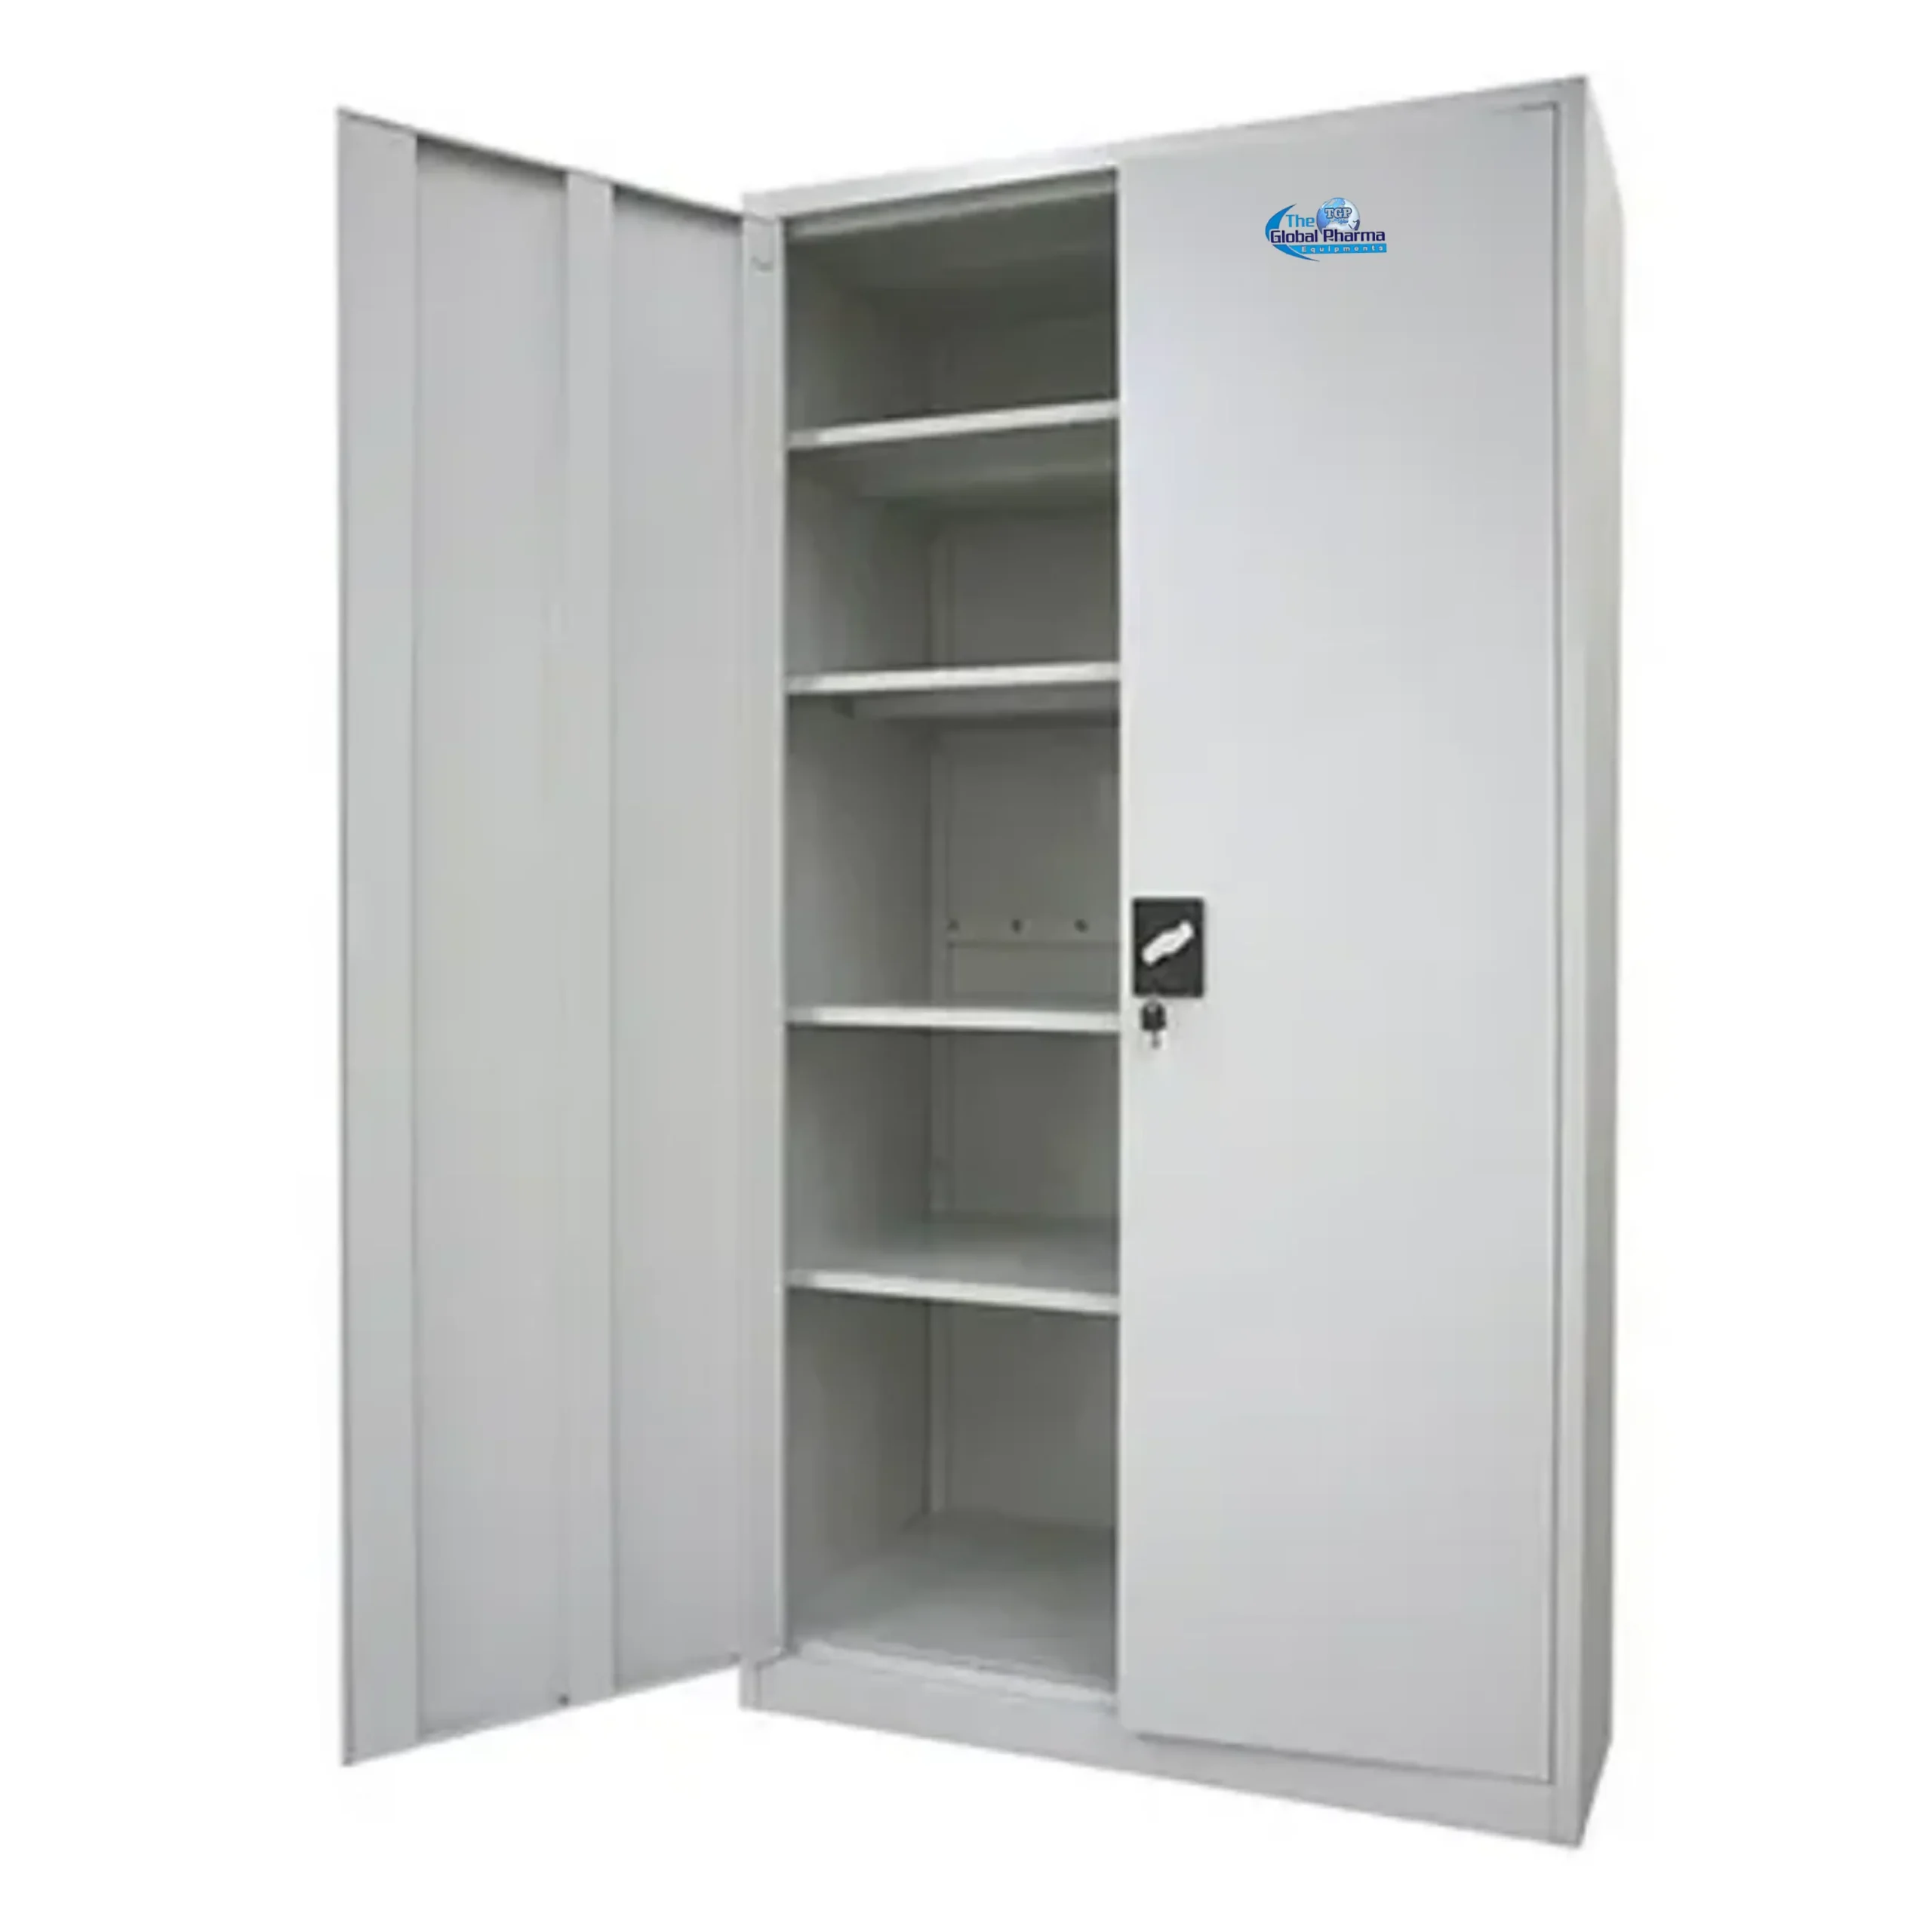
Well-organized storage is essential for maintaining hygiene, efficiency, and acc...
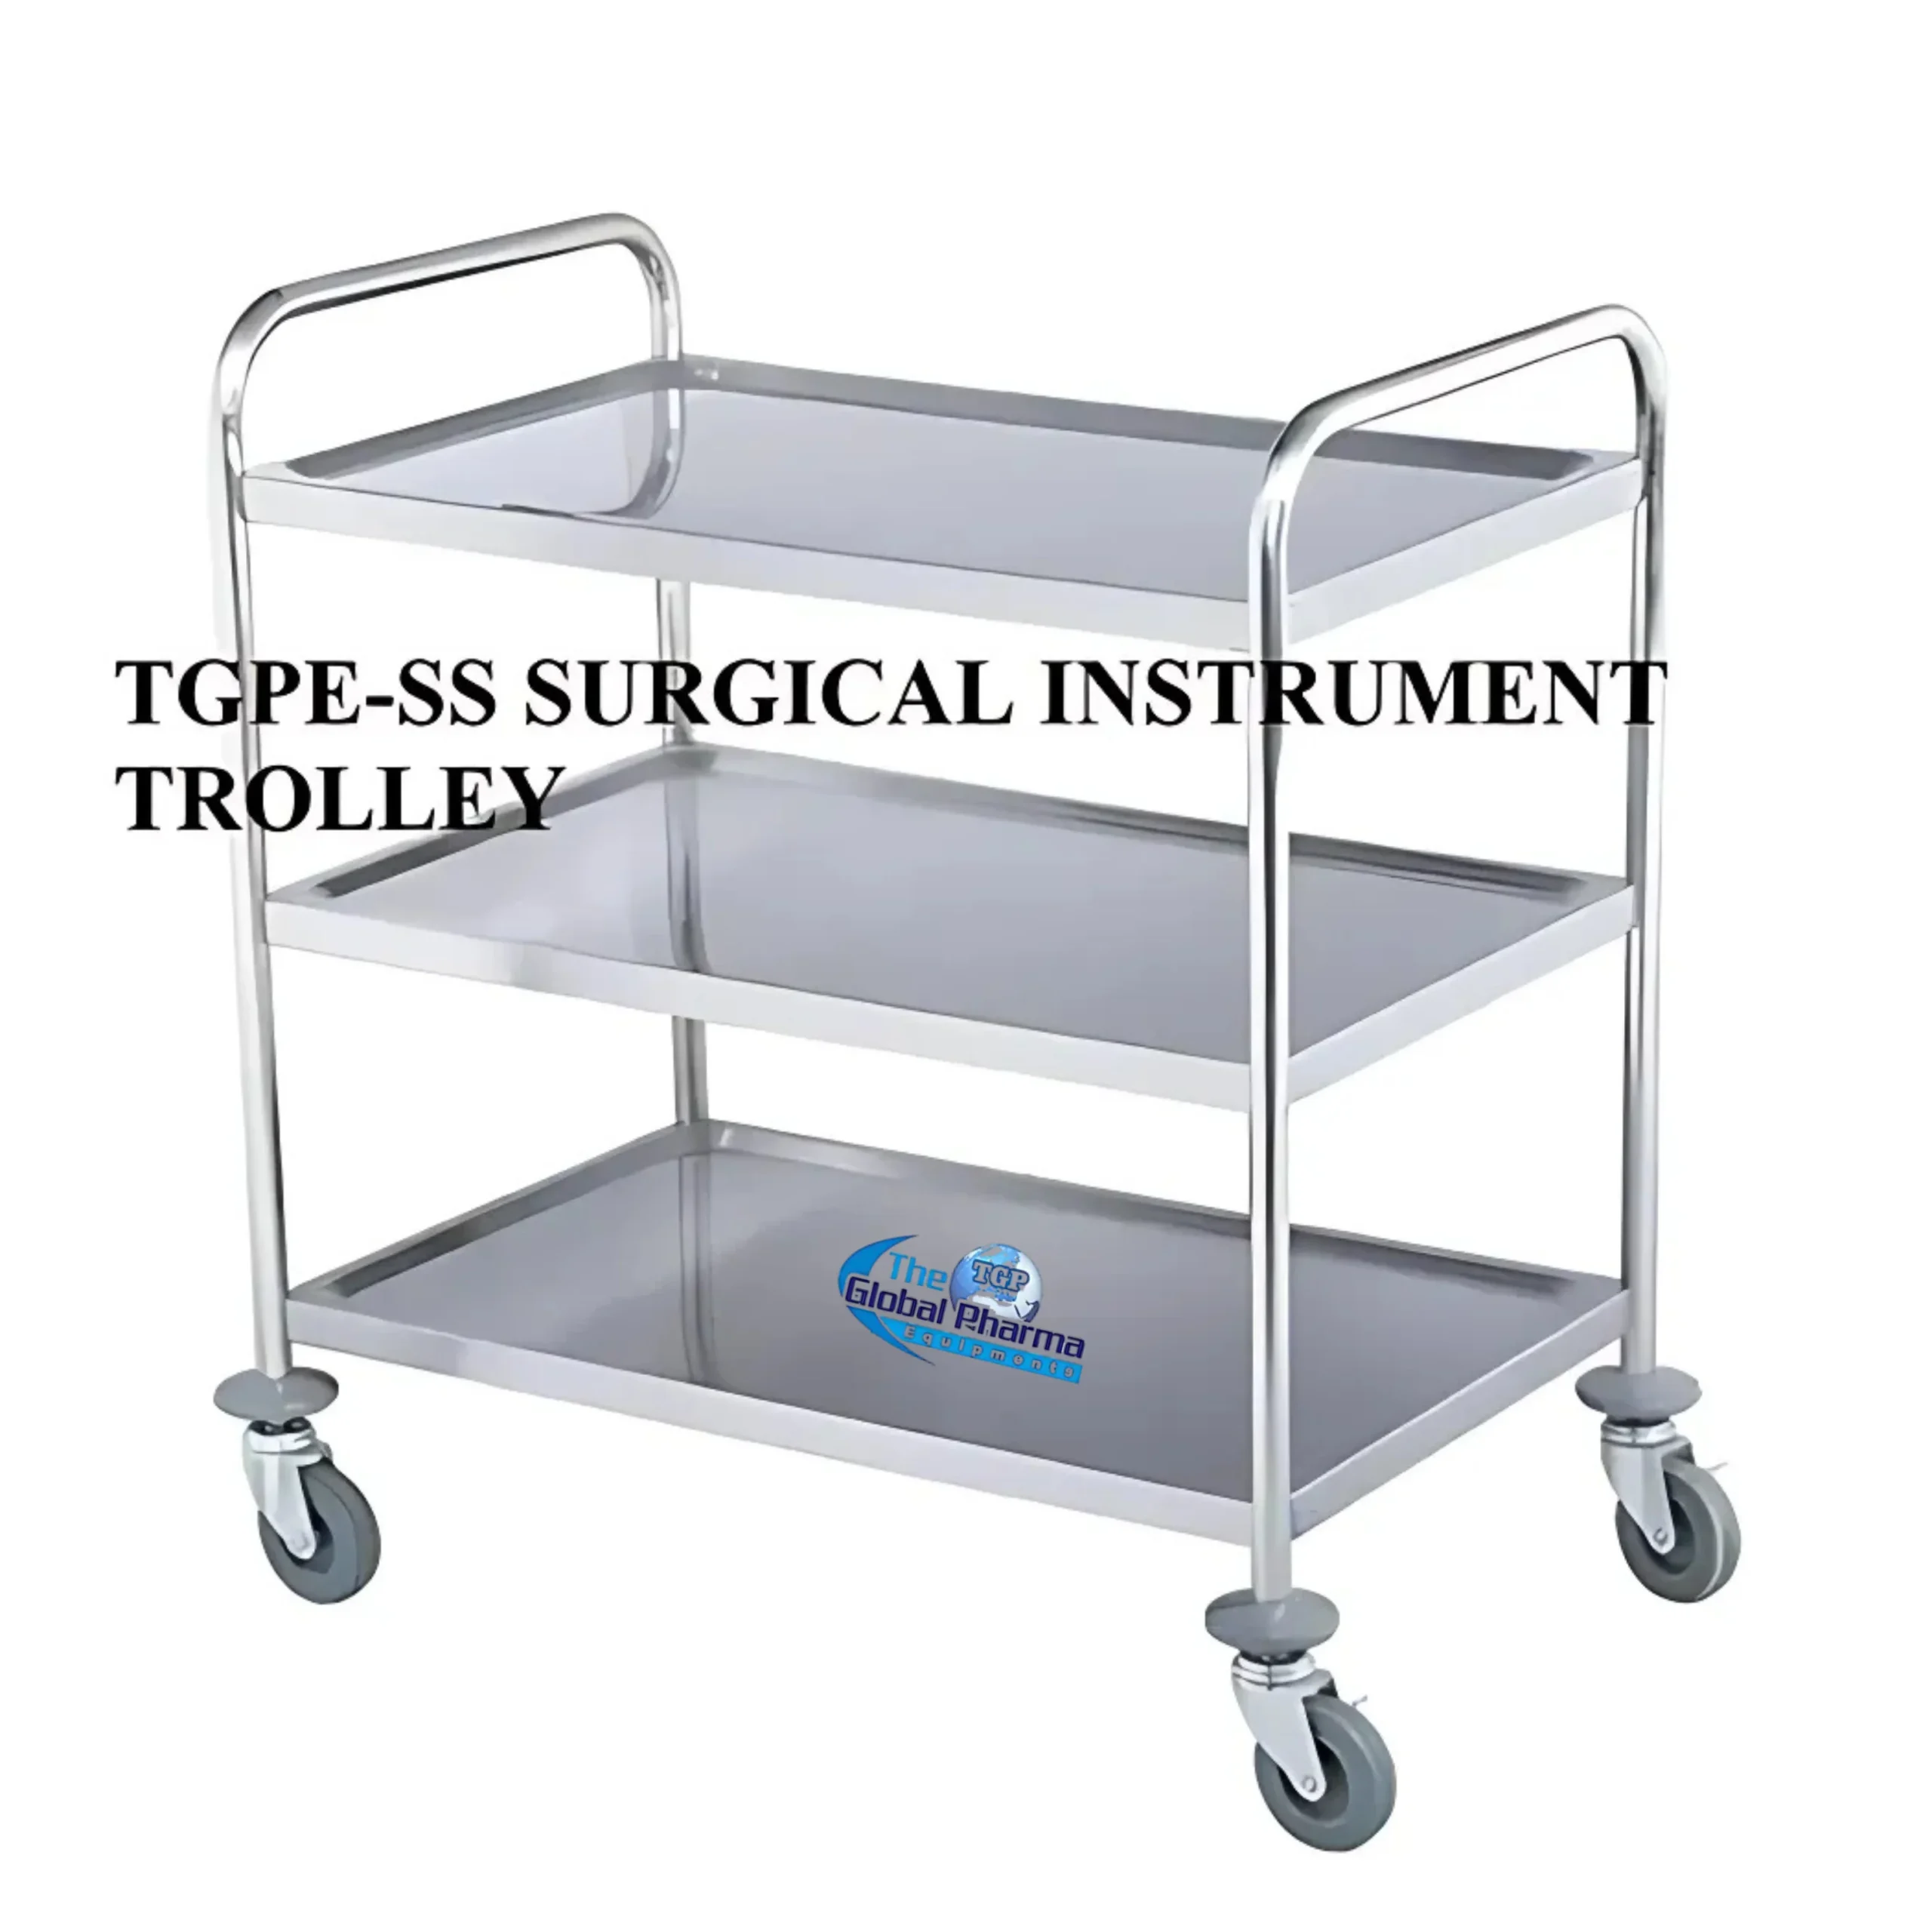
Safe handling and organized transportation of surgical instruments are essential...
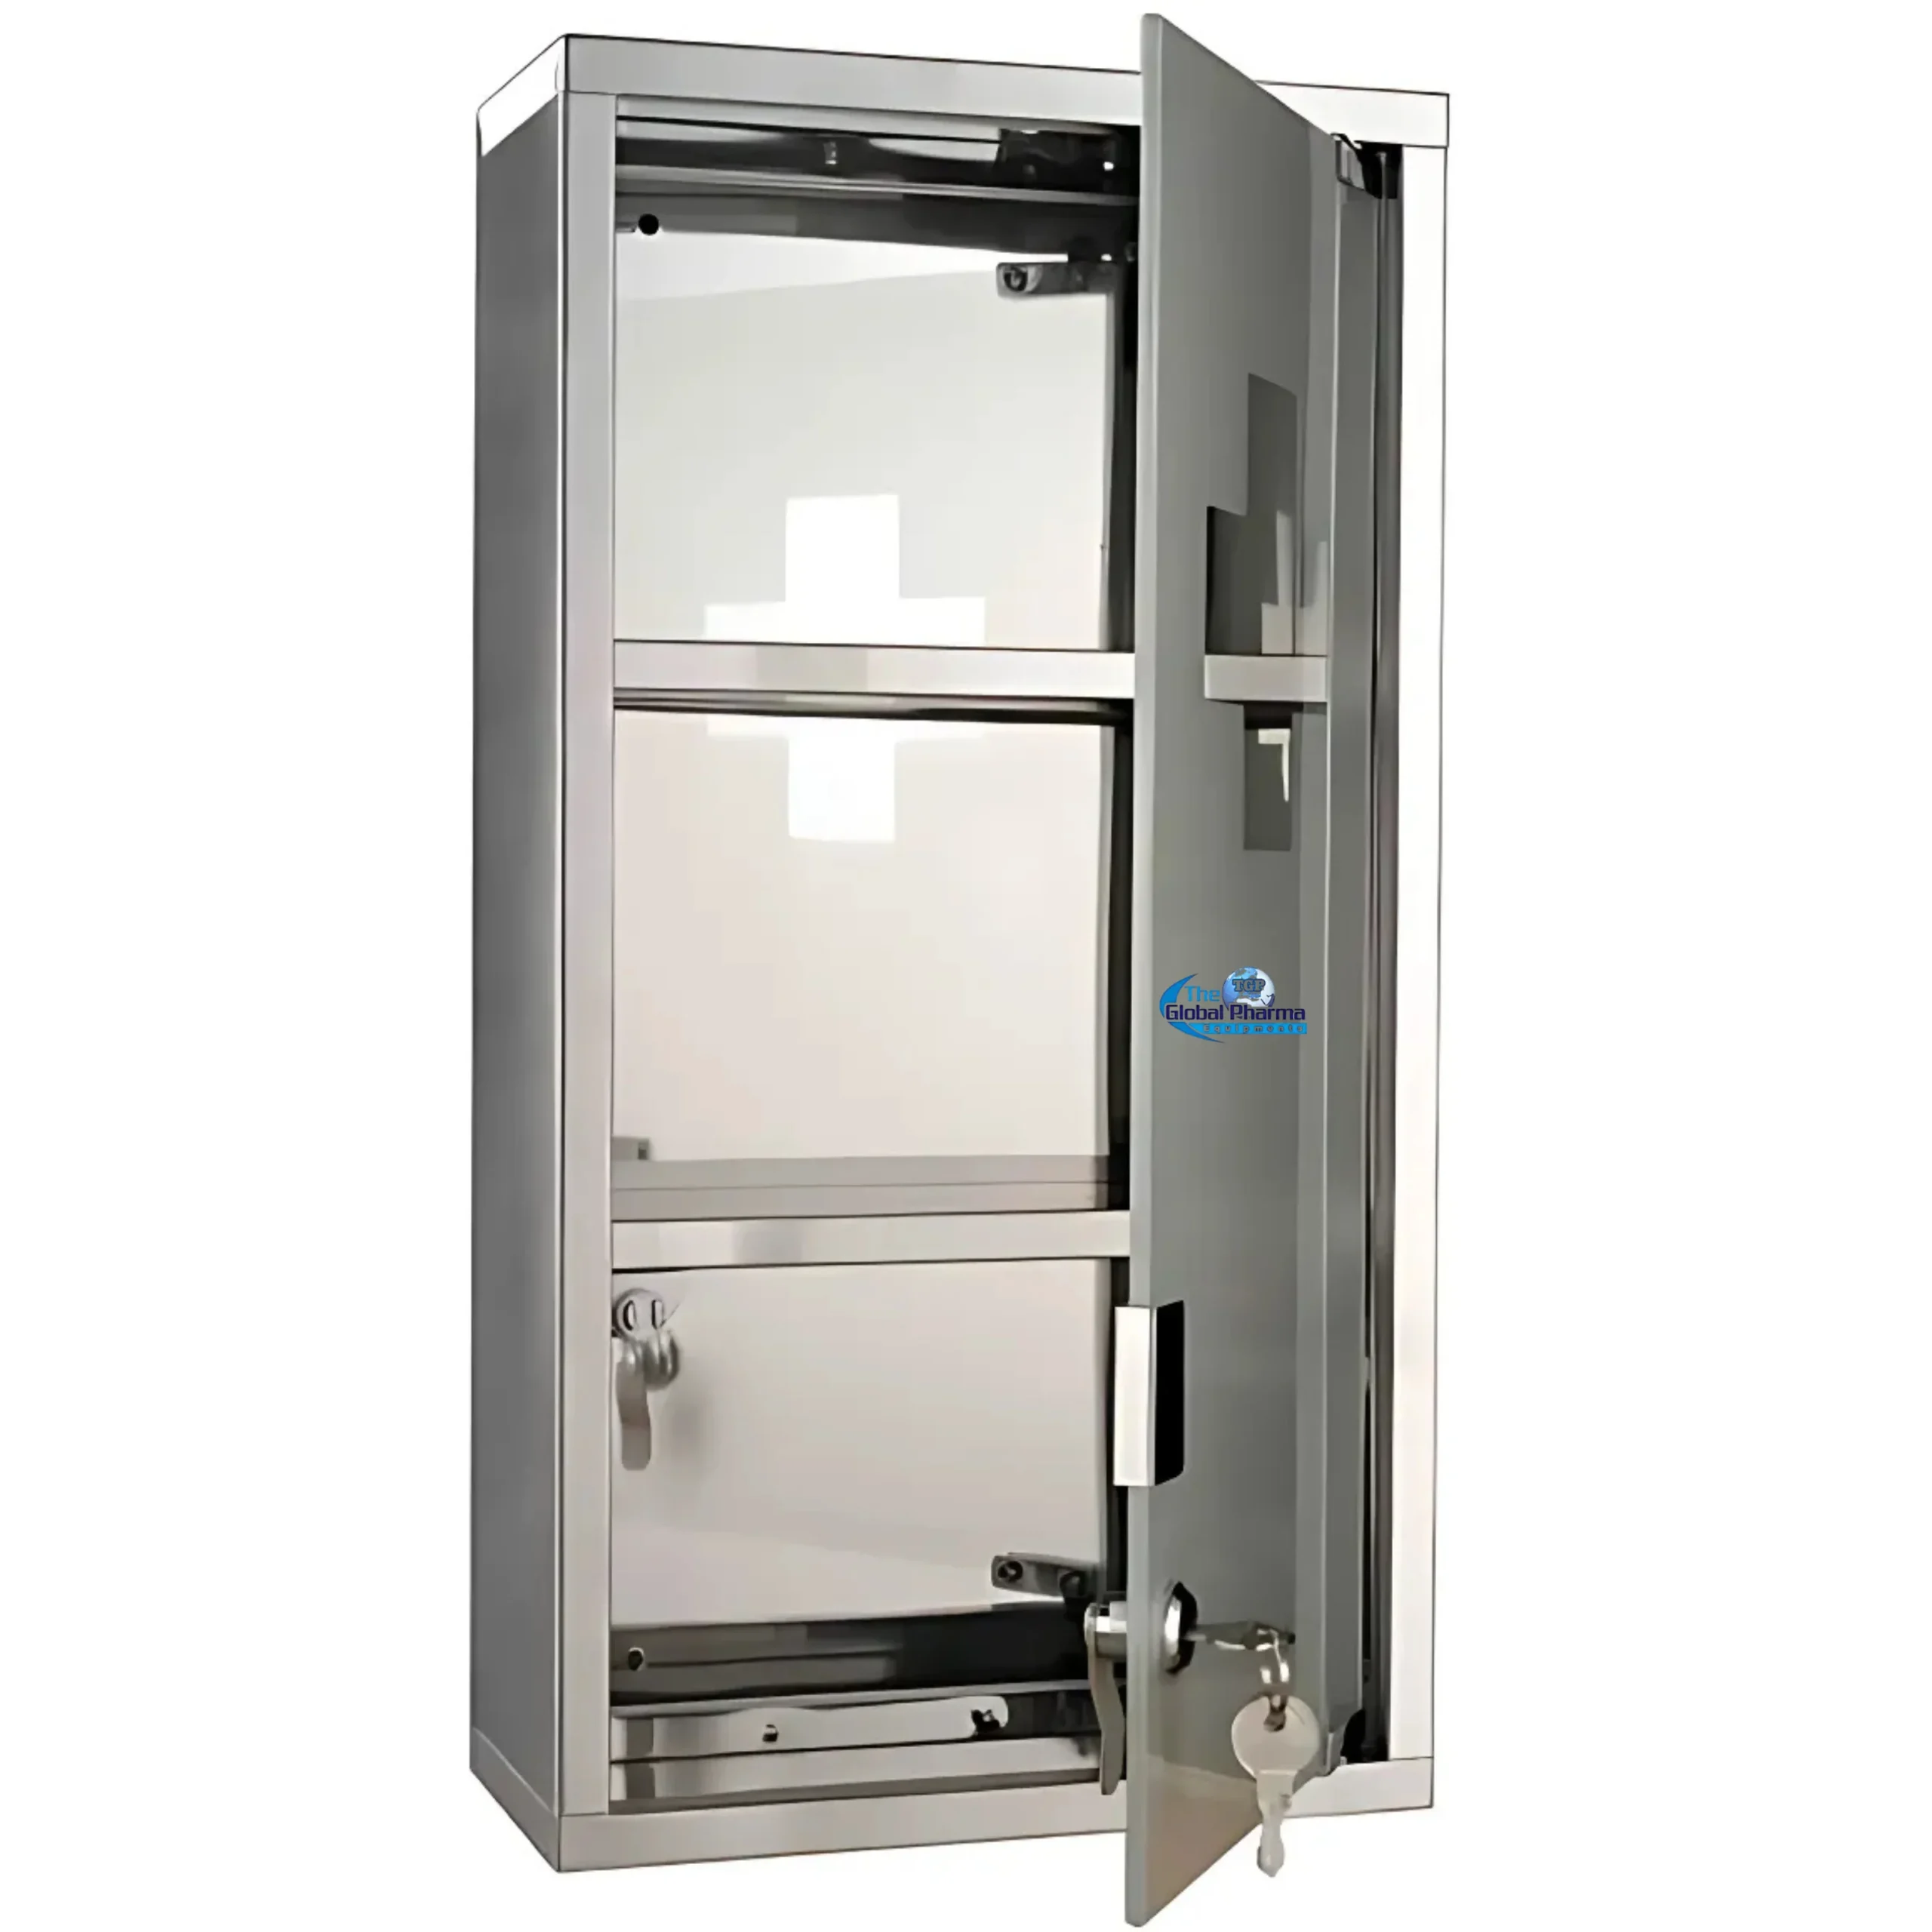
Quick access to medical supplies is essential during emergencies in hospitals, c...
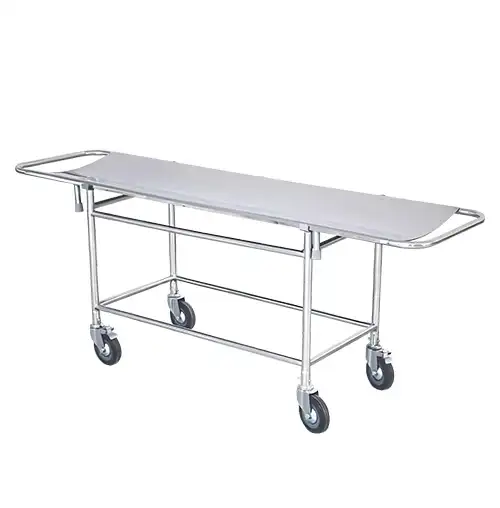
Safe and efficient patient transportation is essential in hospitals and healthca...
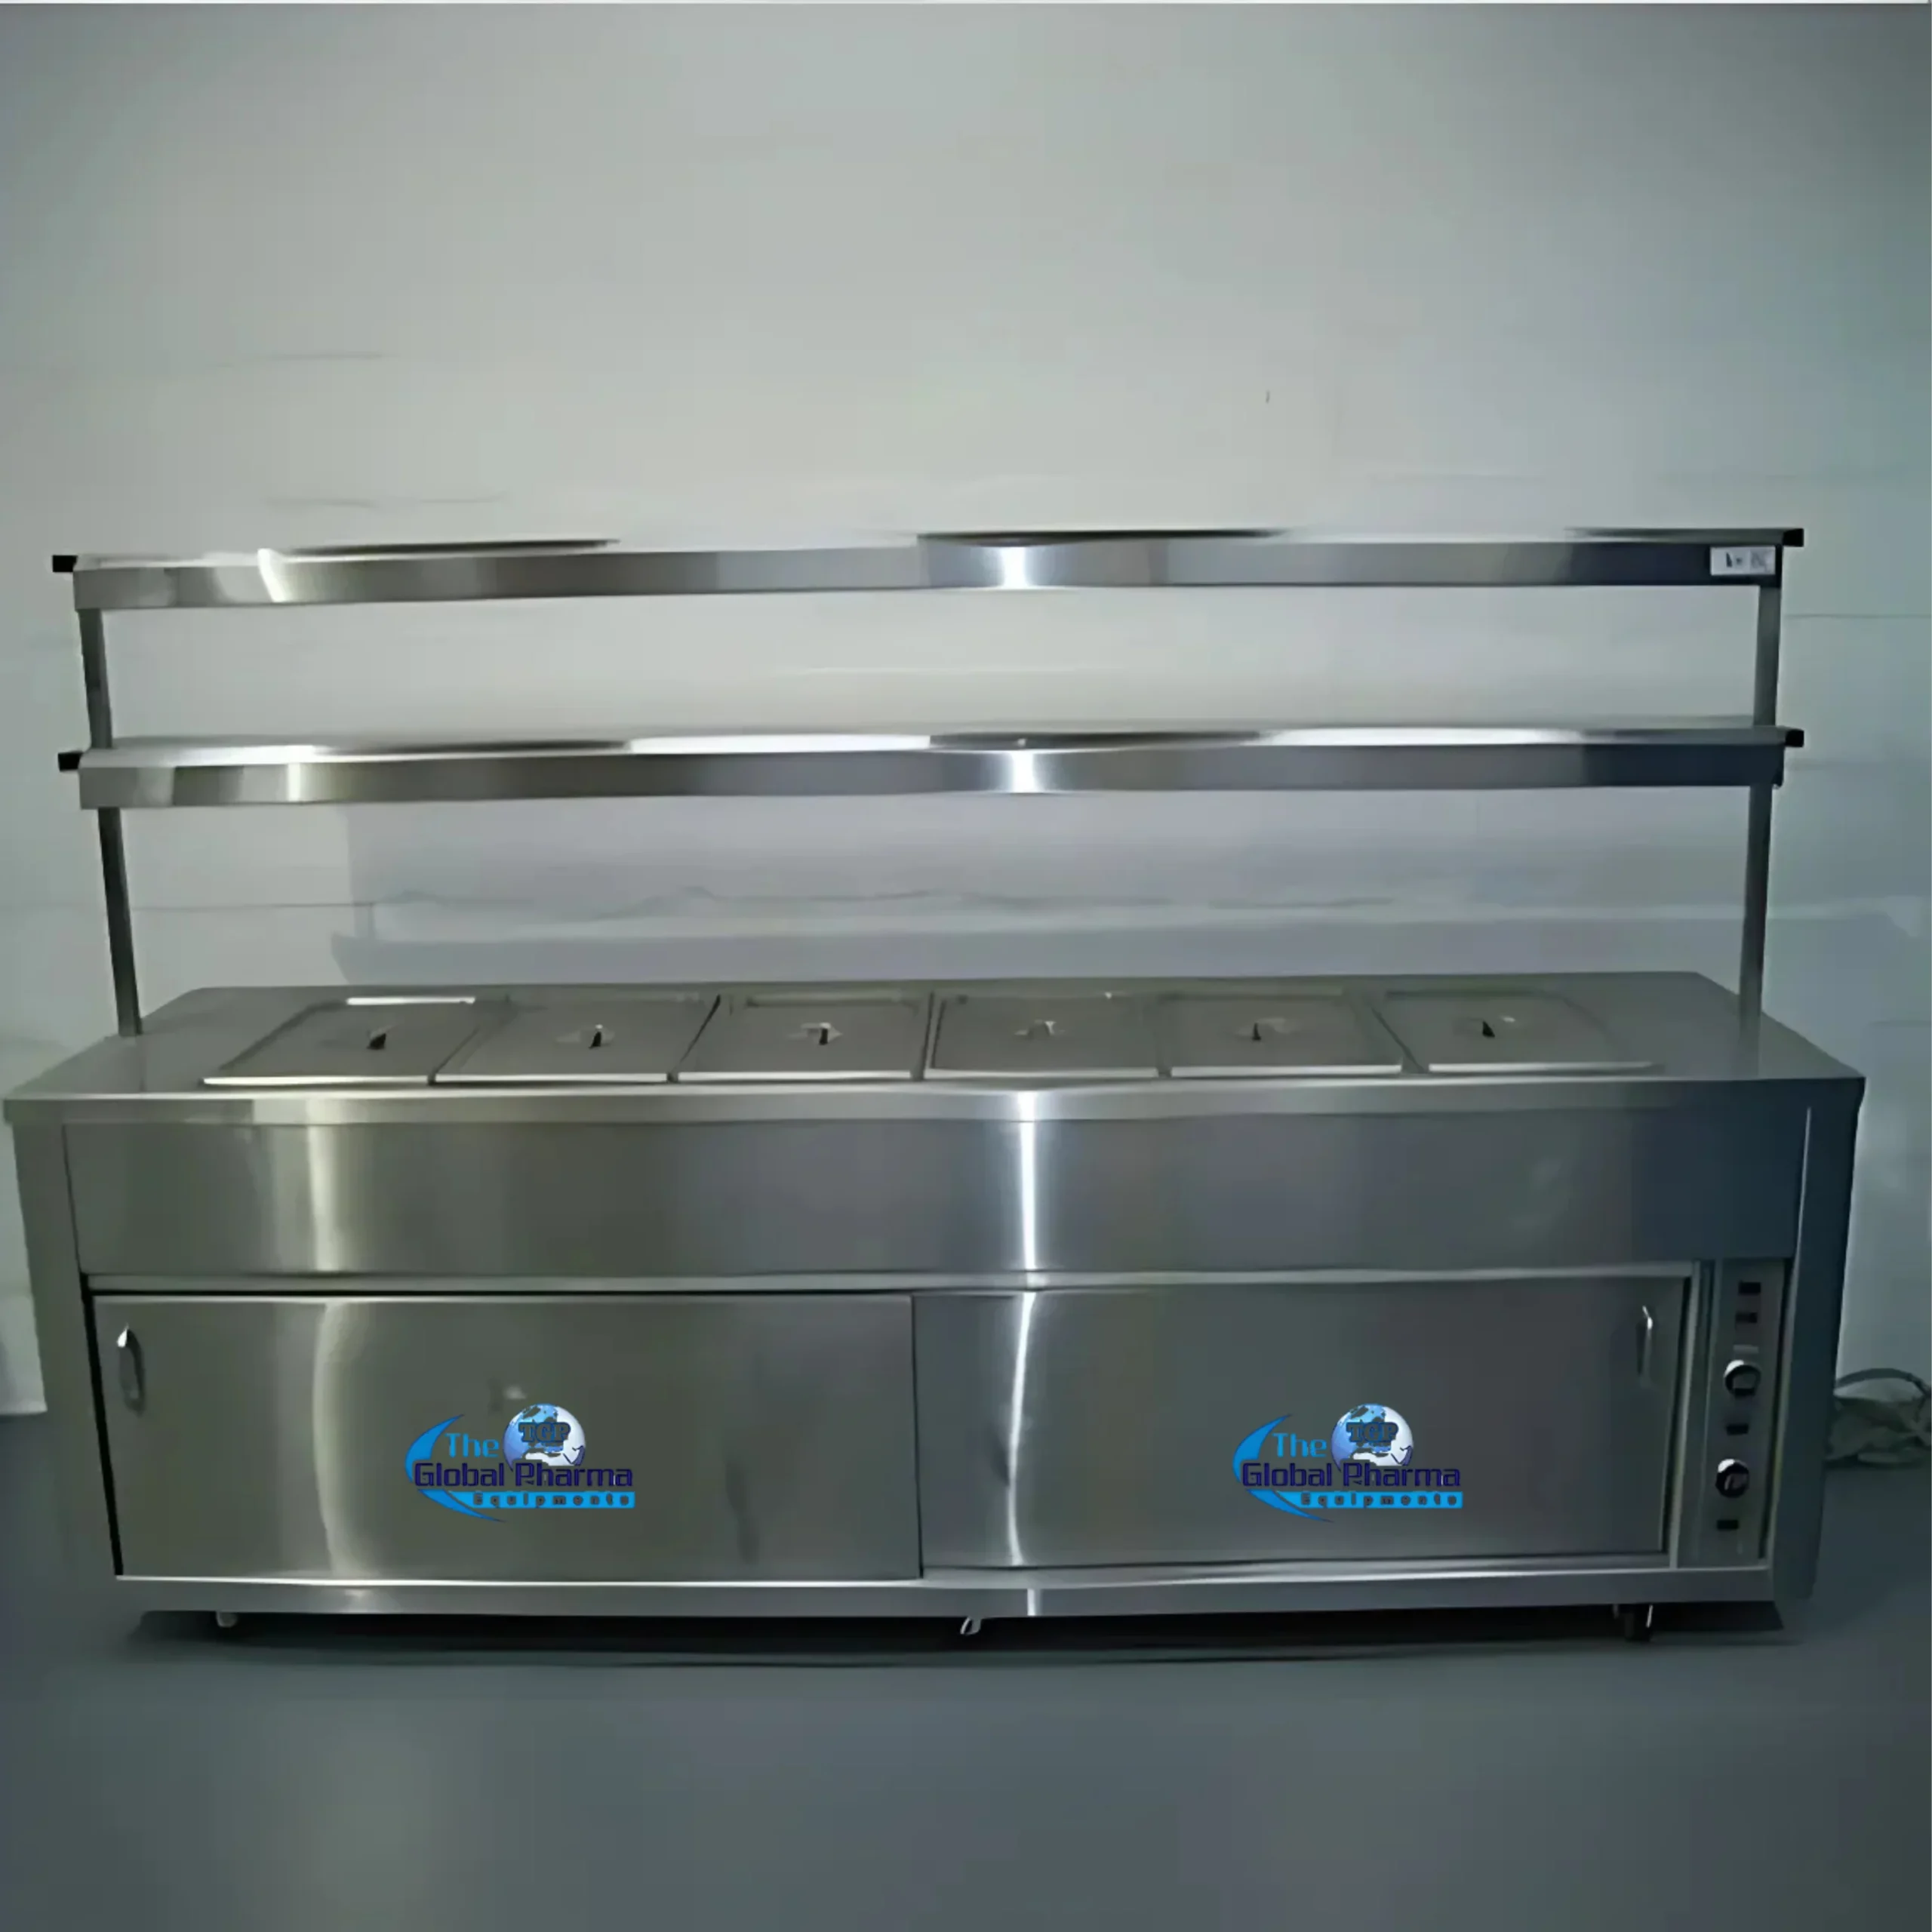
Modern food preparation facilities require reliable equipment that enhances prod...
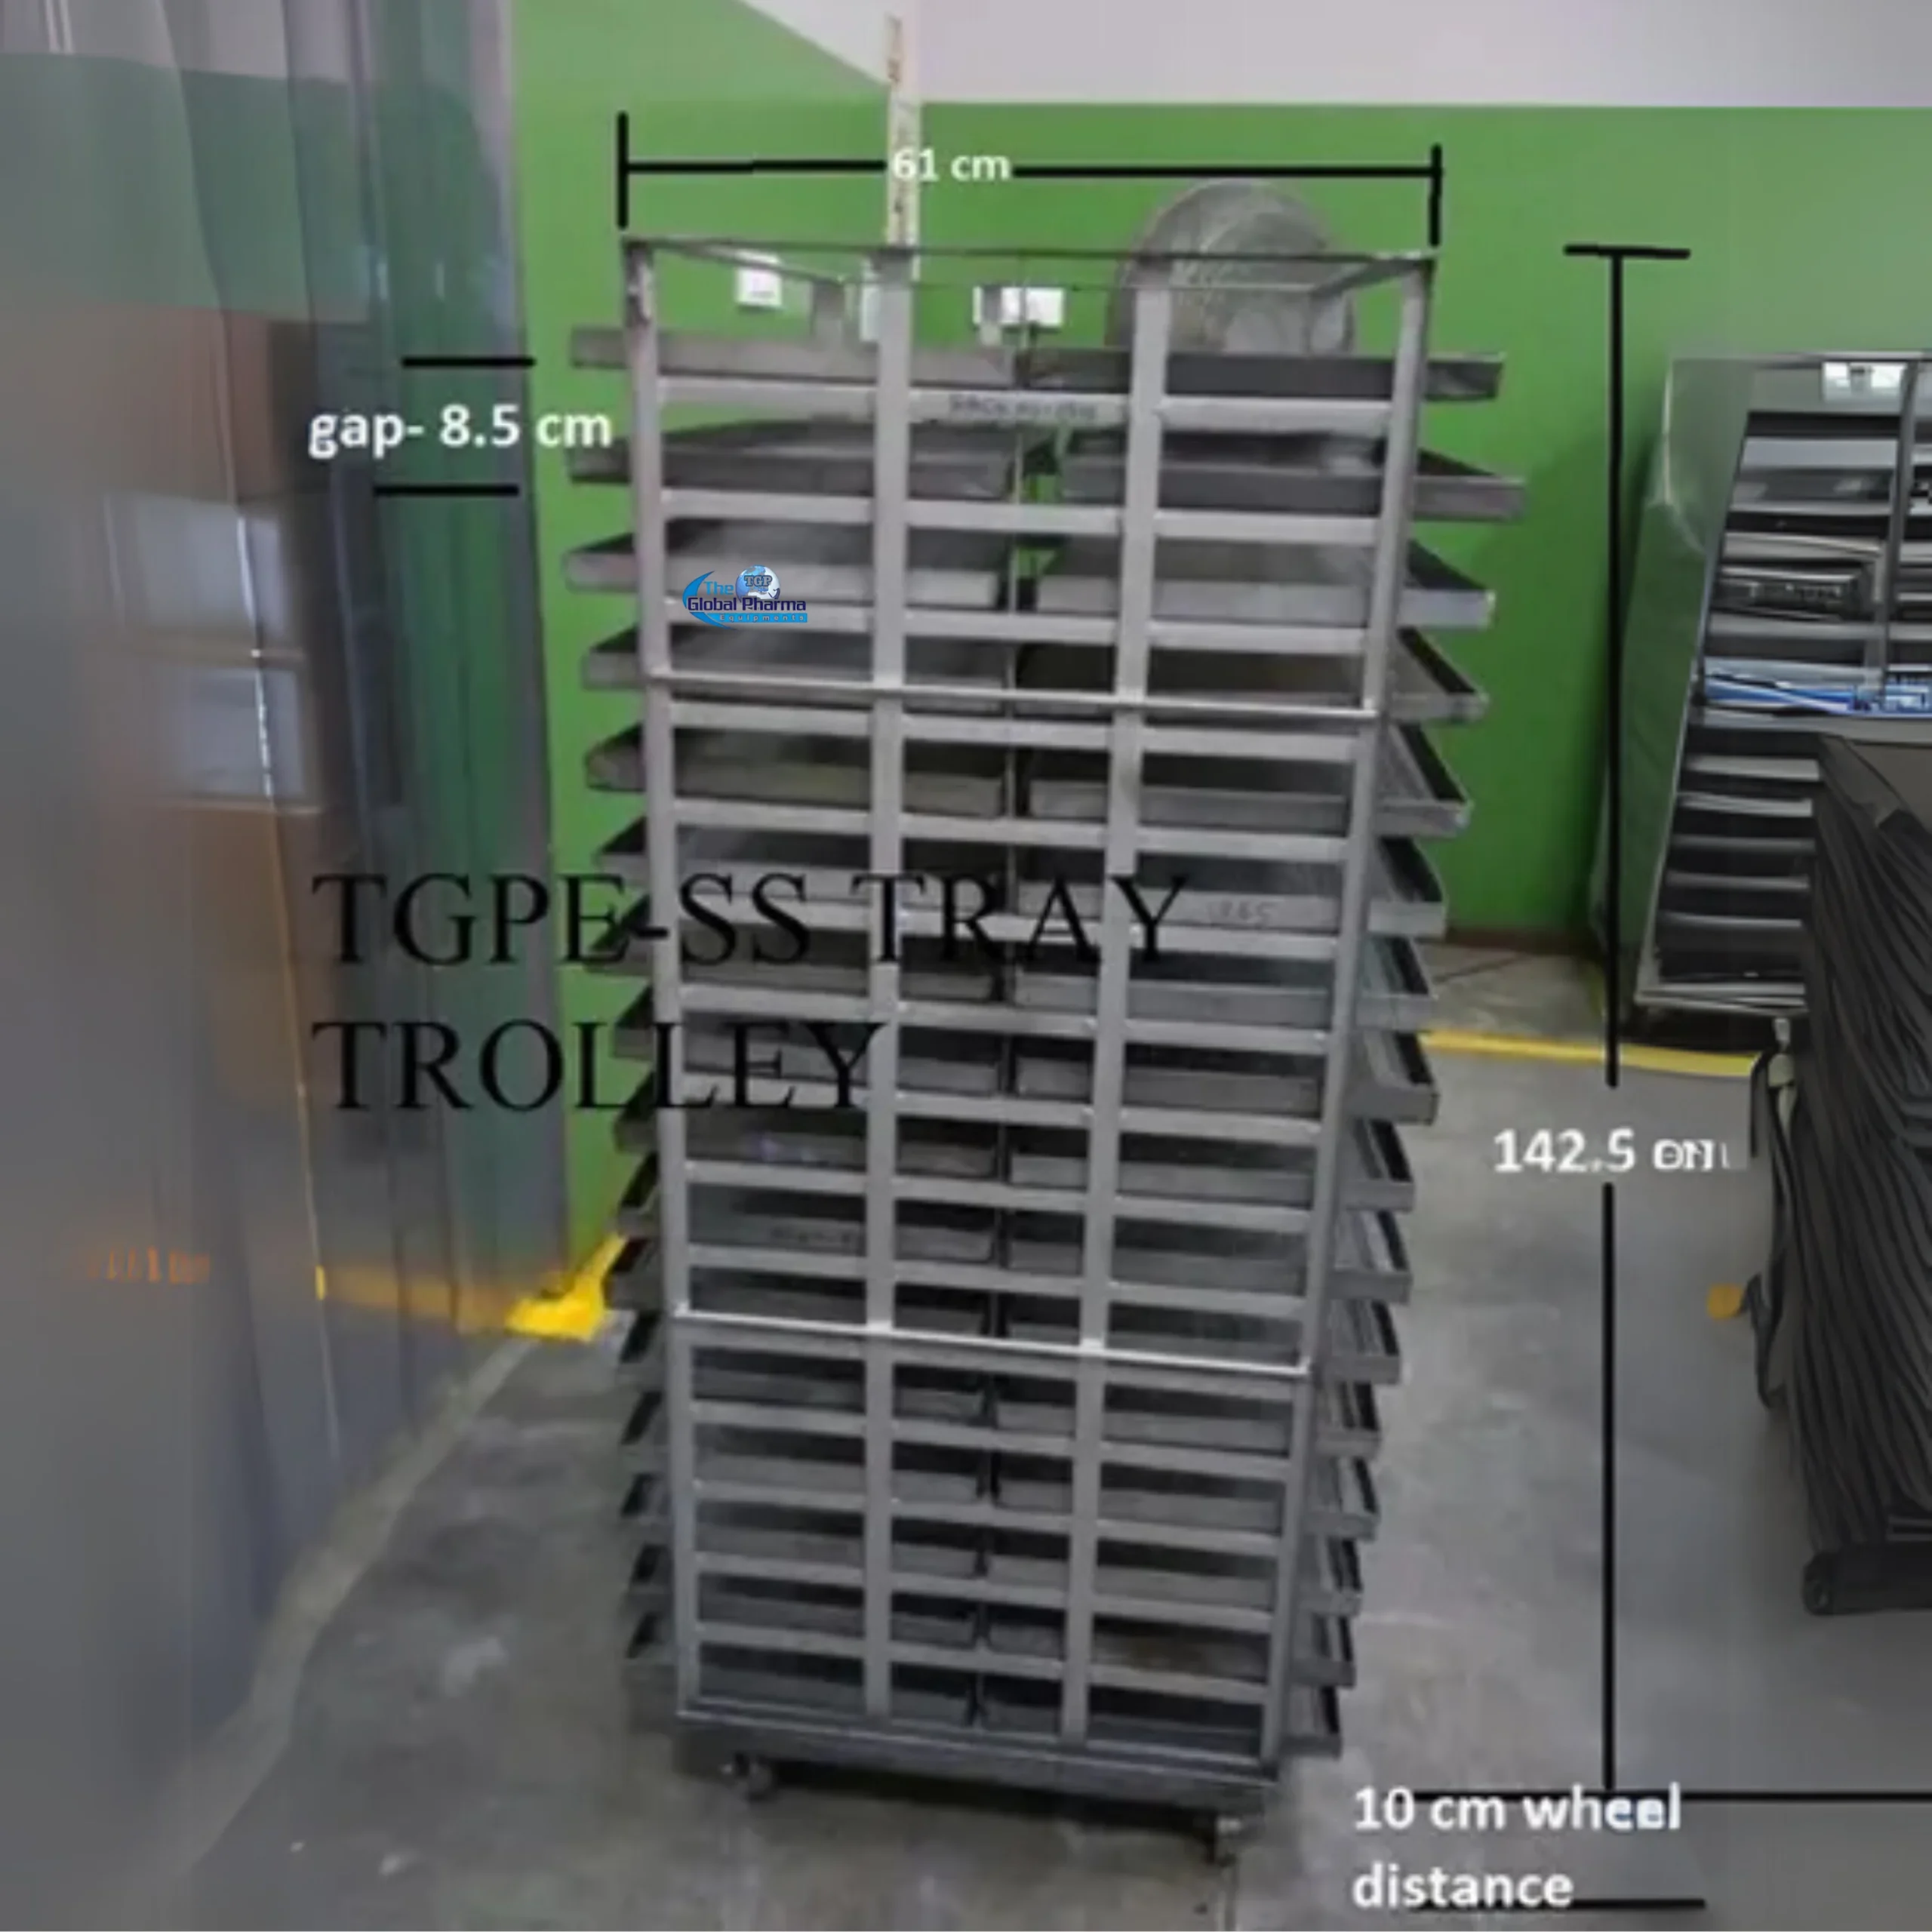
Efficient transportation of trays, food items, medical supplies, and equipment i...
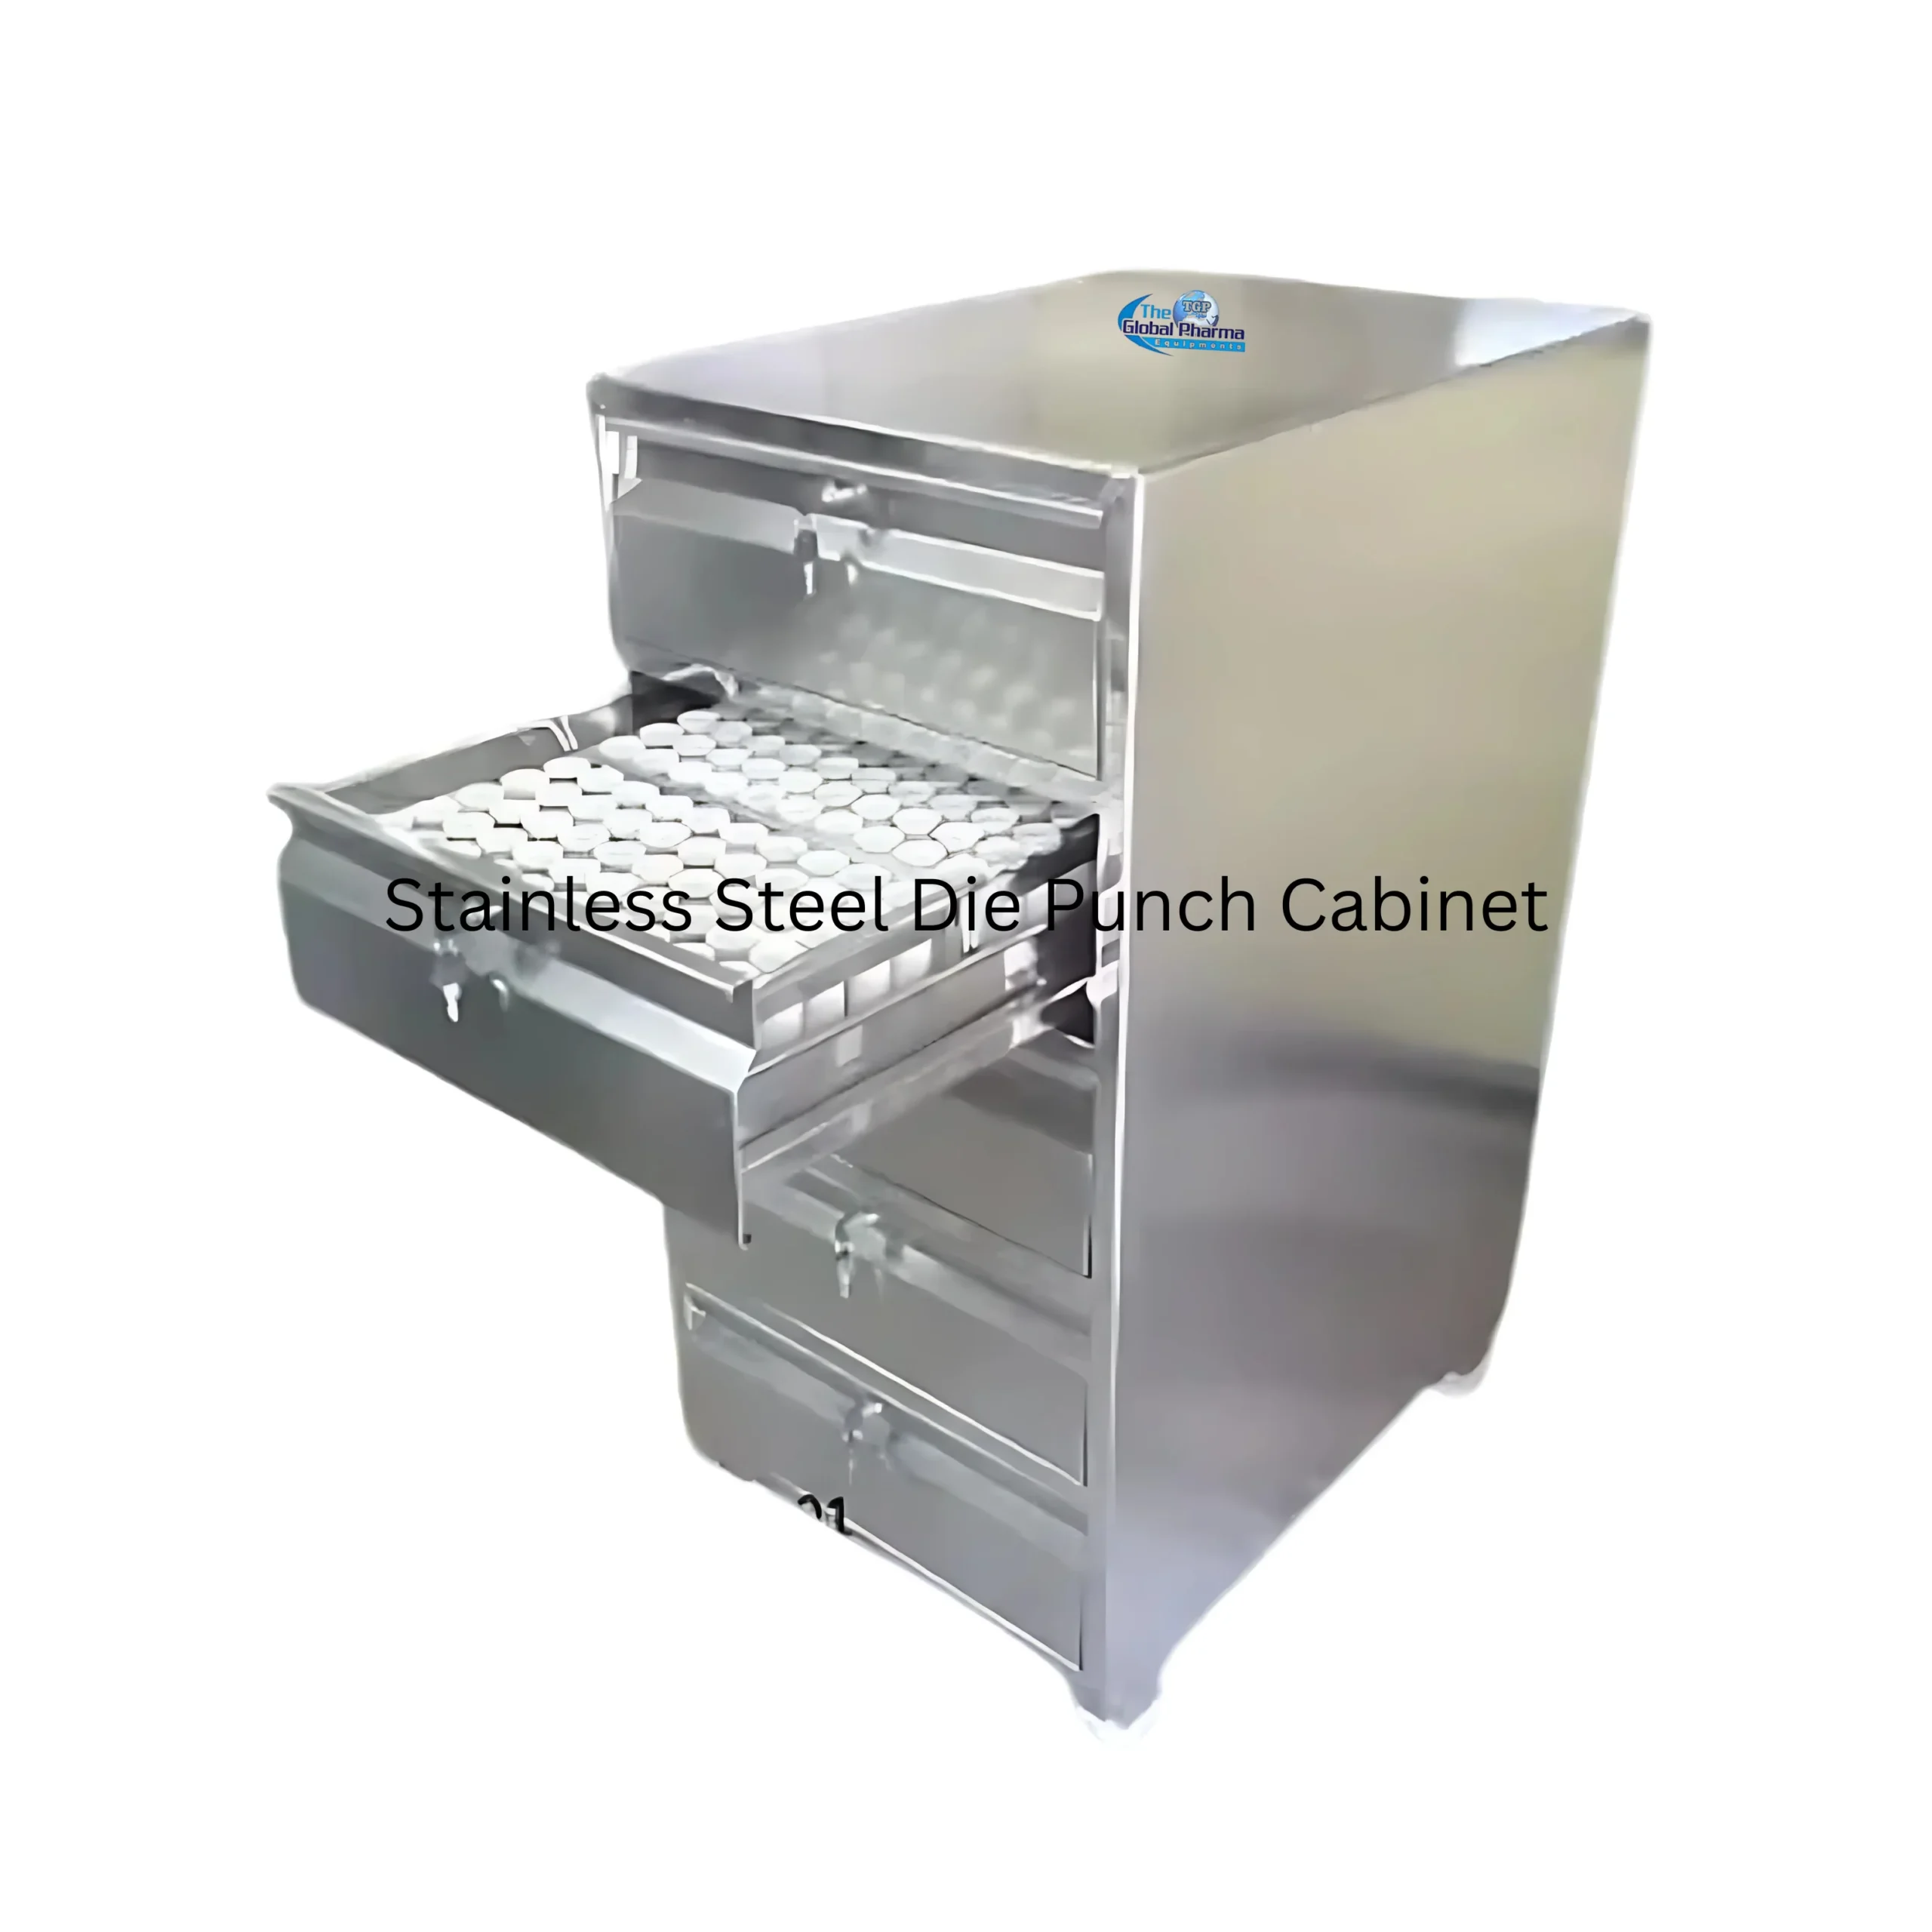
Efficient storage and systematic organization of dies, punches, tooling componen...
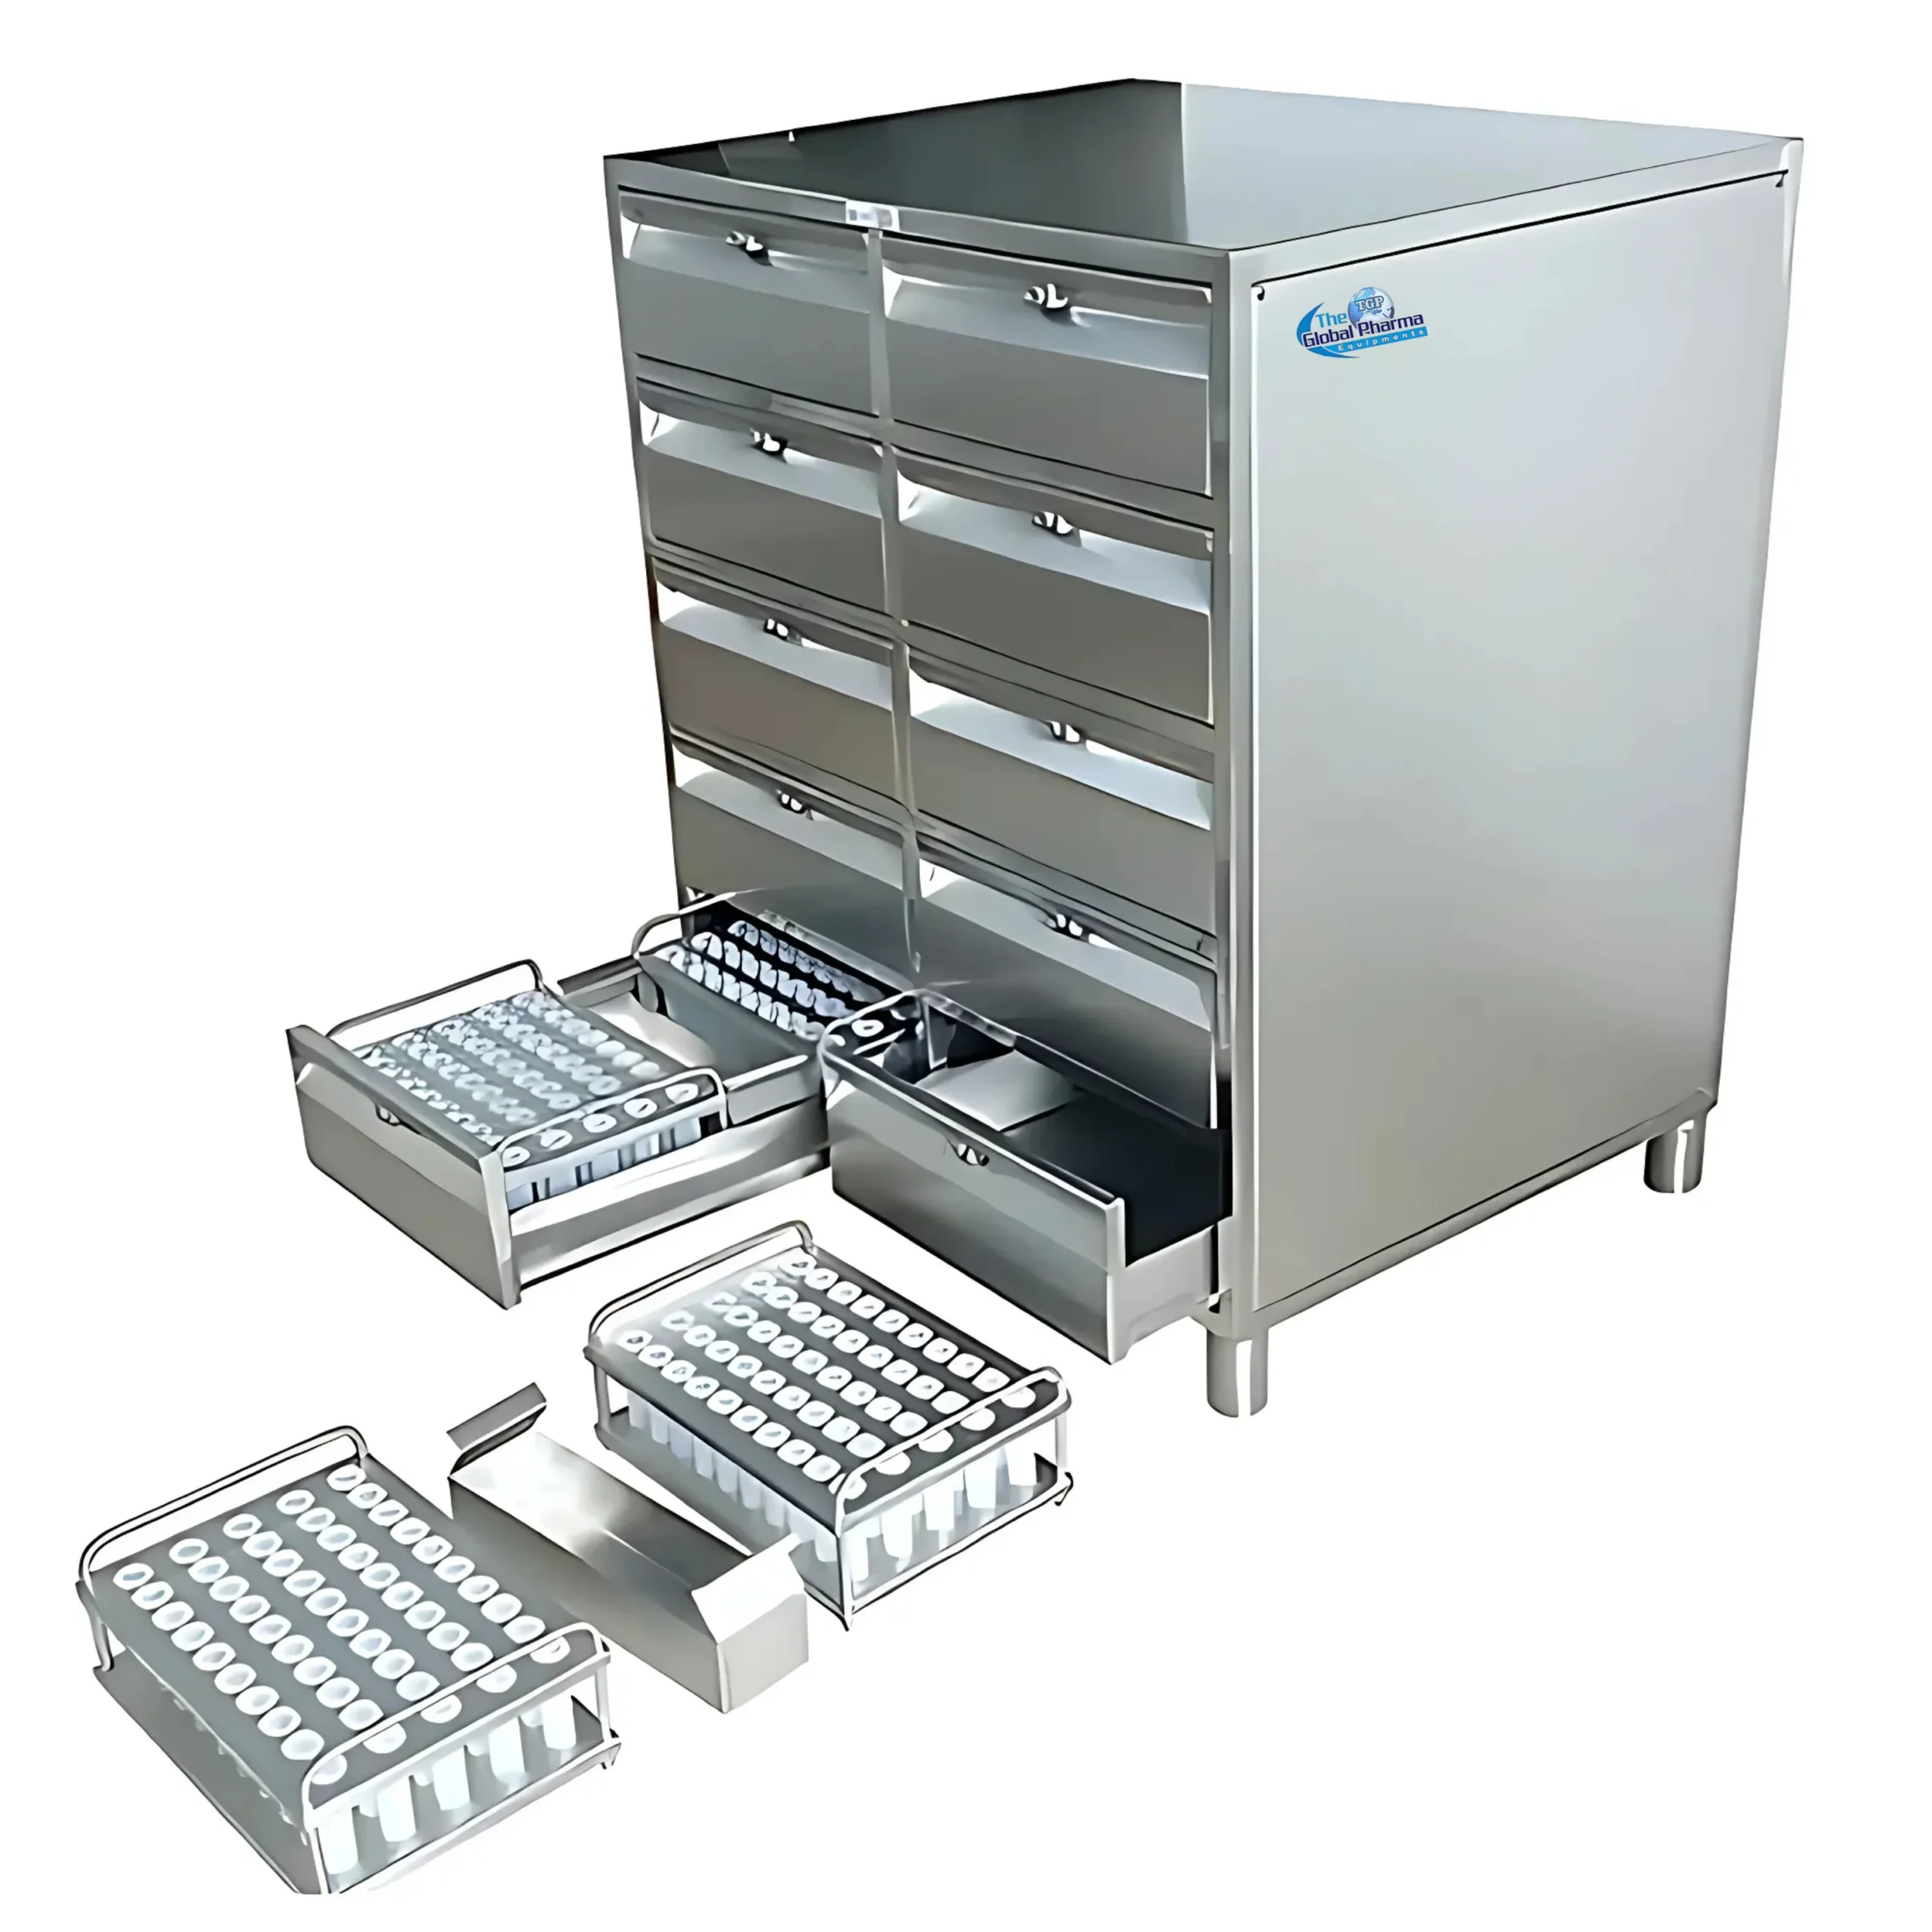
Efficient storage and systematic organization of punches, dies, and precision to...
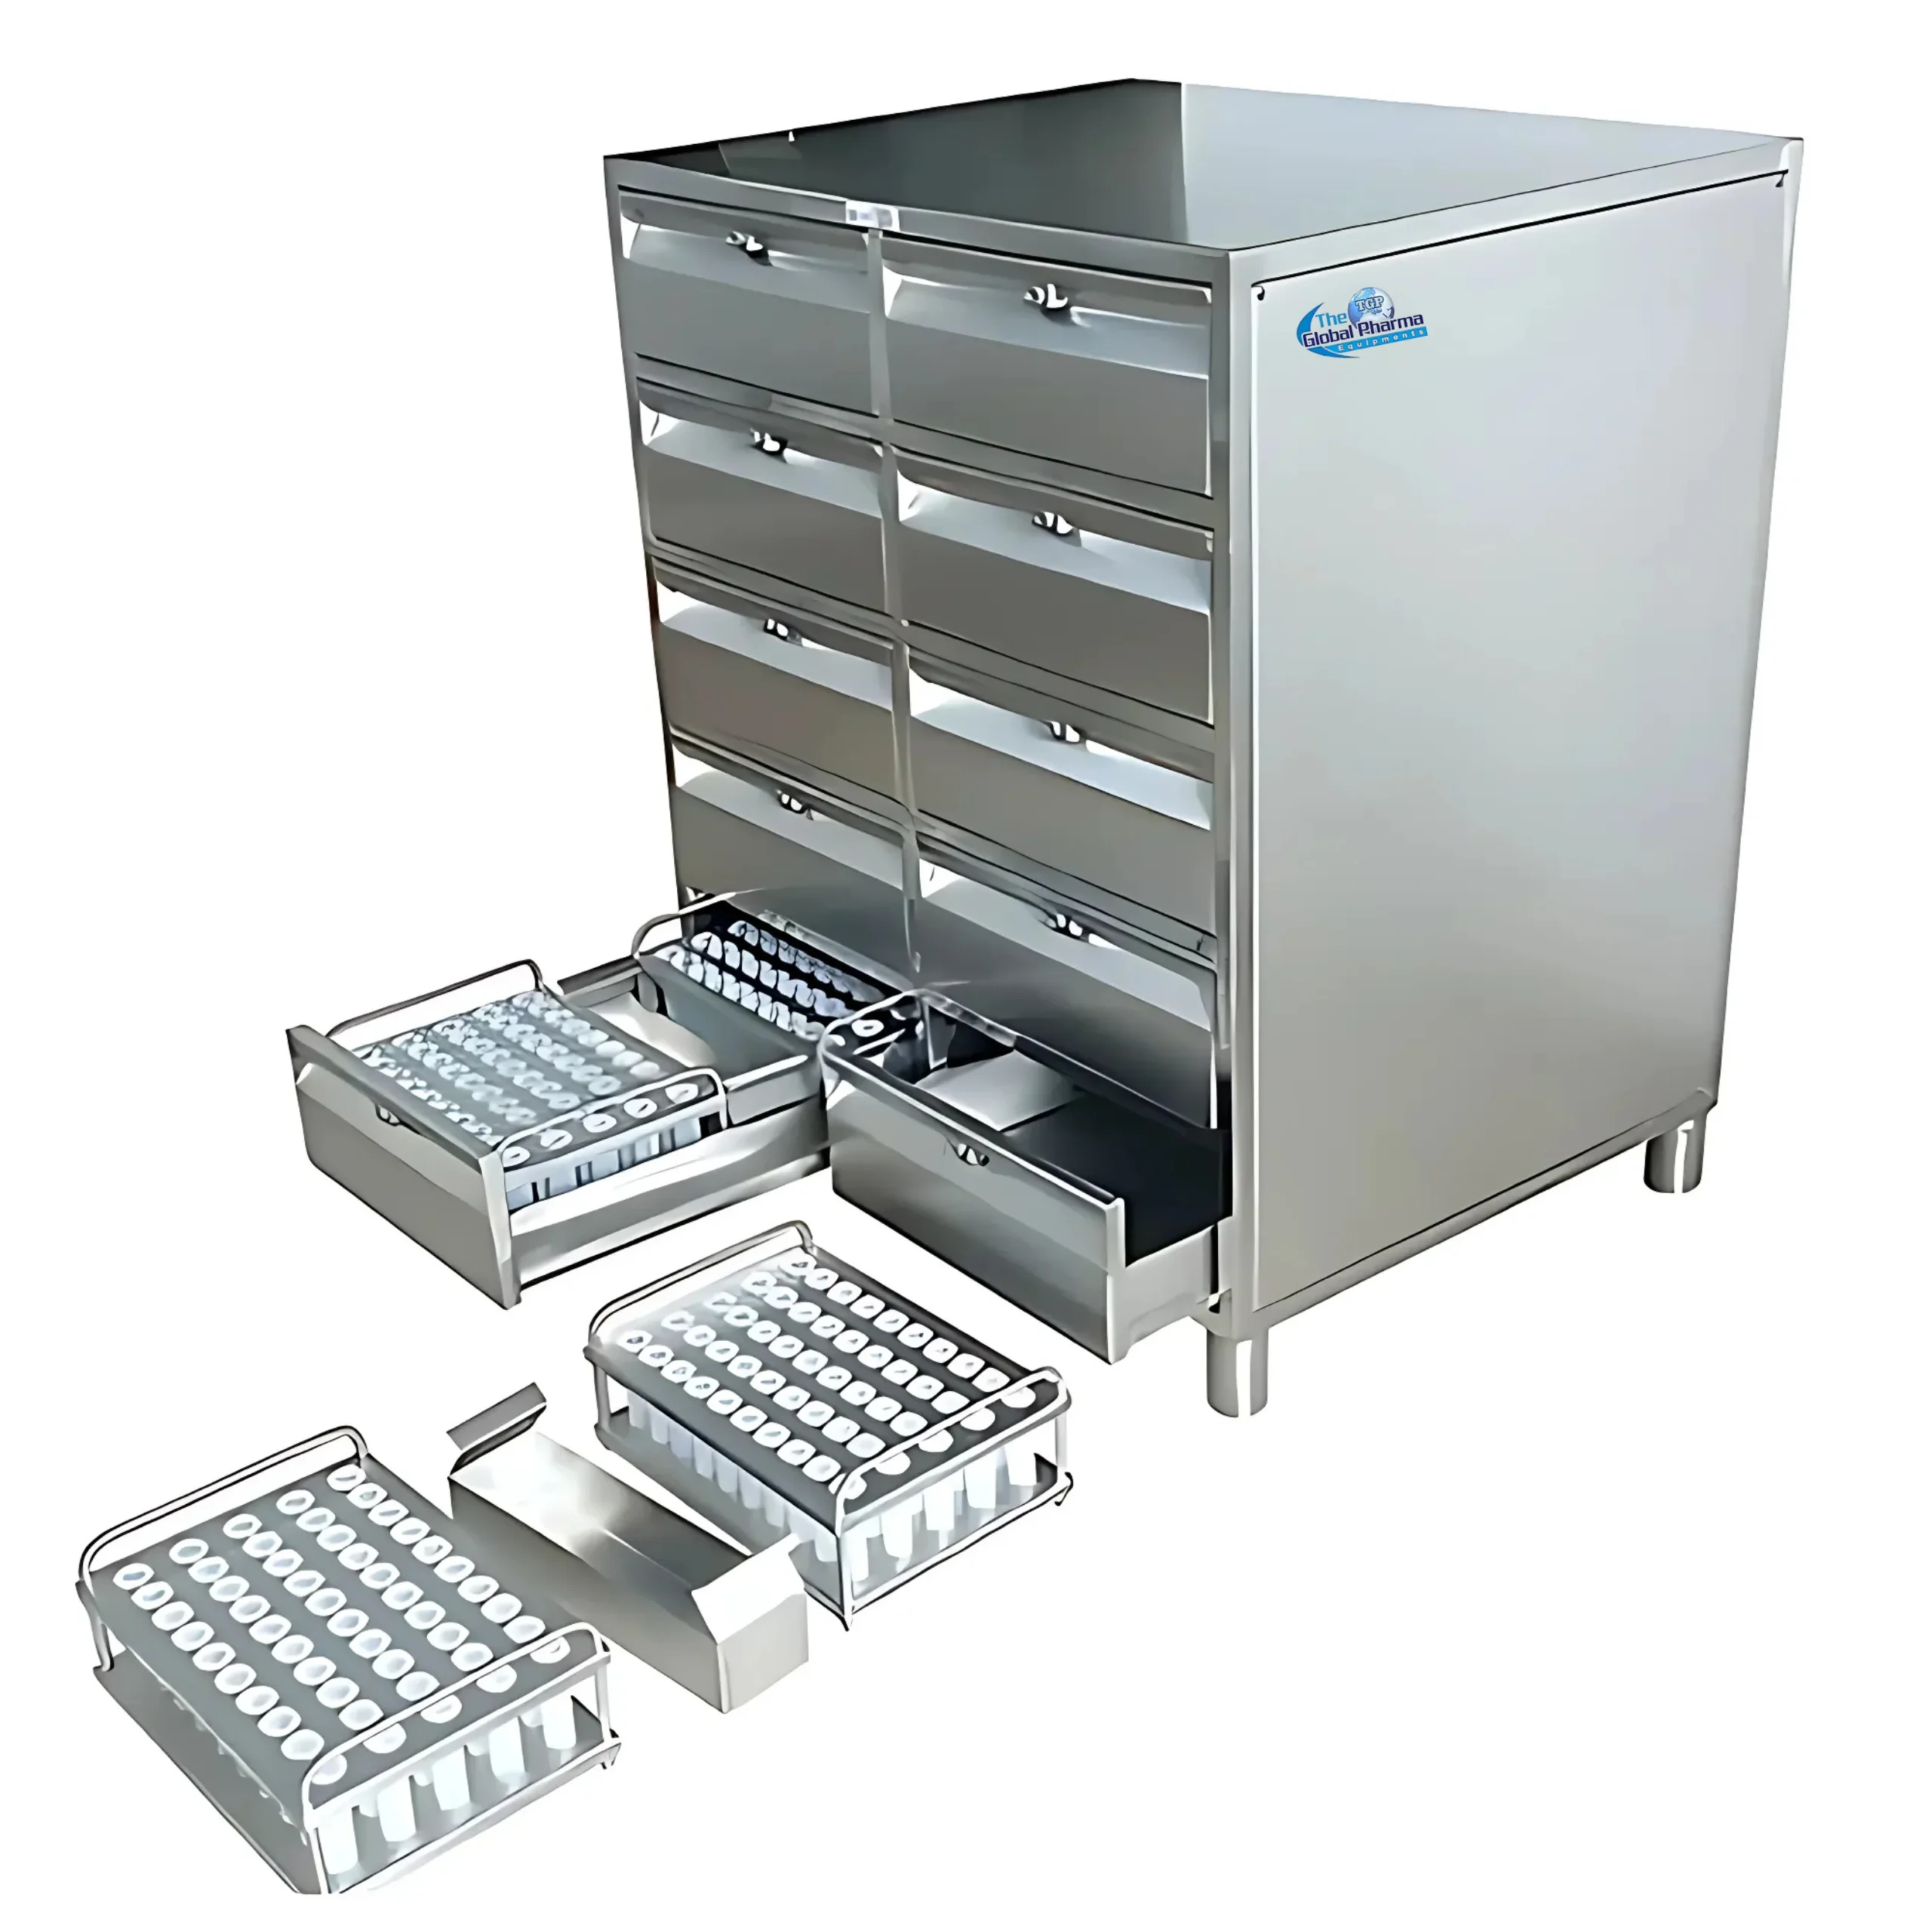
Safe transportation and organized handling of dies, punches, and precision tooli...
Reliable and hygienic drinking and utility vessels are essential across hospital...
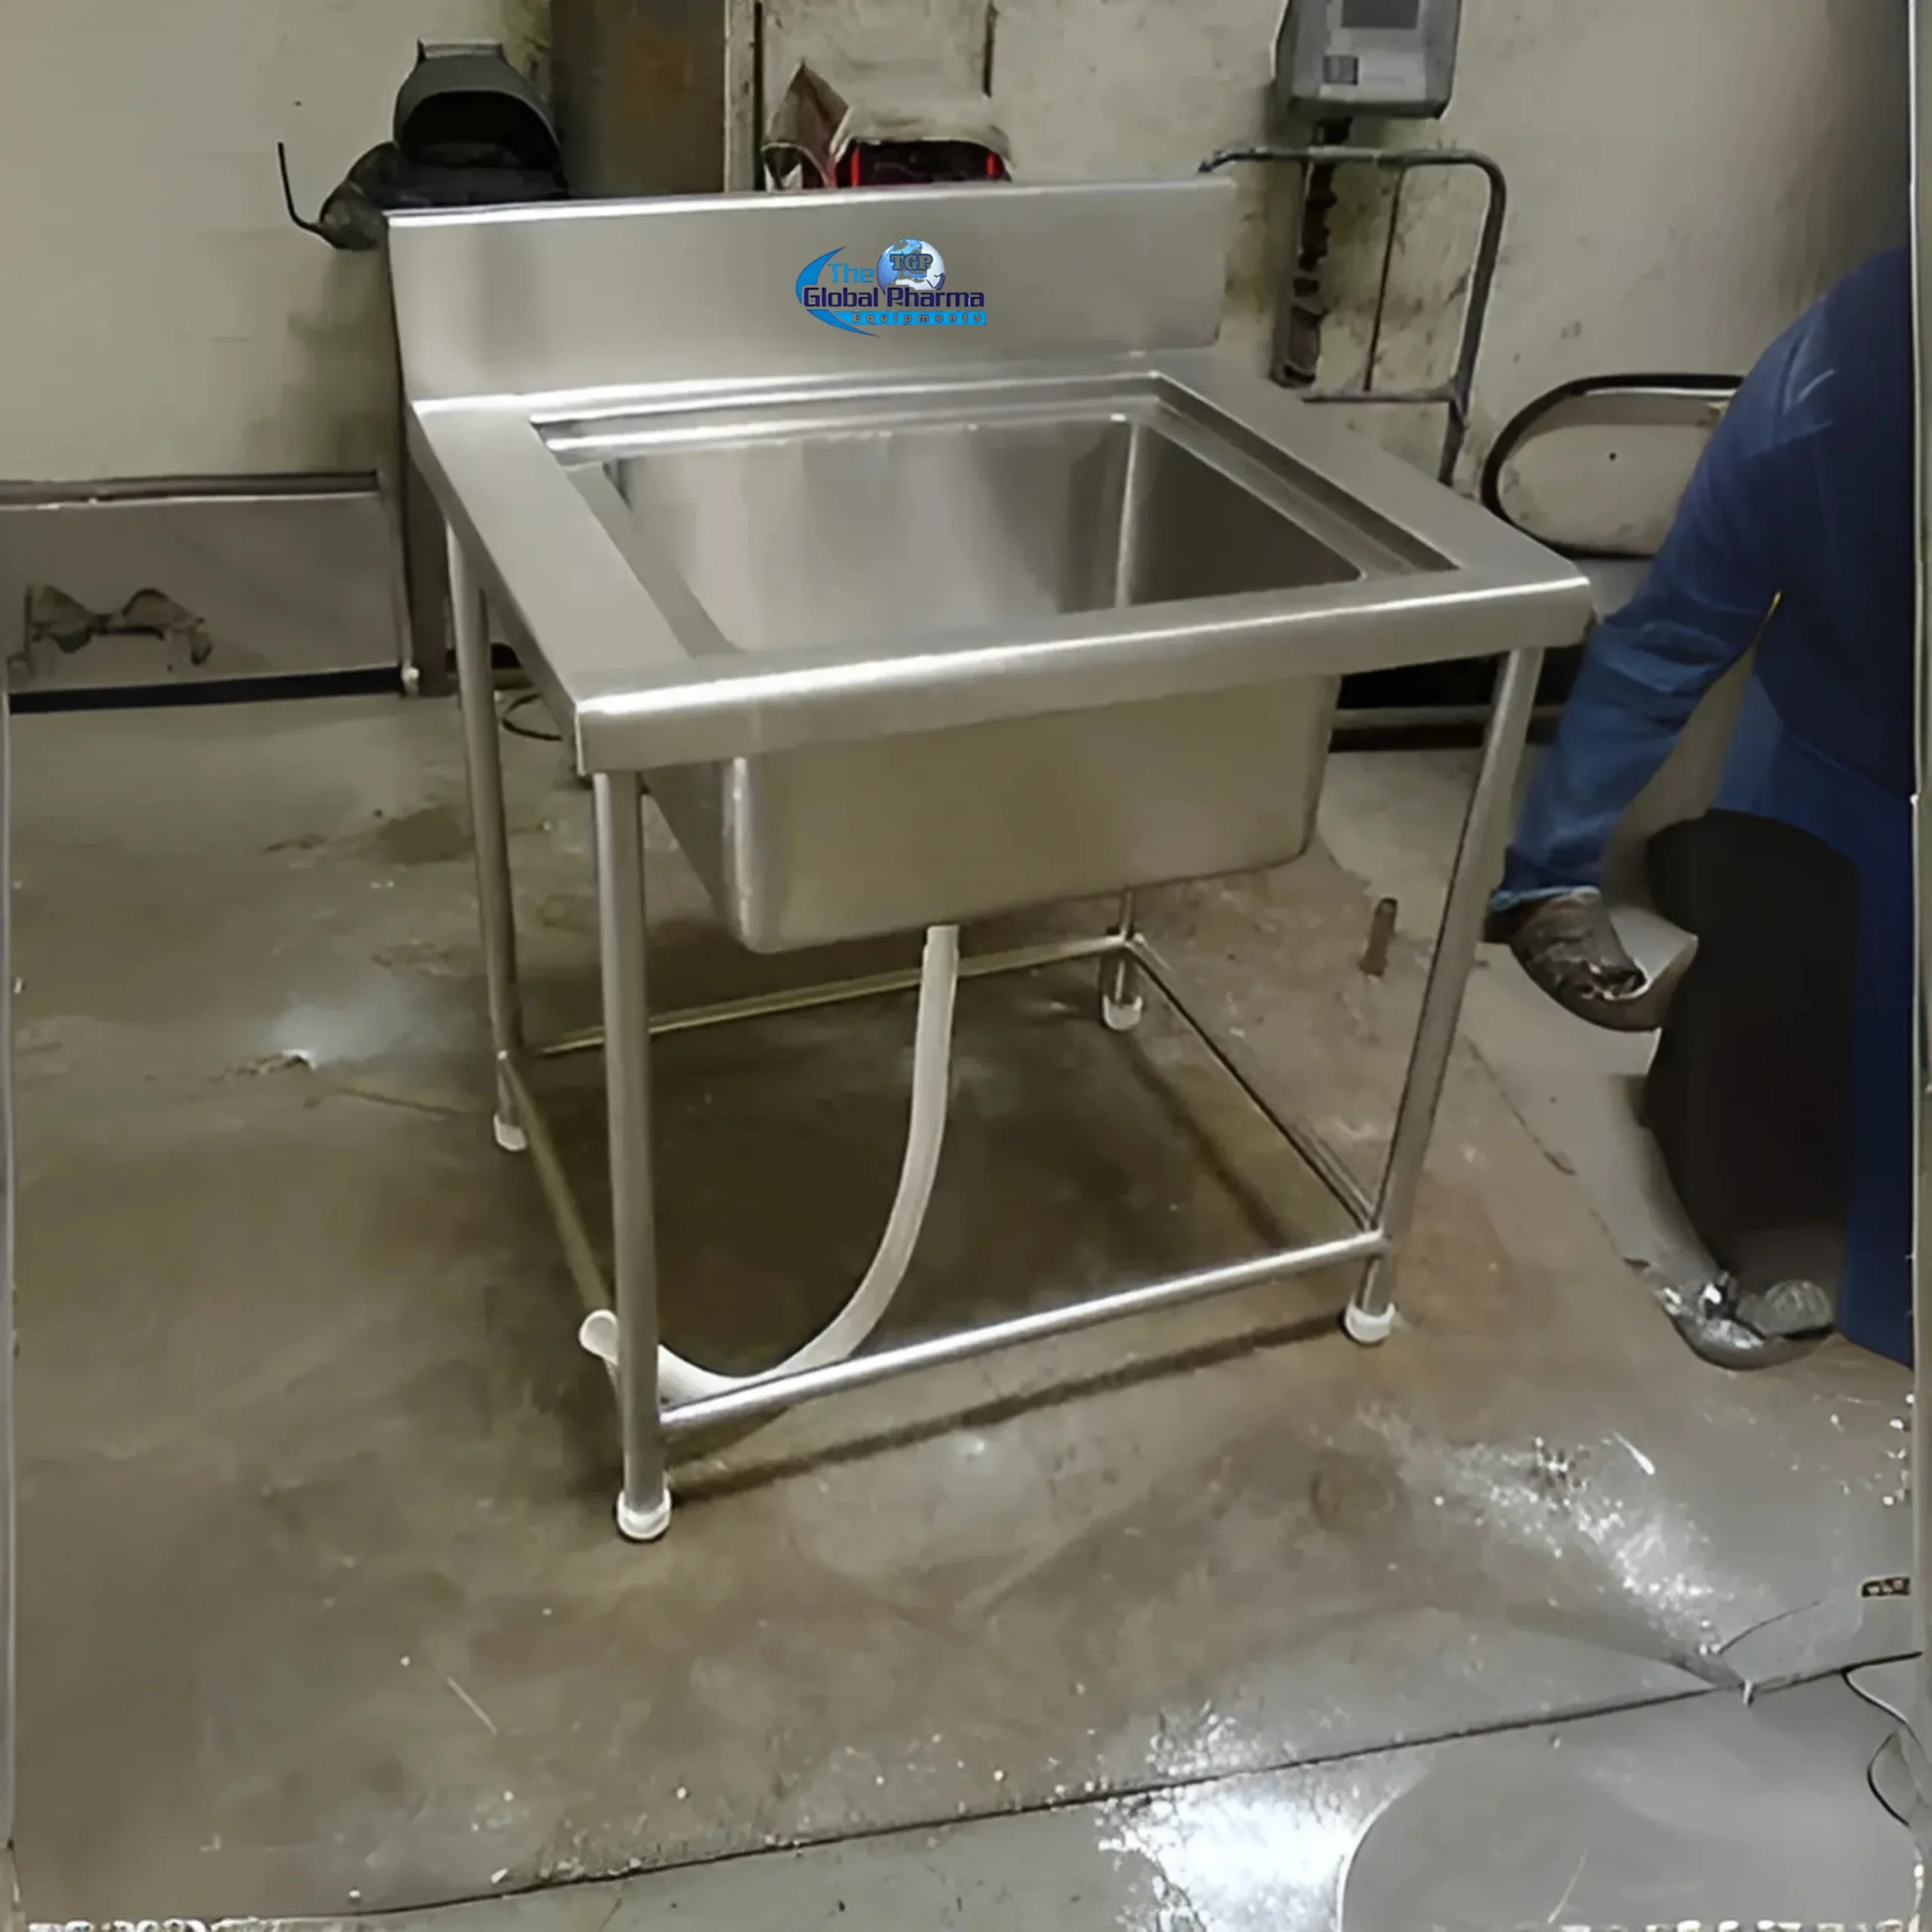
Hygienic washing facilities are essential in commercial kitchens, pharmaceutical...
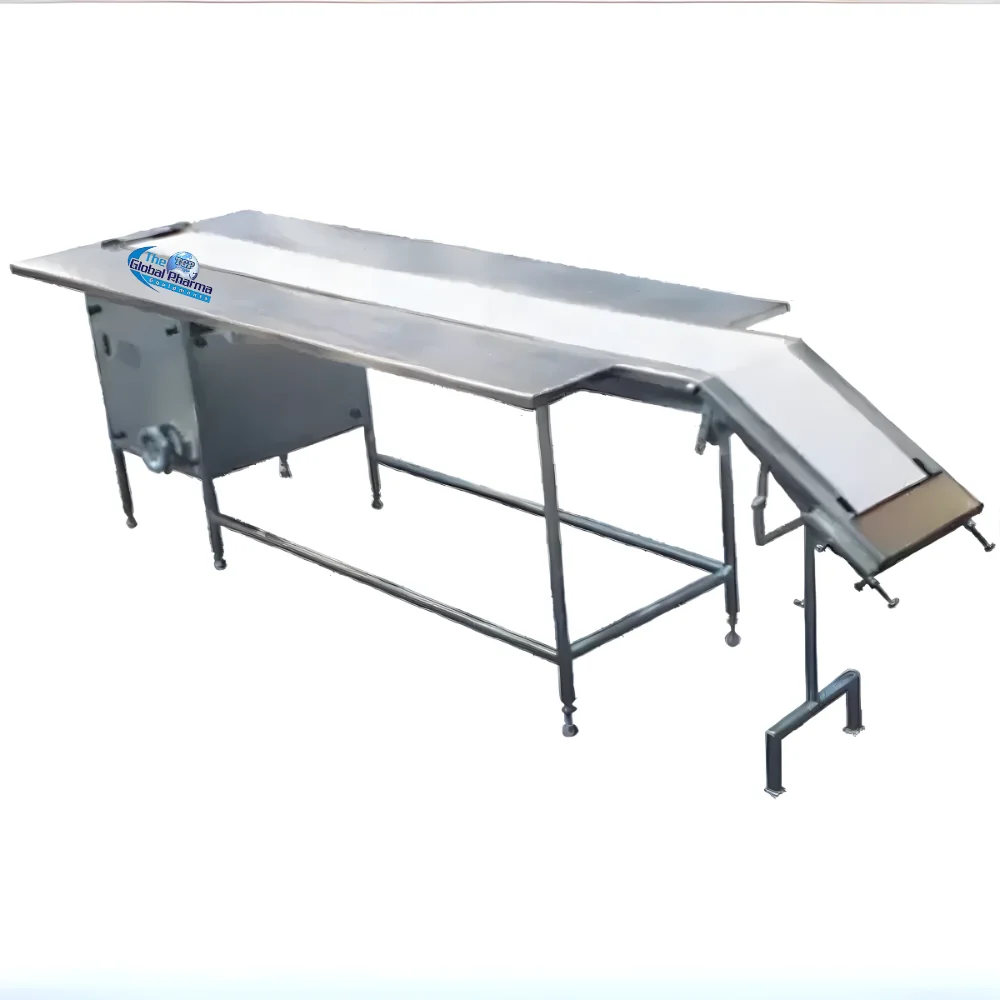
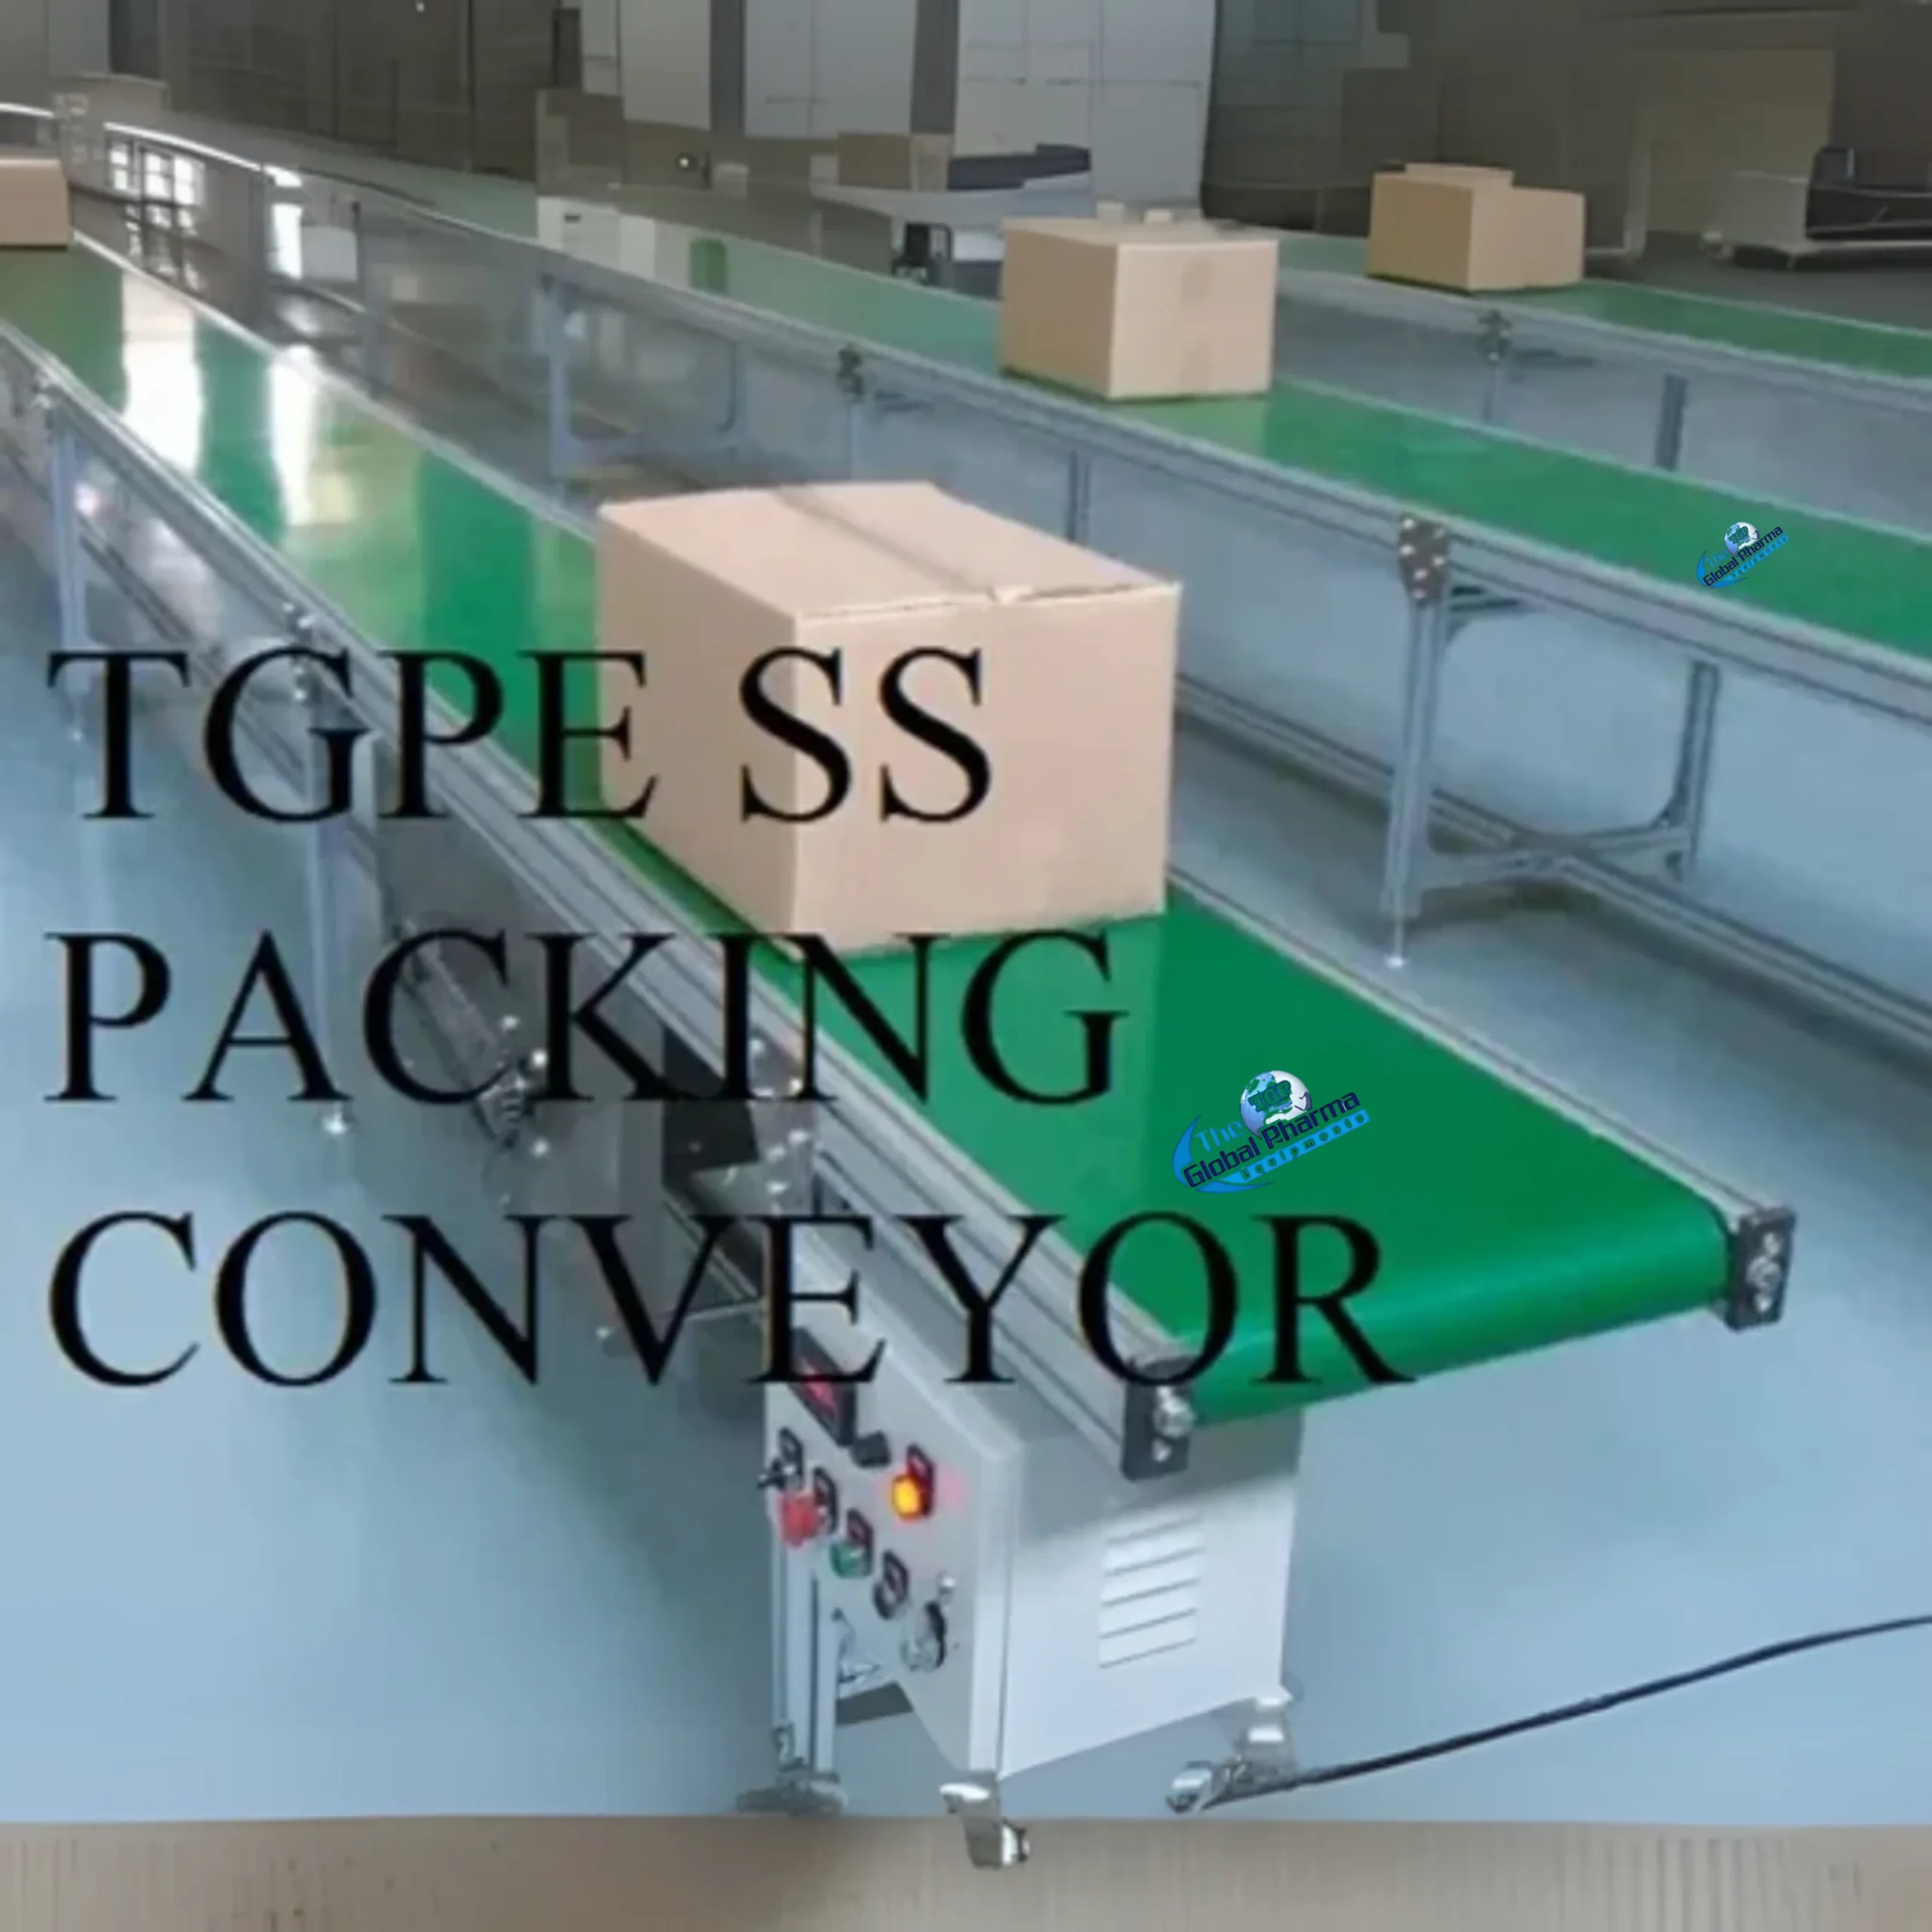
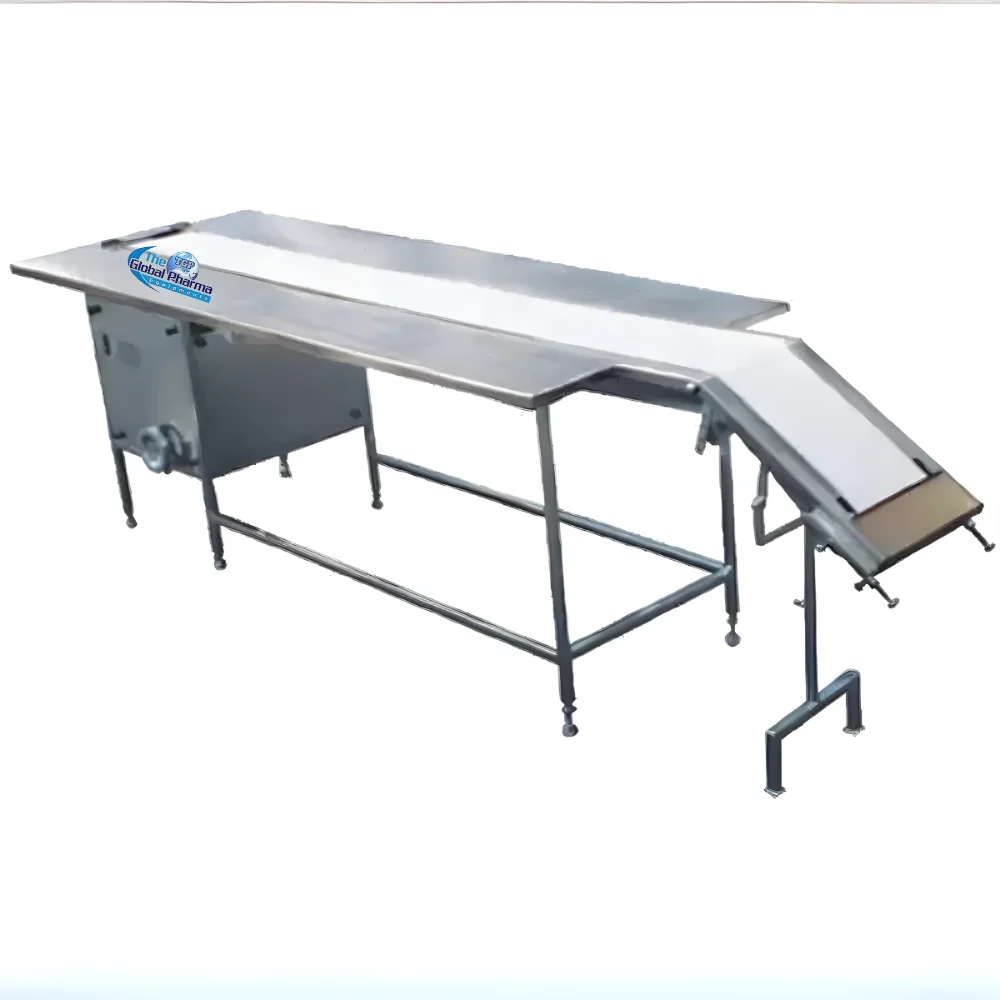
Efficient and hygienic material transportation is essential for pharmaceutical, ...
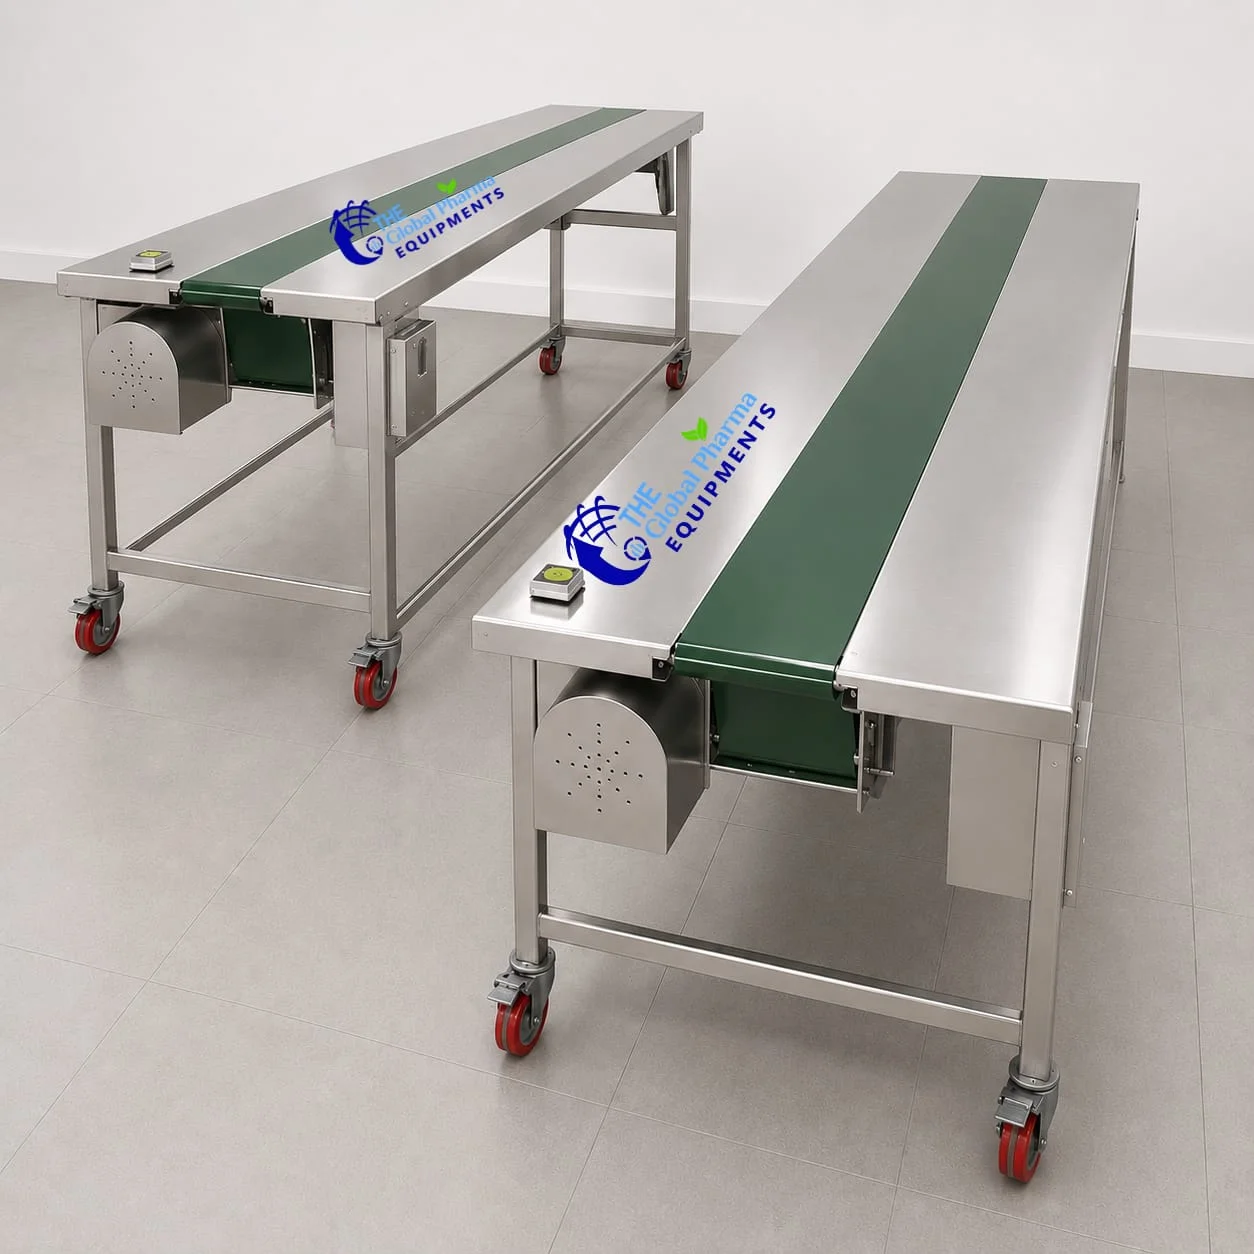
Smooth and uninterrupted product movement is essential for improving packaging e...

Well-designed furniture plays an important role in maintaining organized, hygien...
Safe and convenient access to elevated platforms, machinery, conveyors, producti...
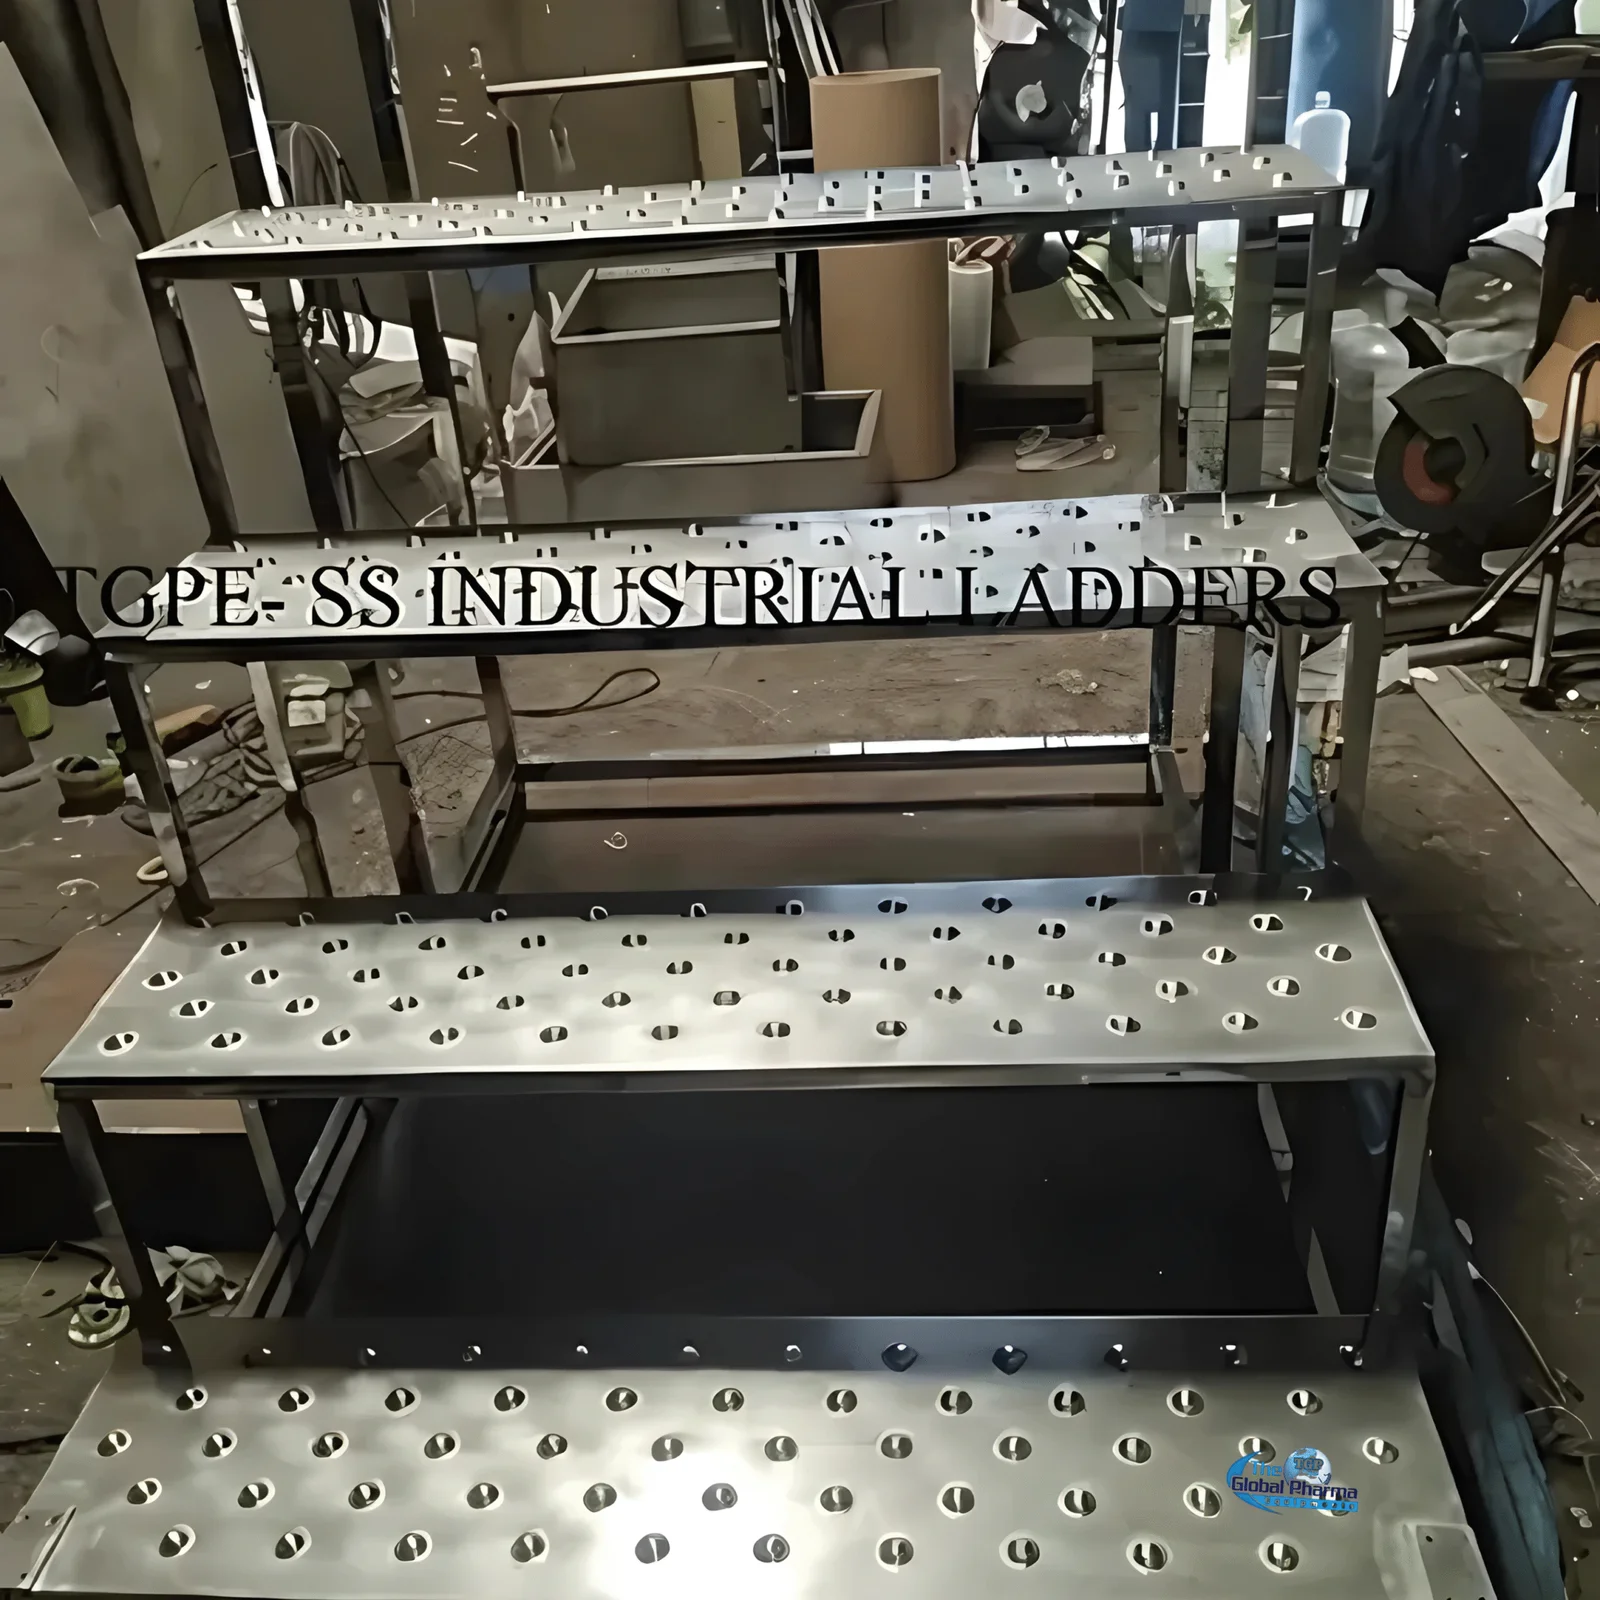
Safe access to elevated work areas, machinery, storage racks, platforms, and mai...

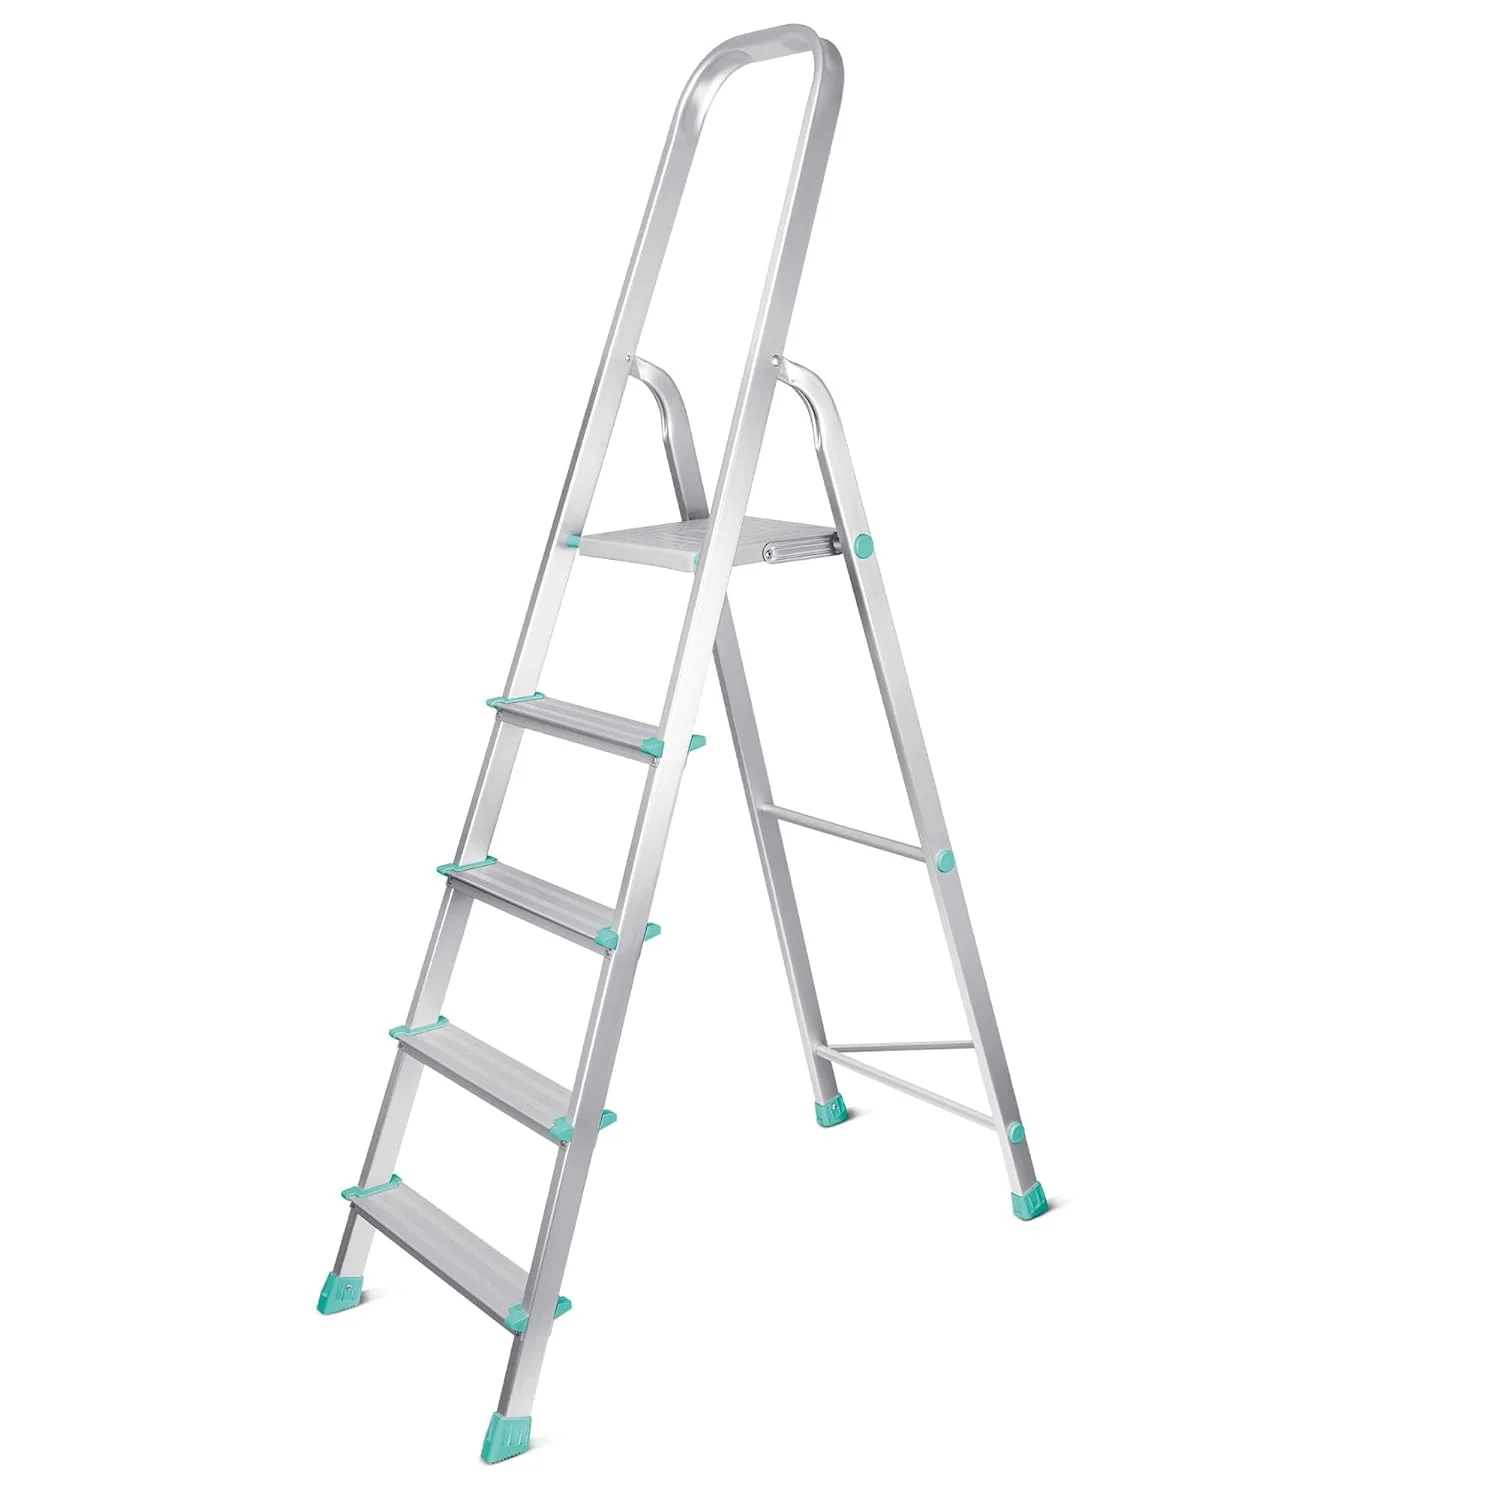
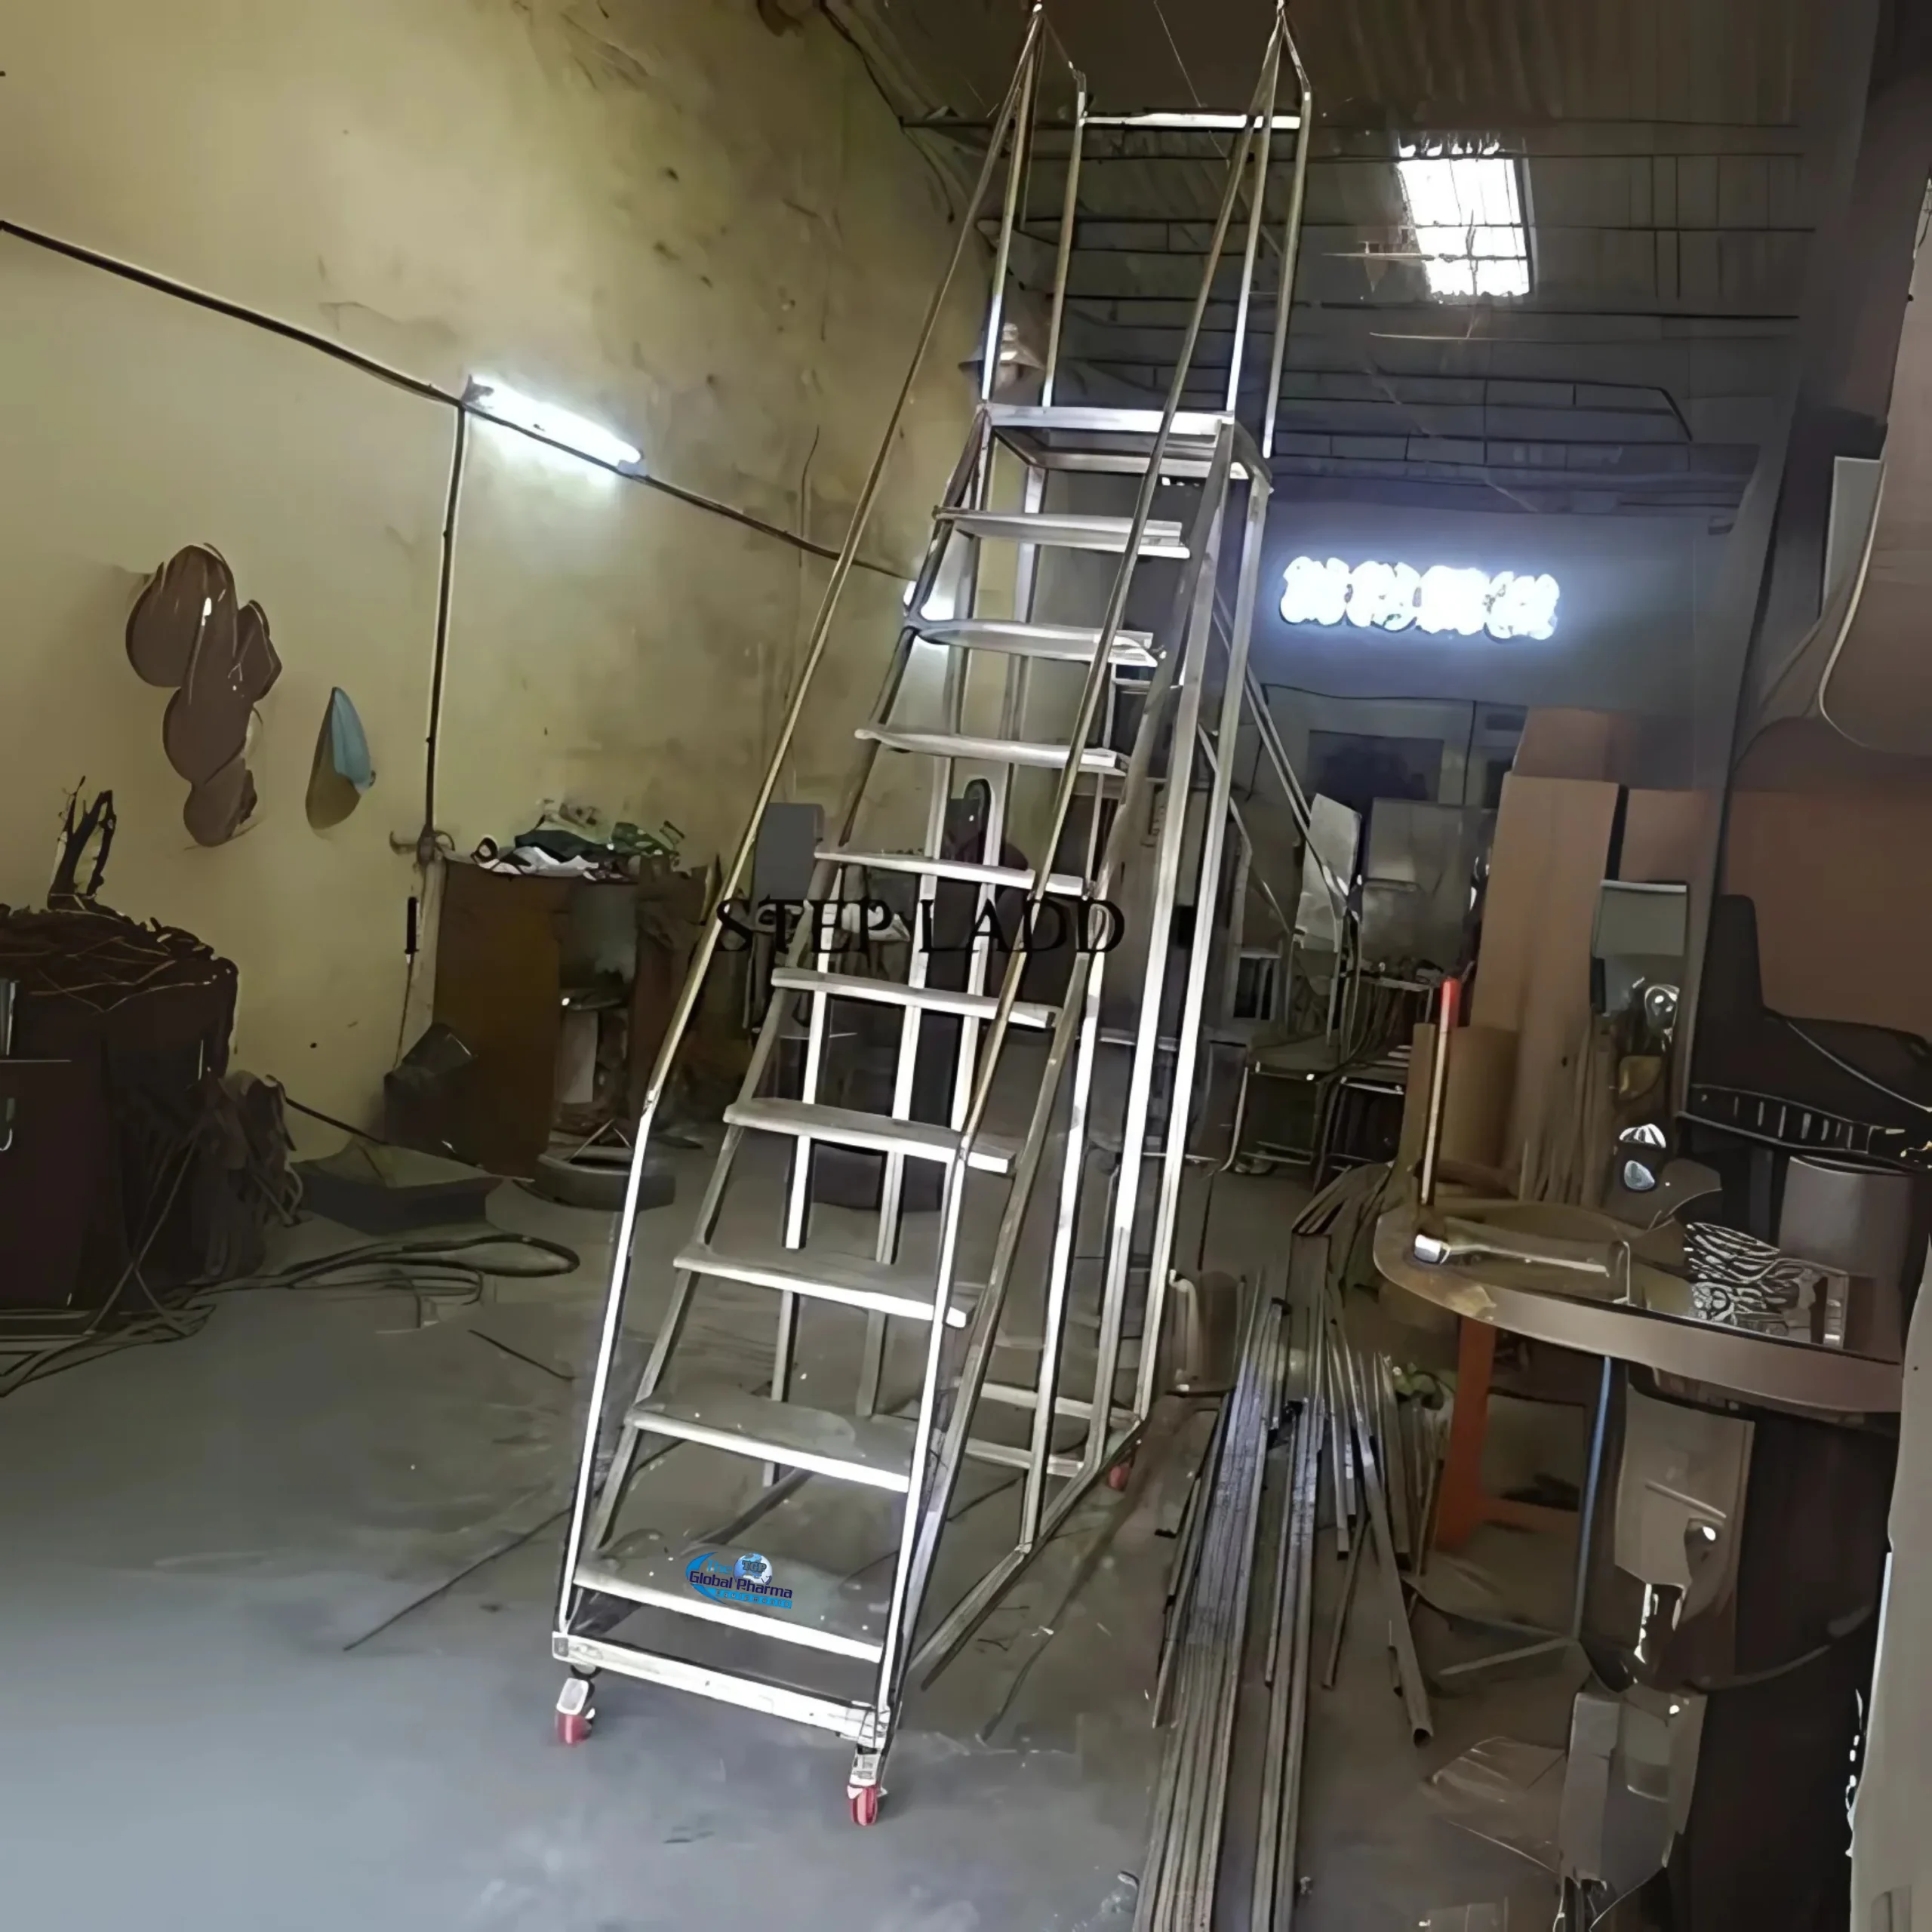
Safe access to elevated shelves, storage areas, equipment, and workstations is e...

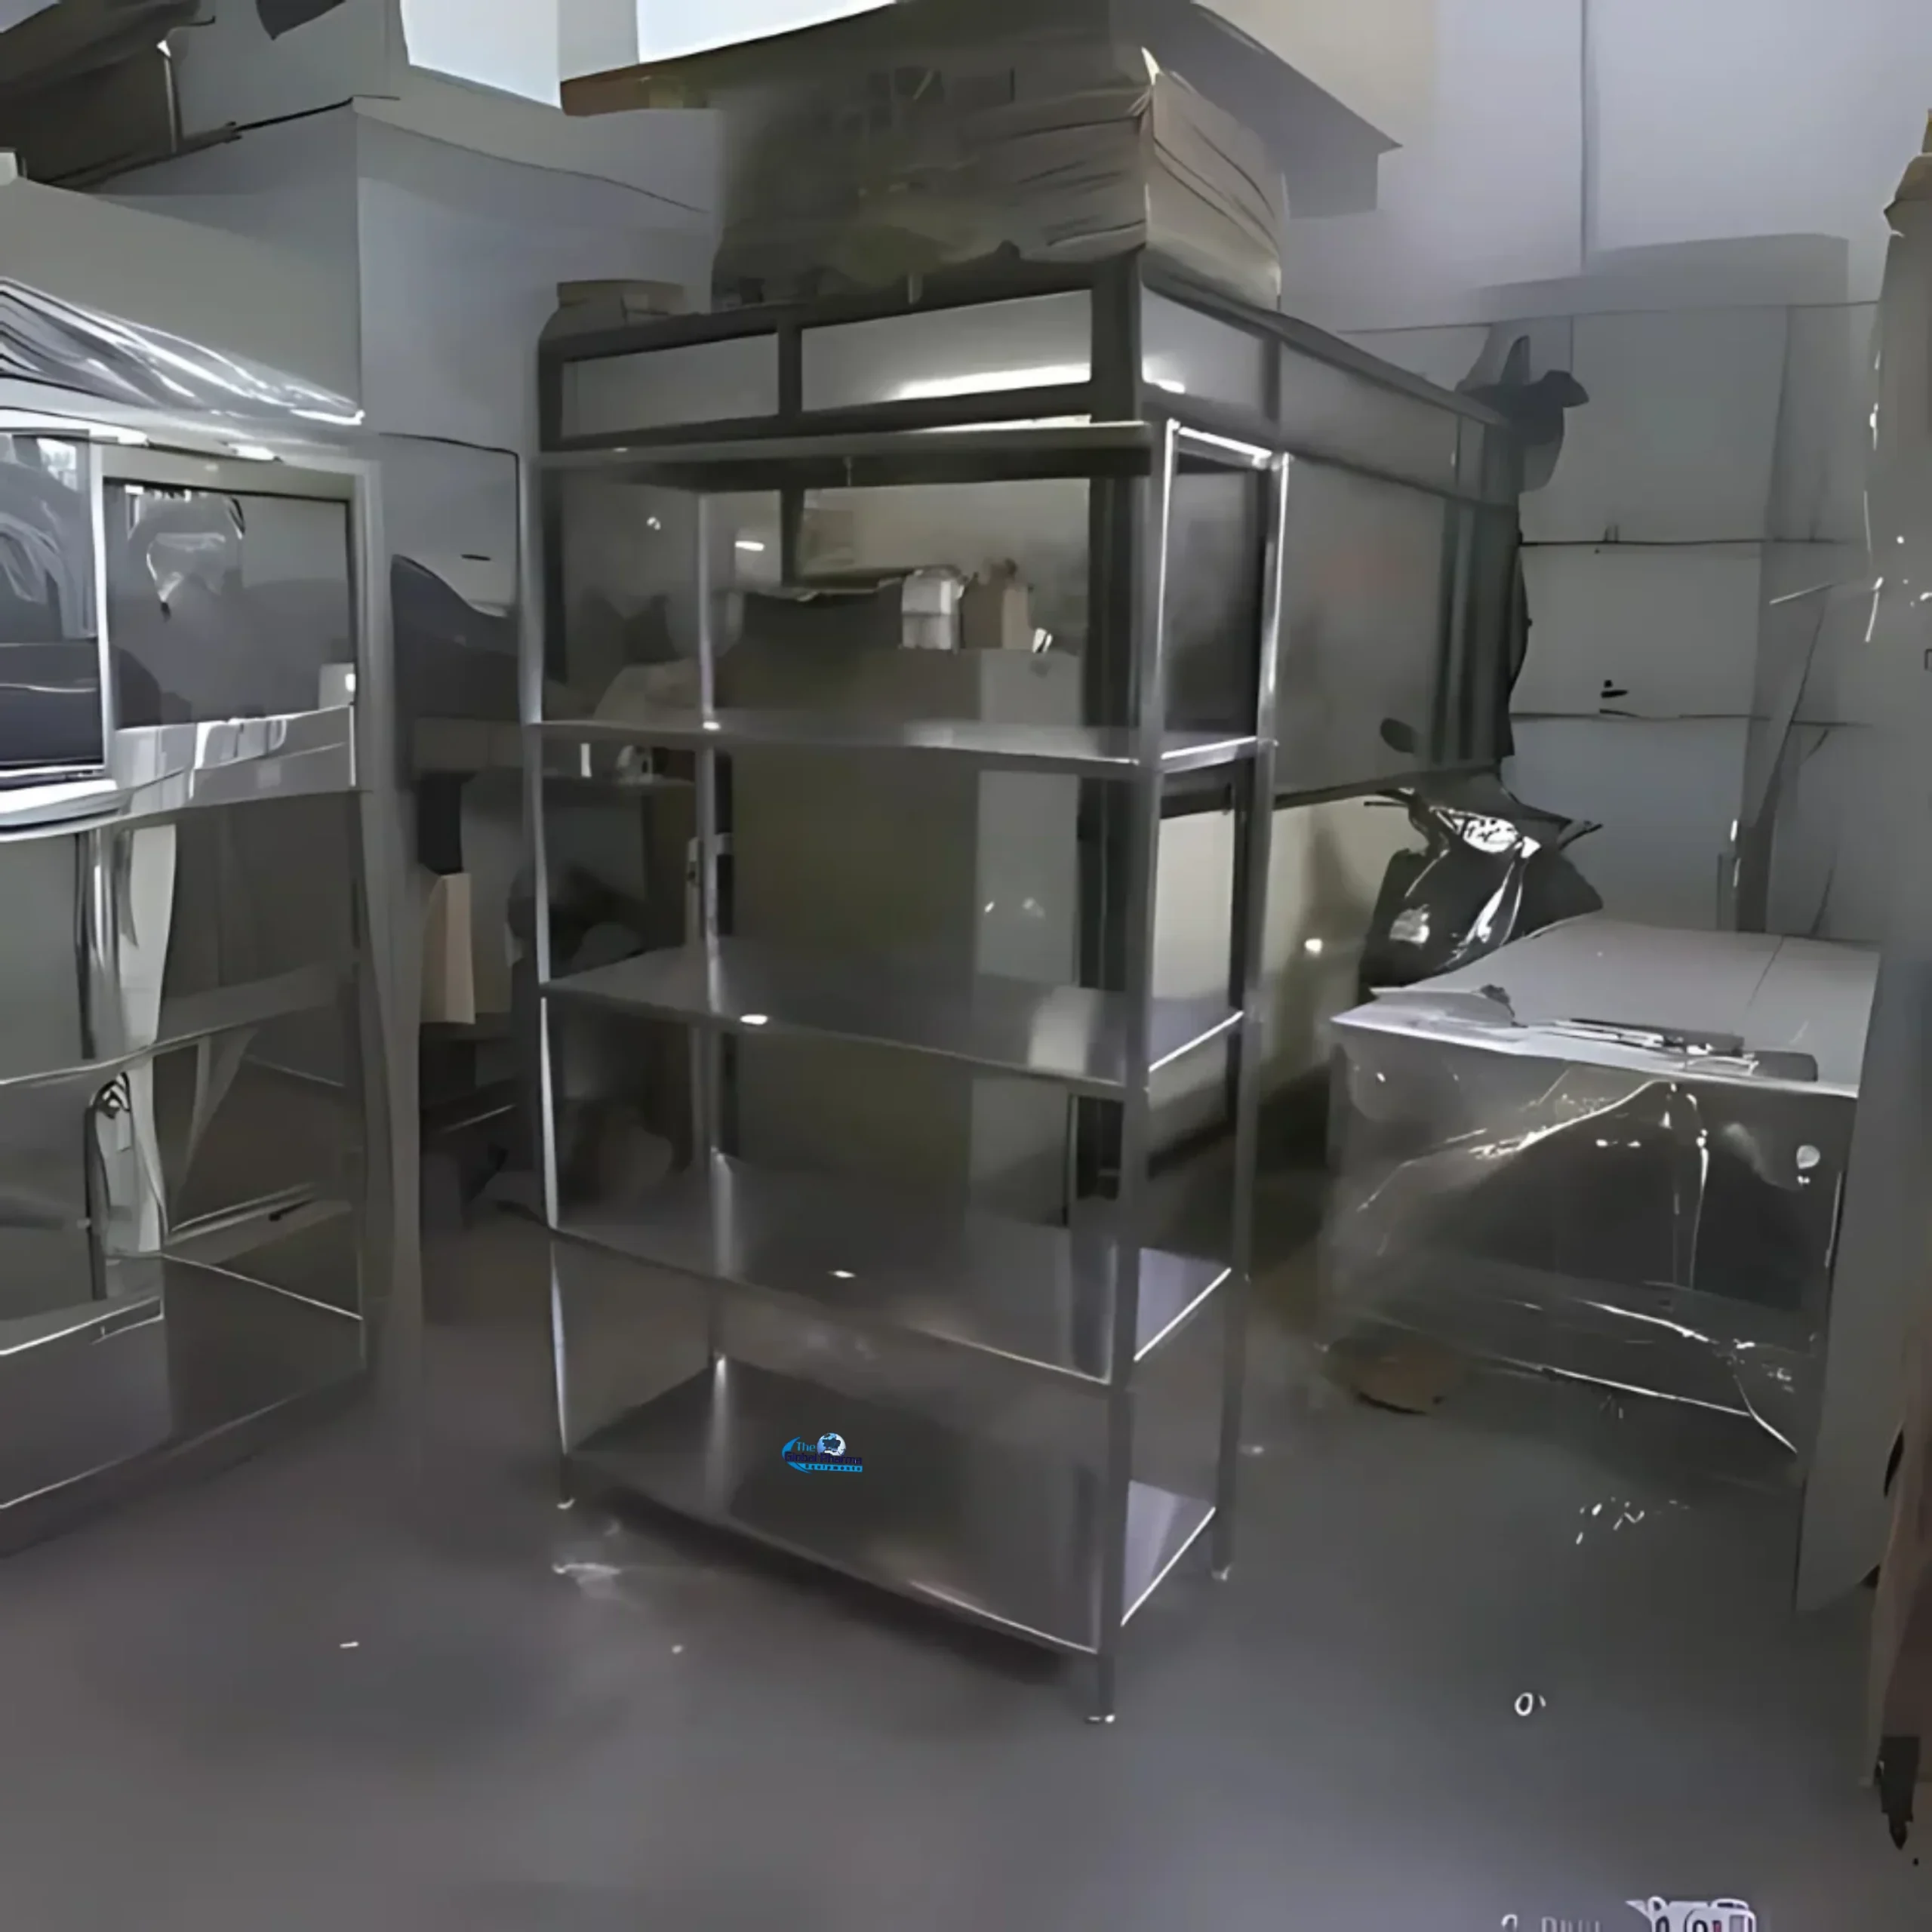
Efficient storage is essential for maintaining organized, hygienic, and producti...

Efficient storage and systematic organization are essential for maintaining prod...
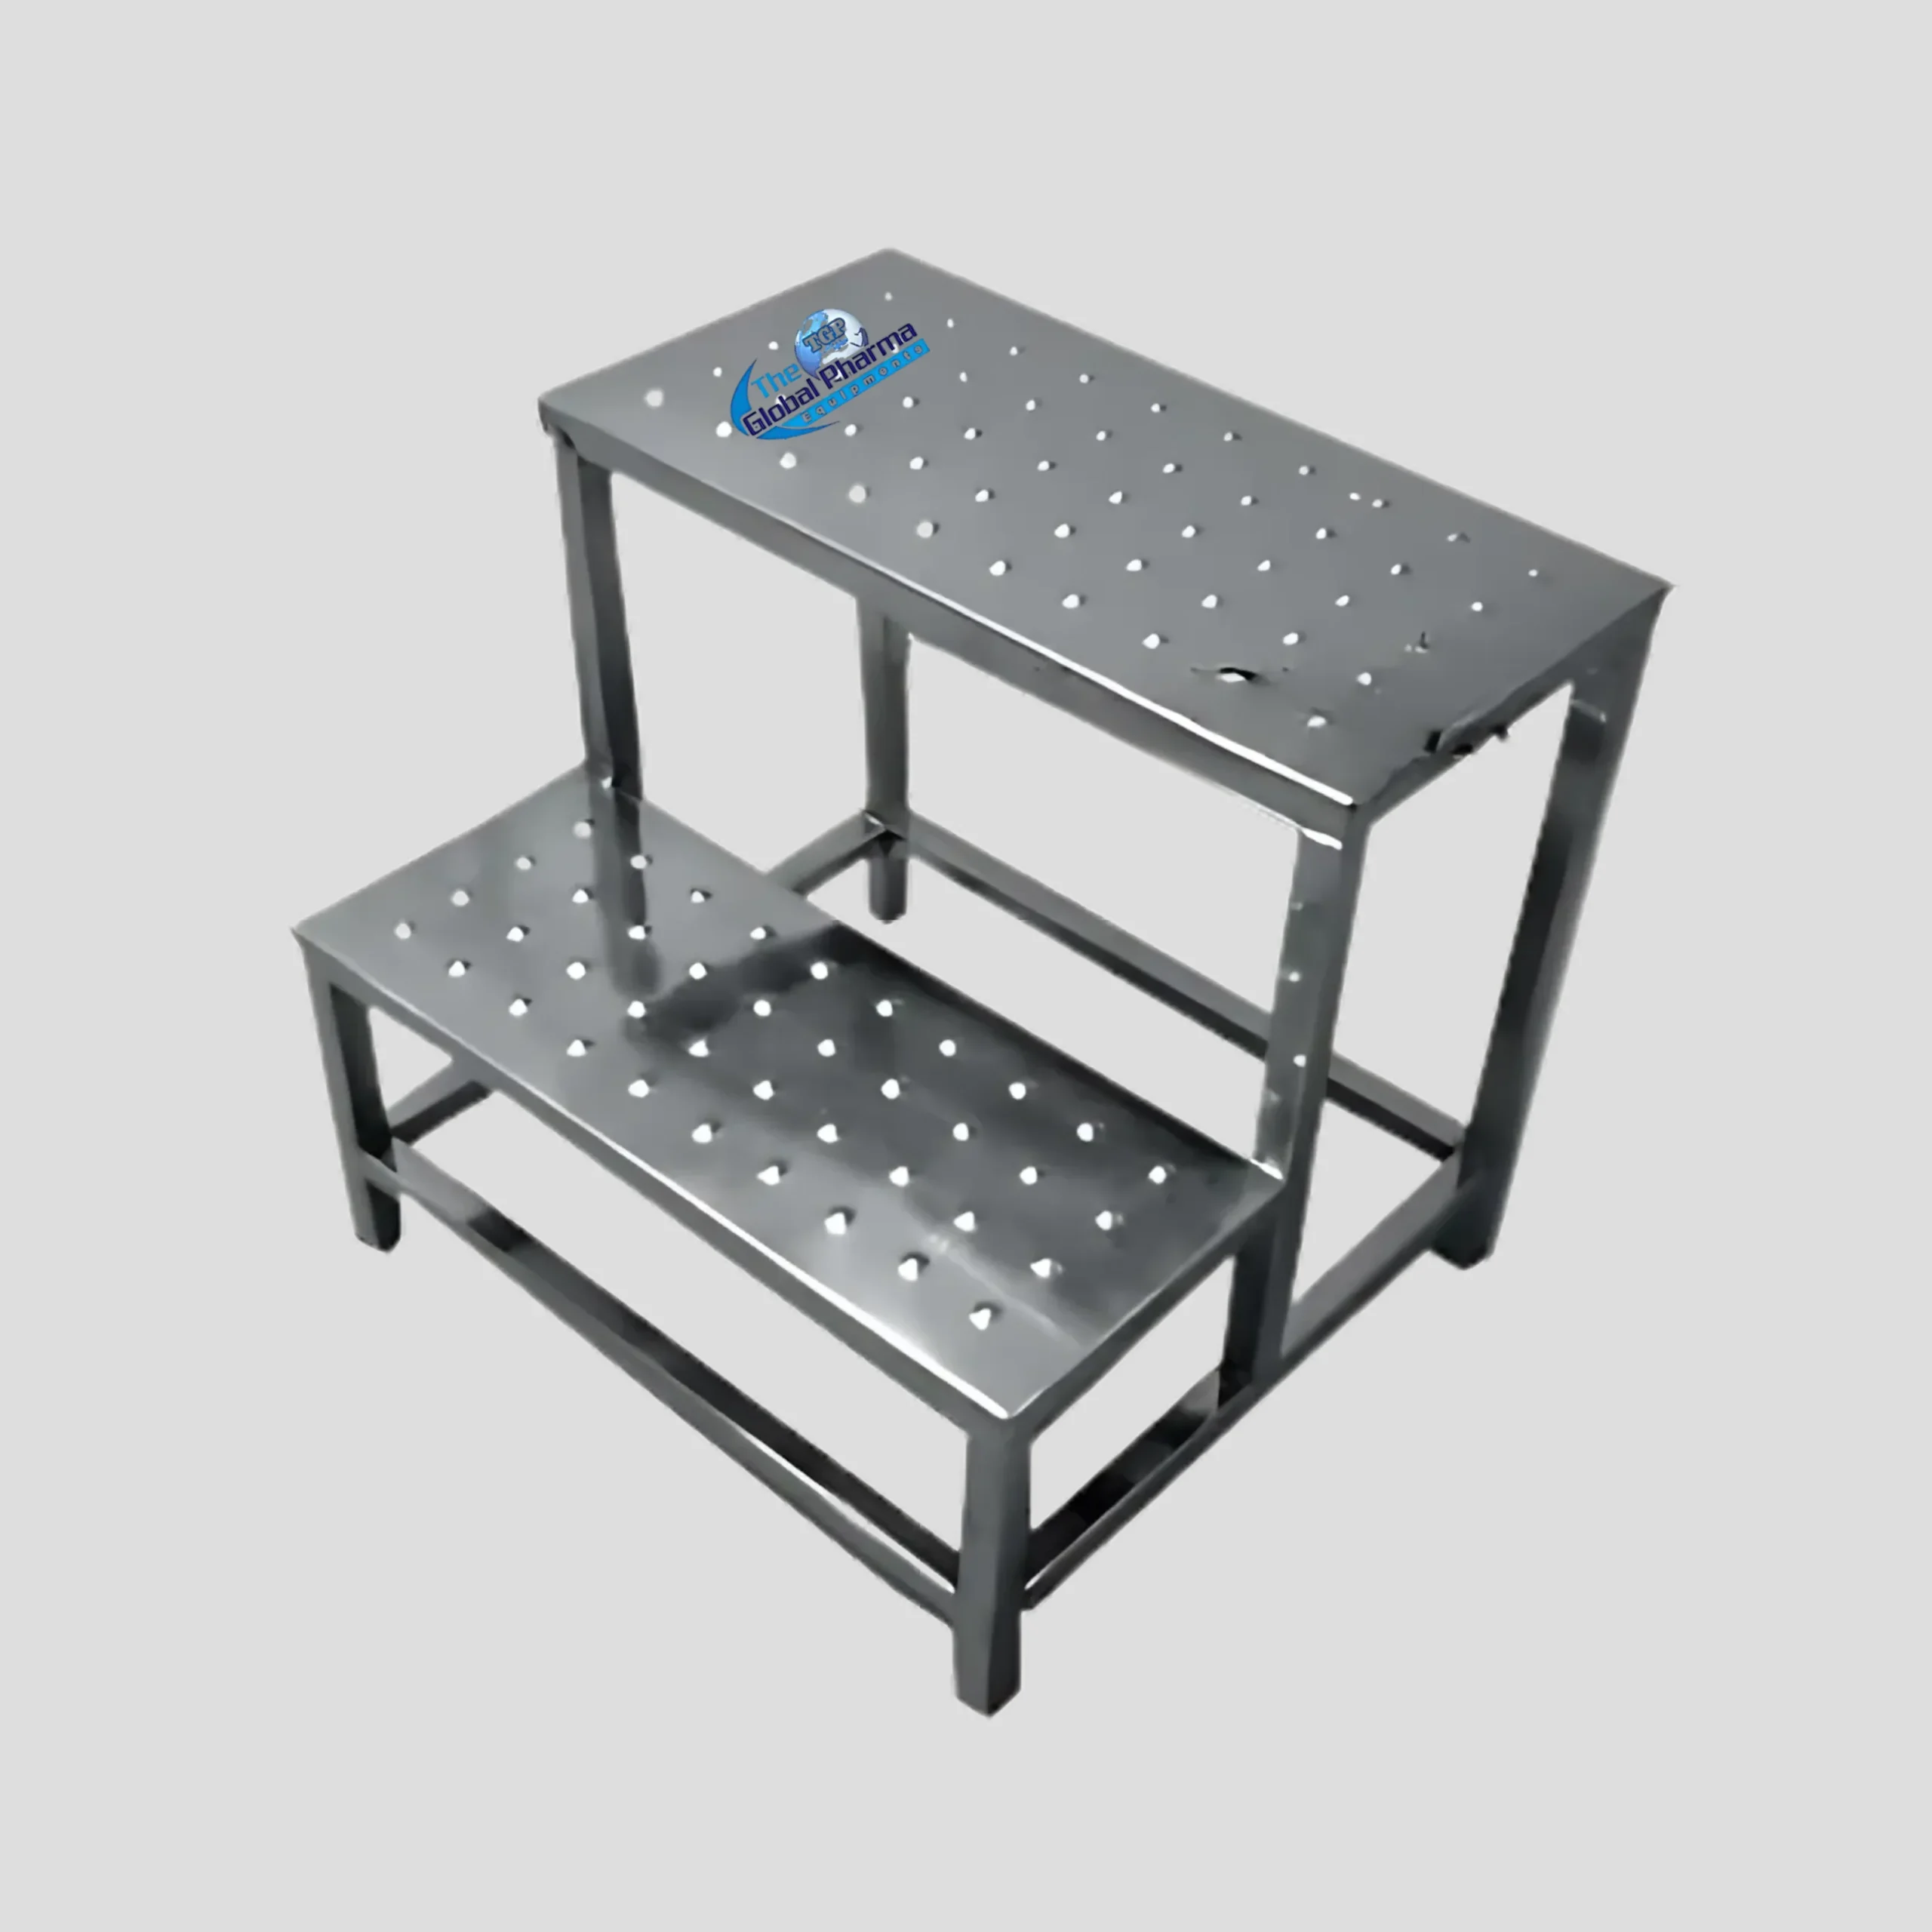
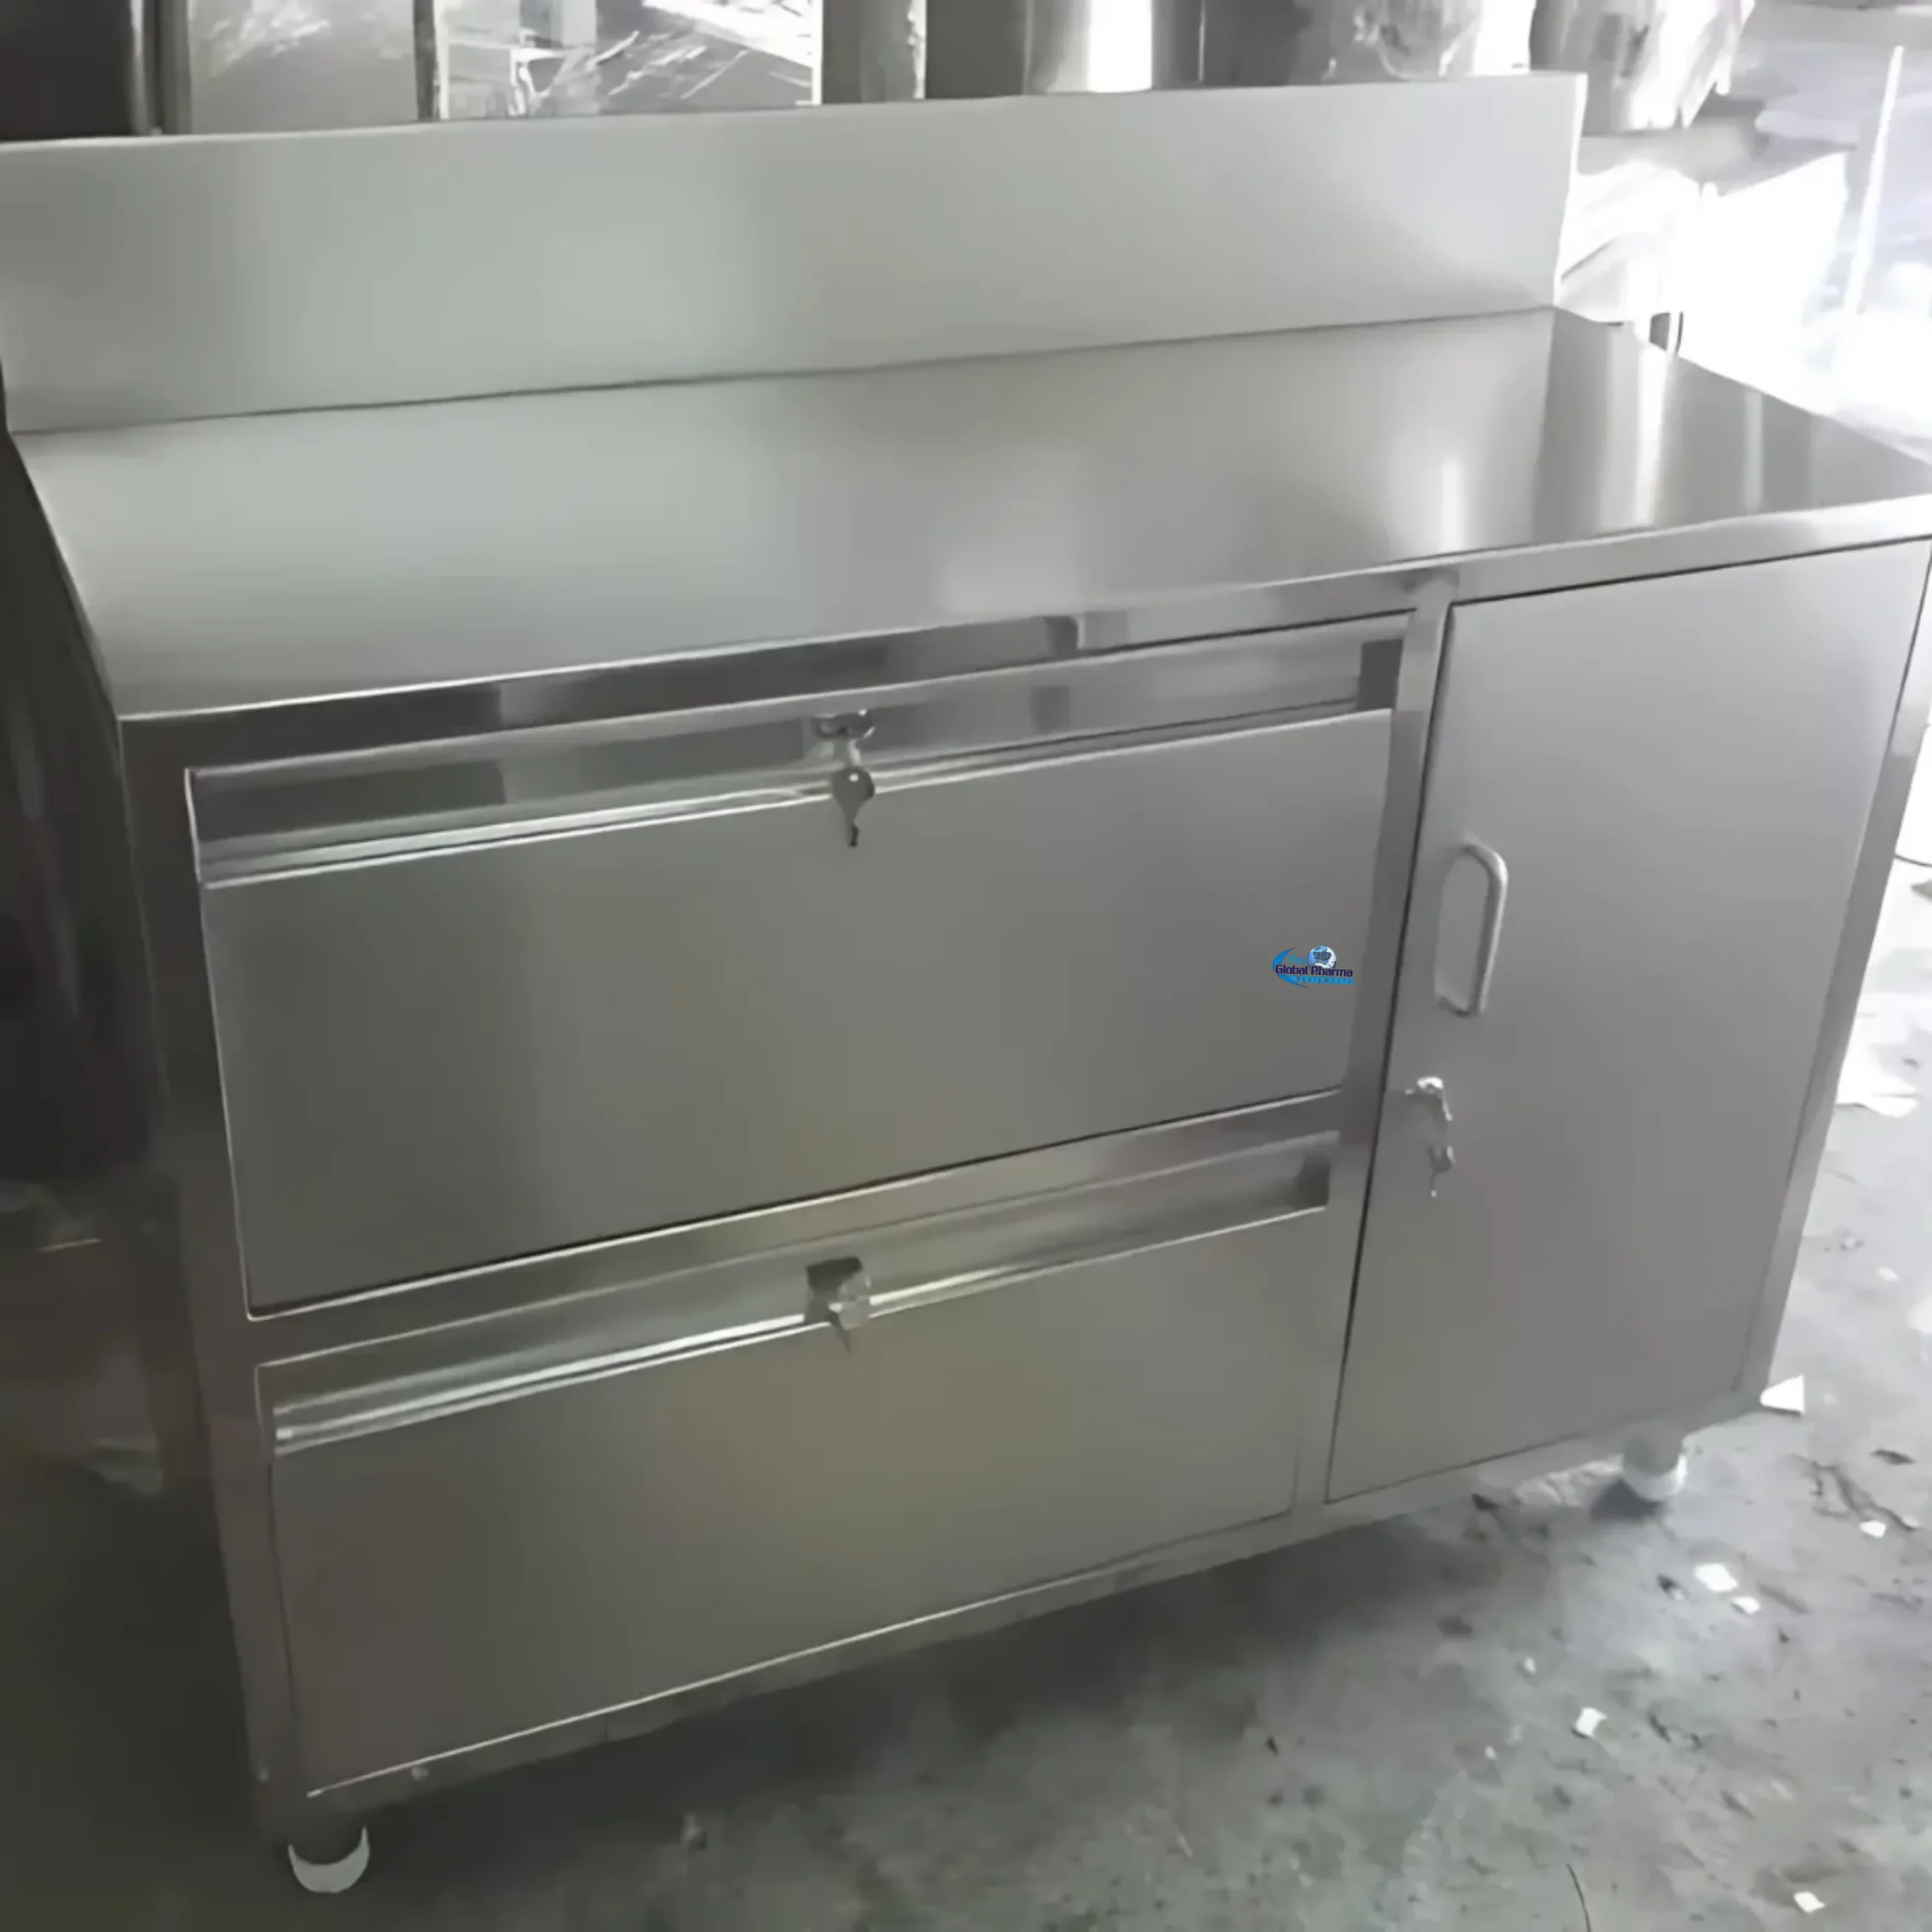
Well-designed office furniture helps create organized, efficient, and profession...

SS two step ladders are practical access equipment designed to help operators sa...
Stainless Steel Curved Cross Over Benches are specialized cleanroom and pharmace...
Stainless steel foldable ladders are practical access solutions used in pharmace...
Stainless steel furniture is widely used in pharmaceutical plants, hospitals, la...
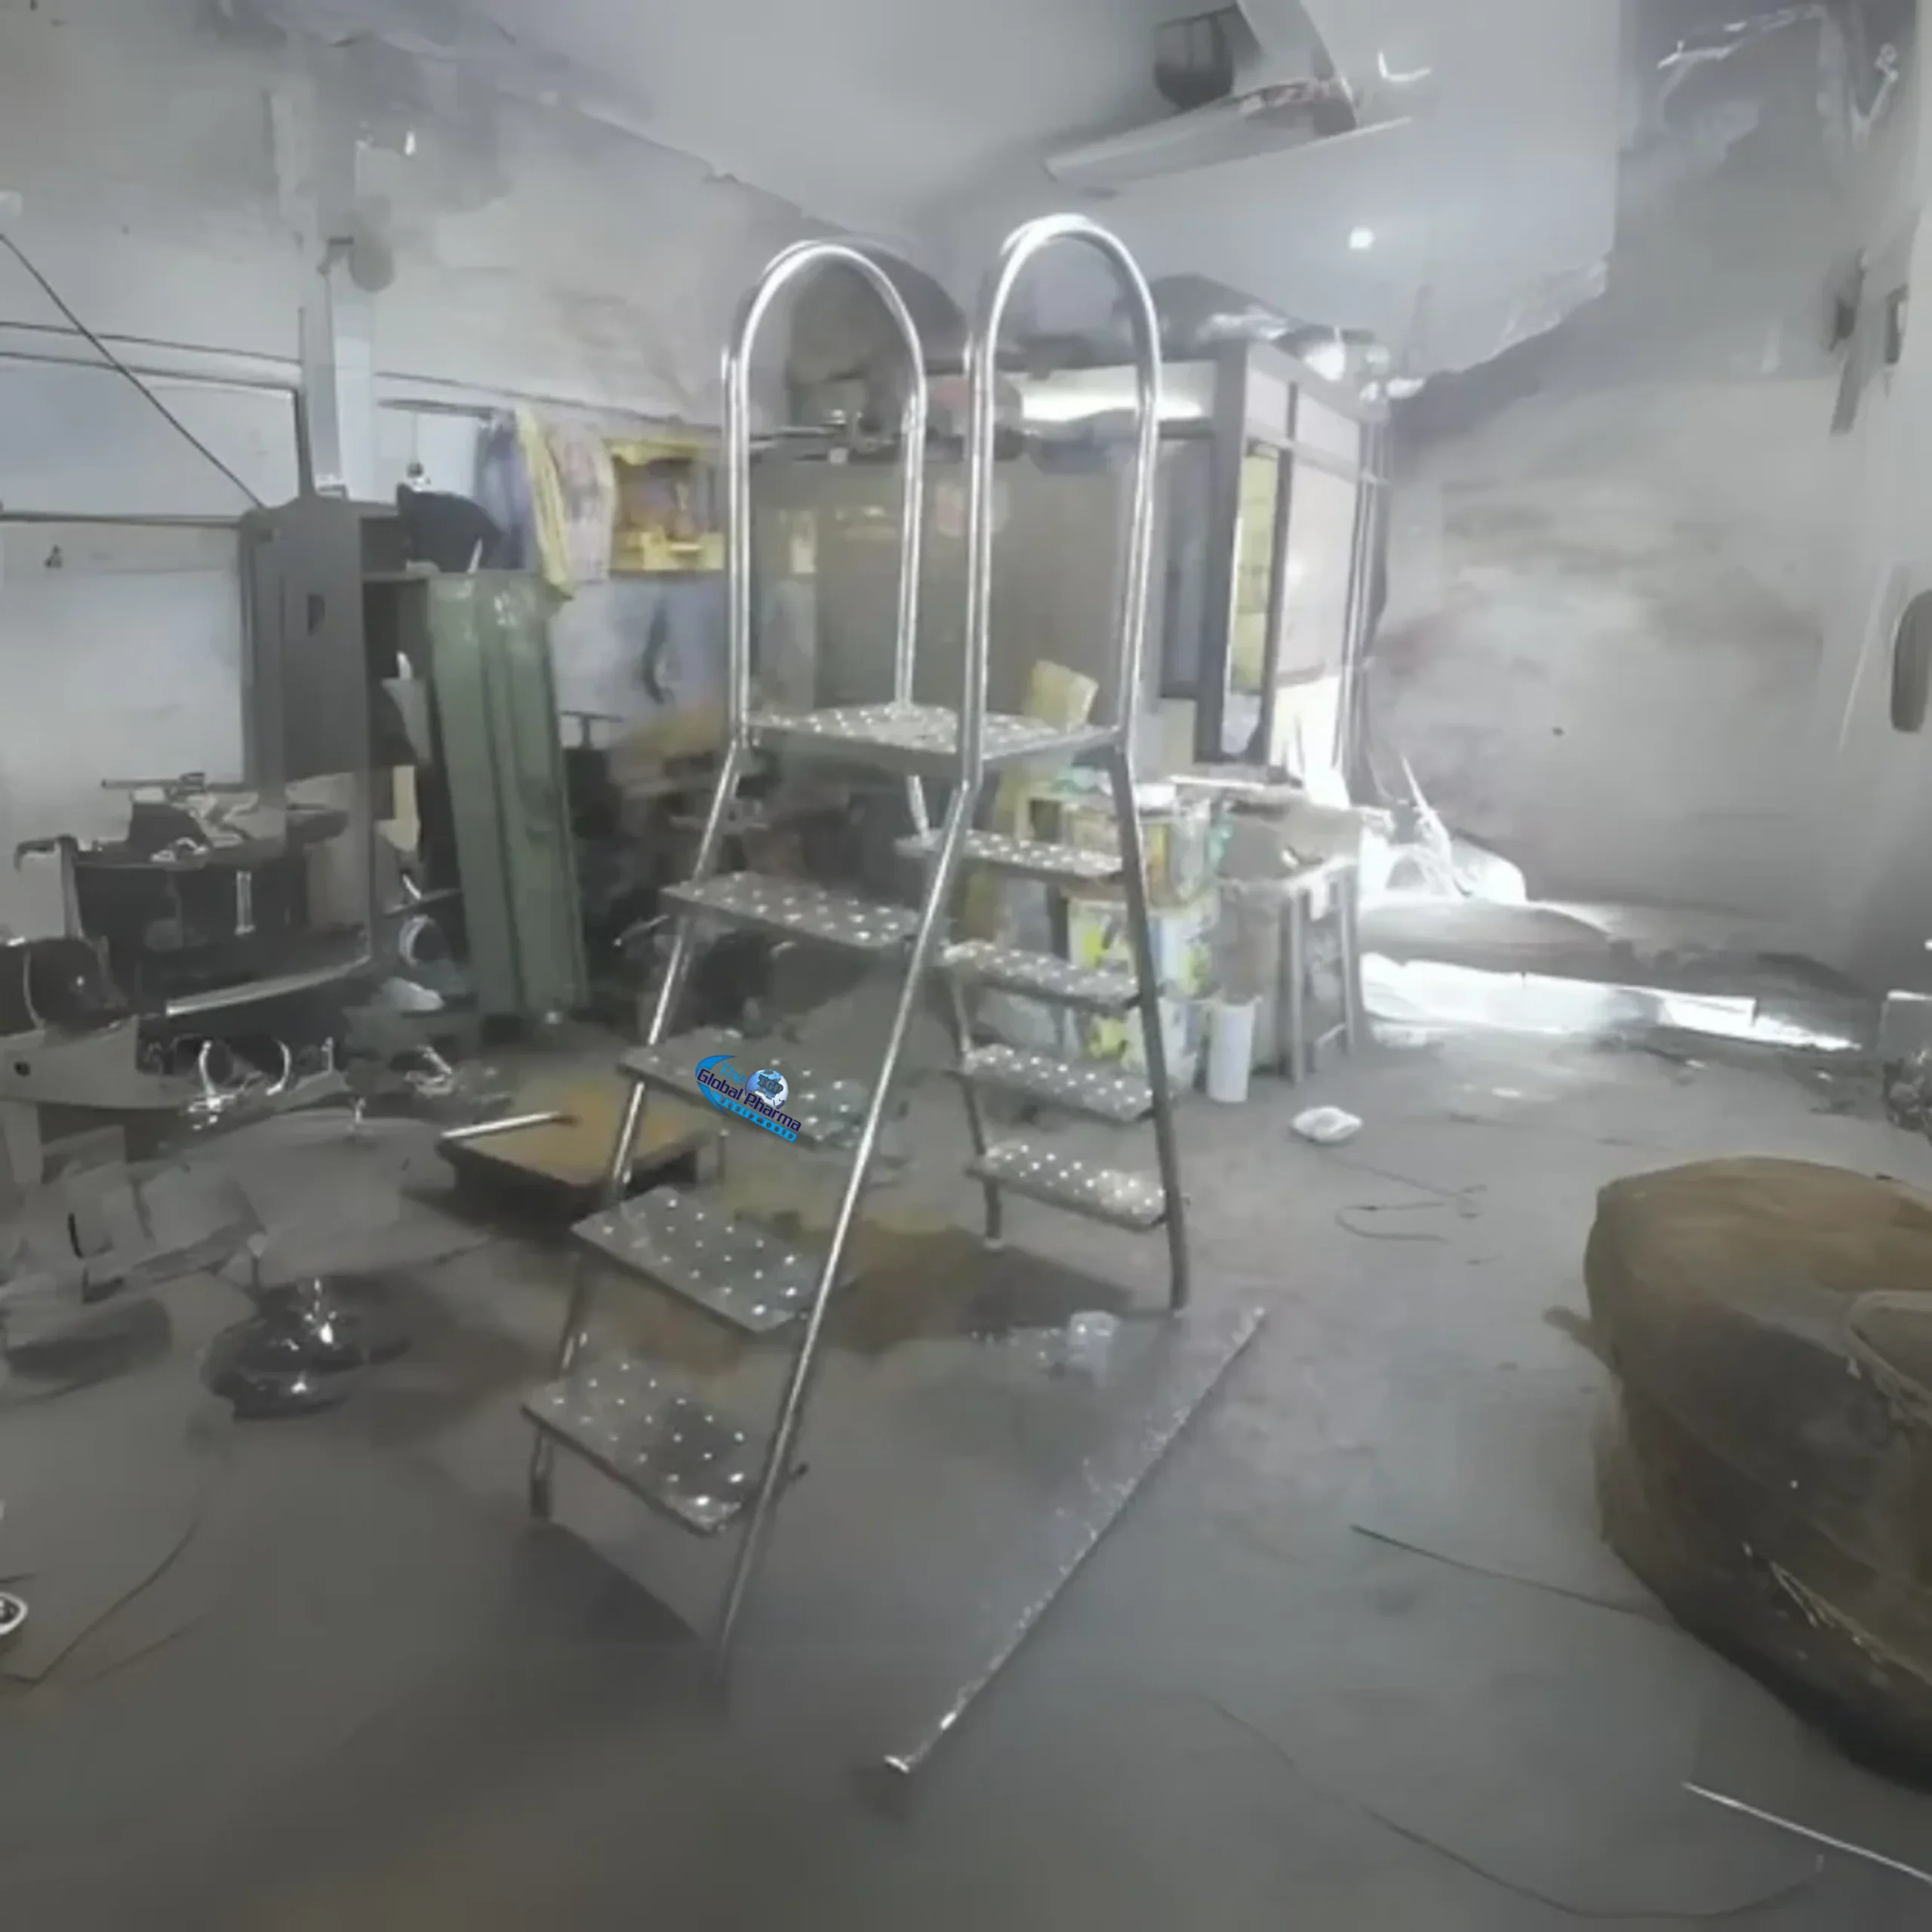
Stainless steel ladders are essential access solutions used for reaching elevate...
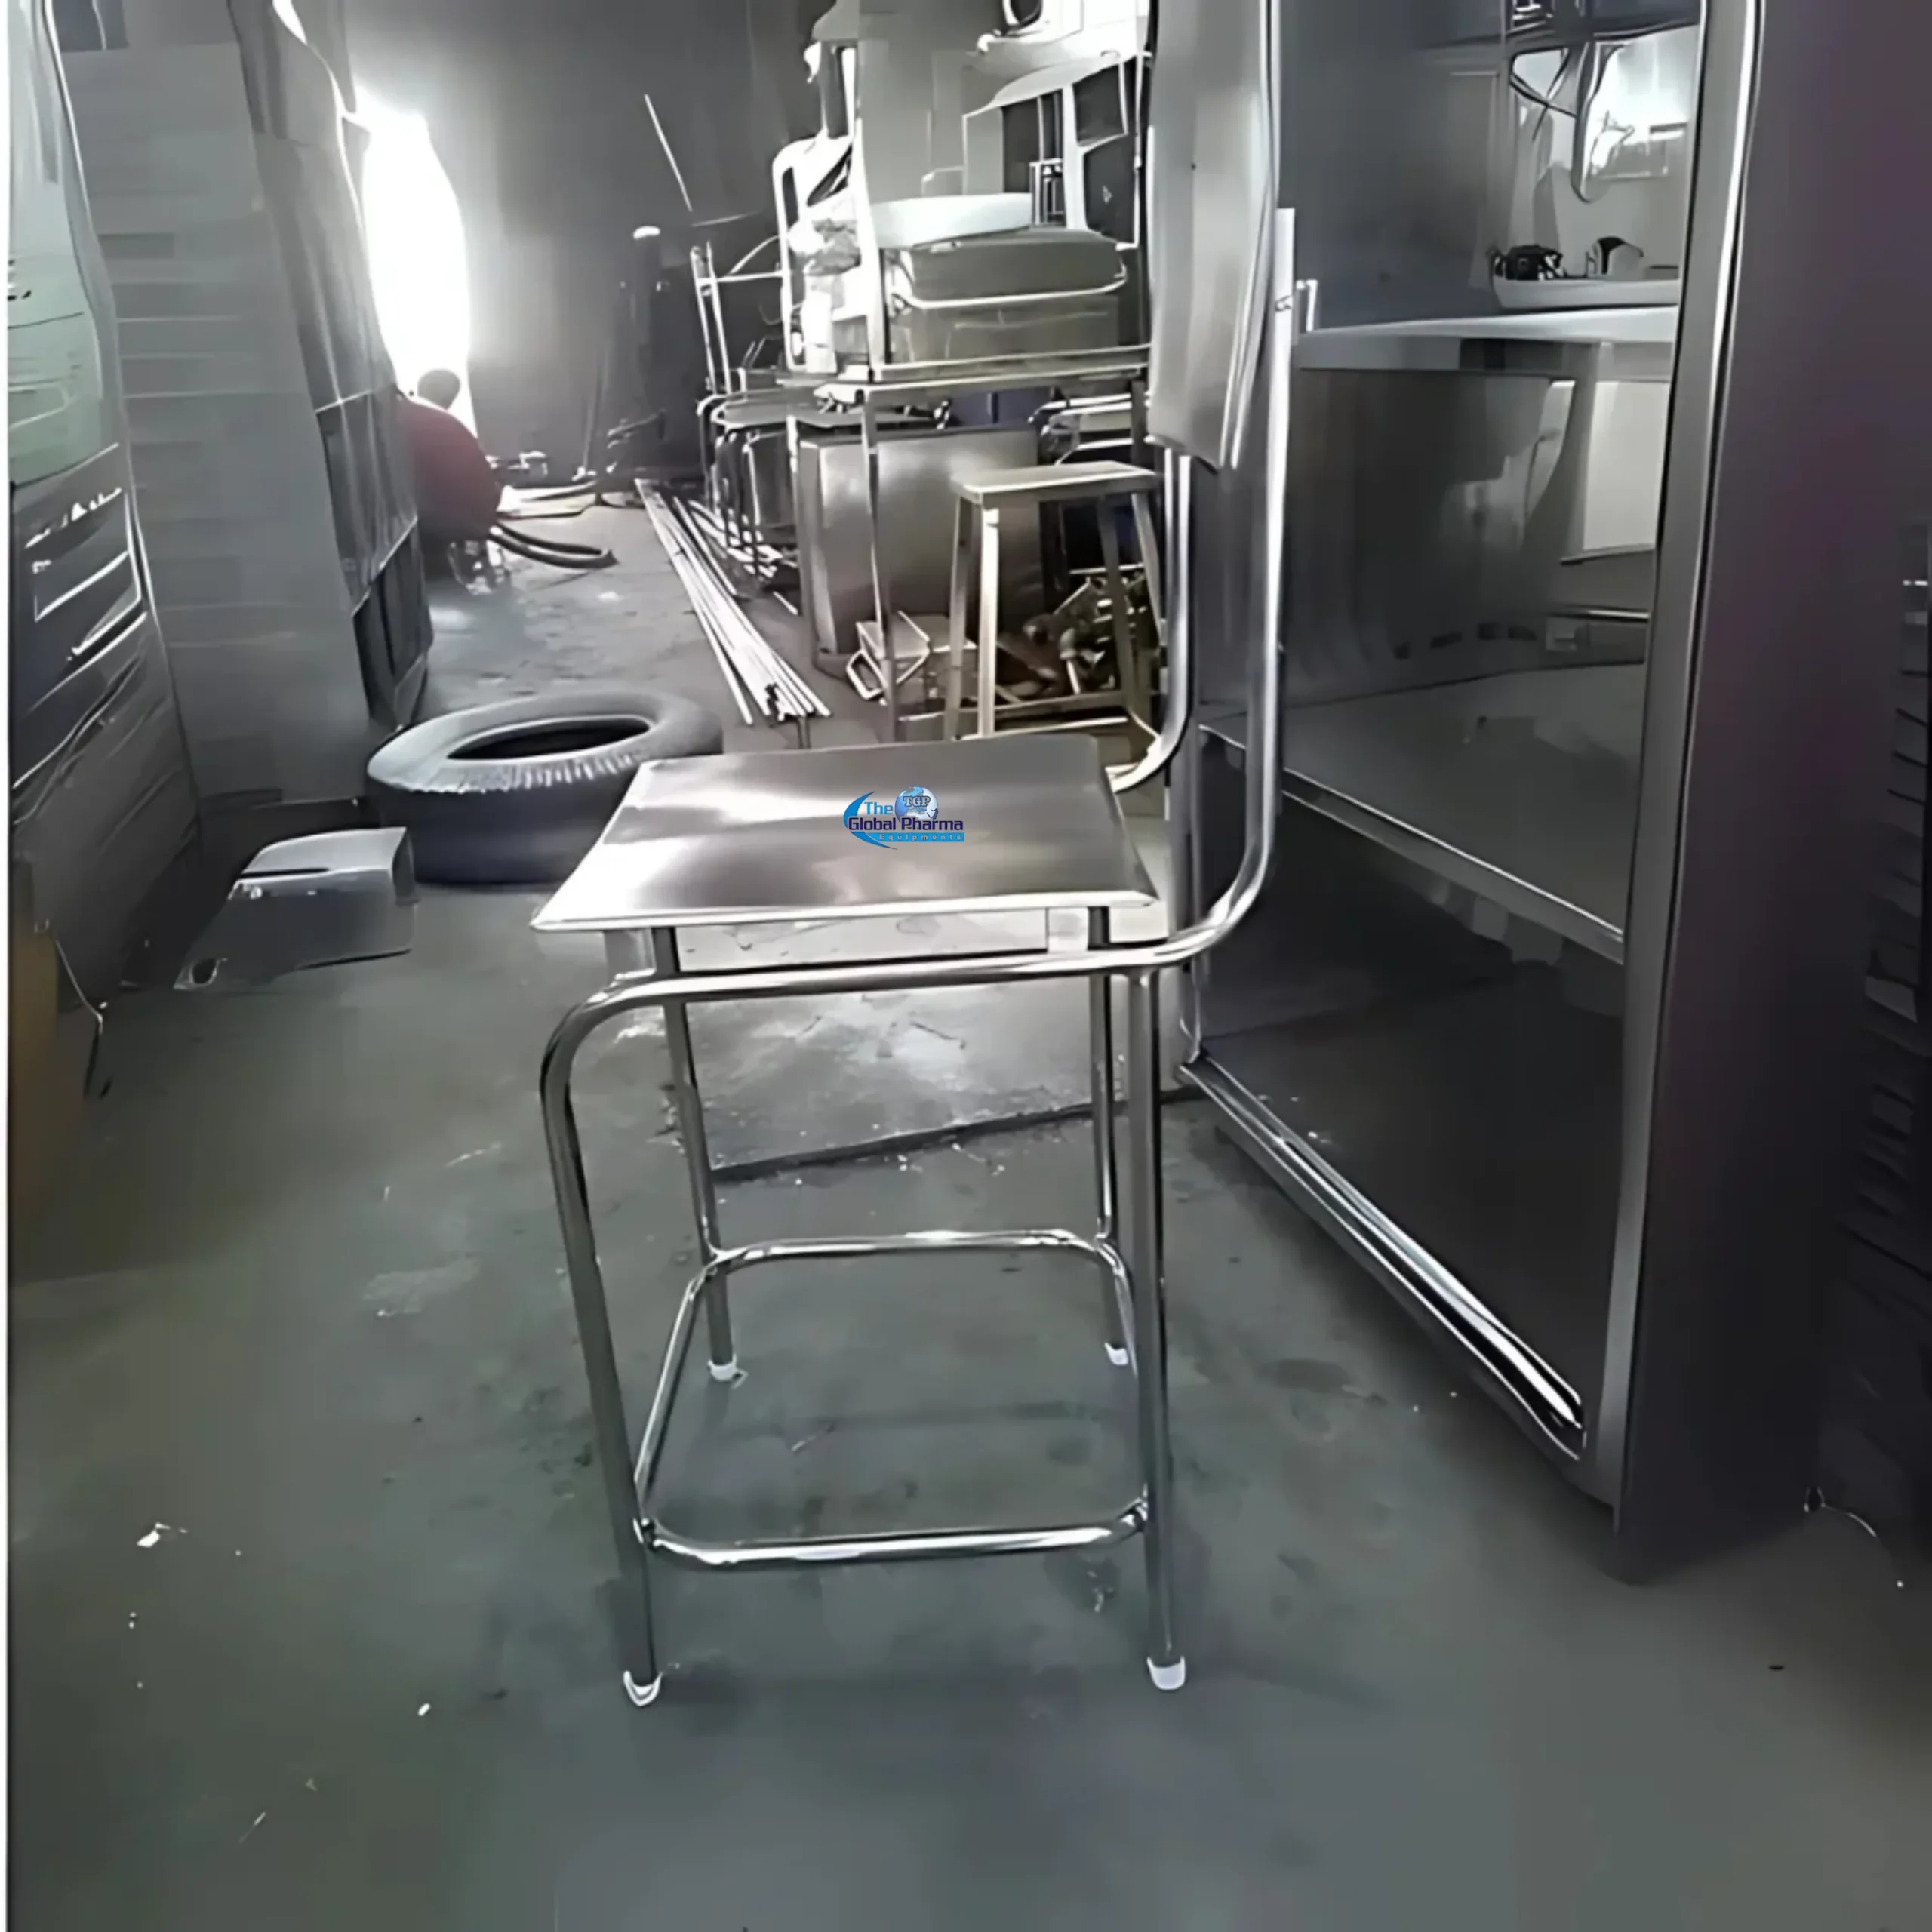
Stainless Steel Packing Chairs are practical industrial seating solutions design...

Stainless Steel Racks are essential storage solutions designed to organize raw m...
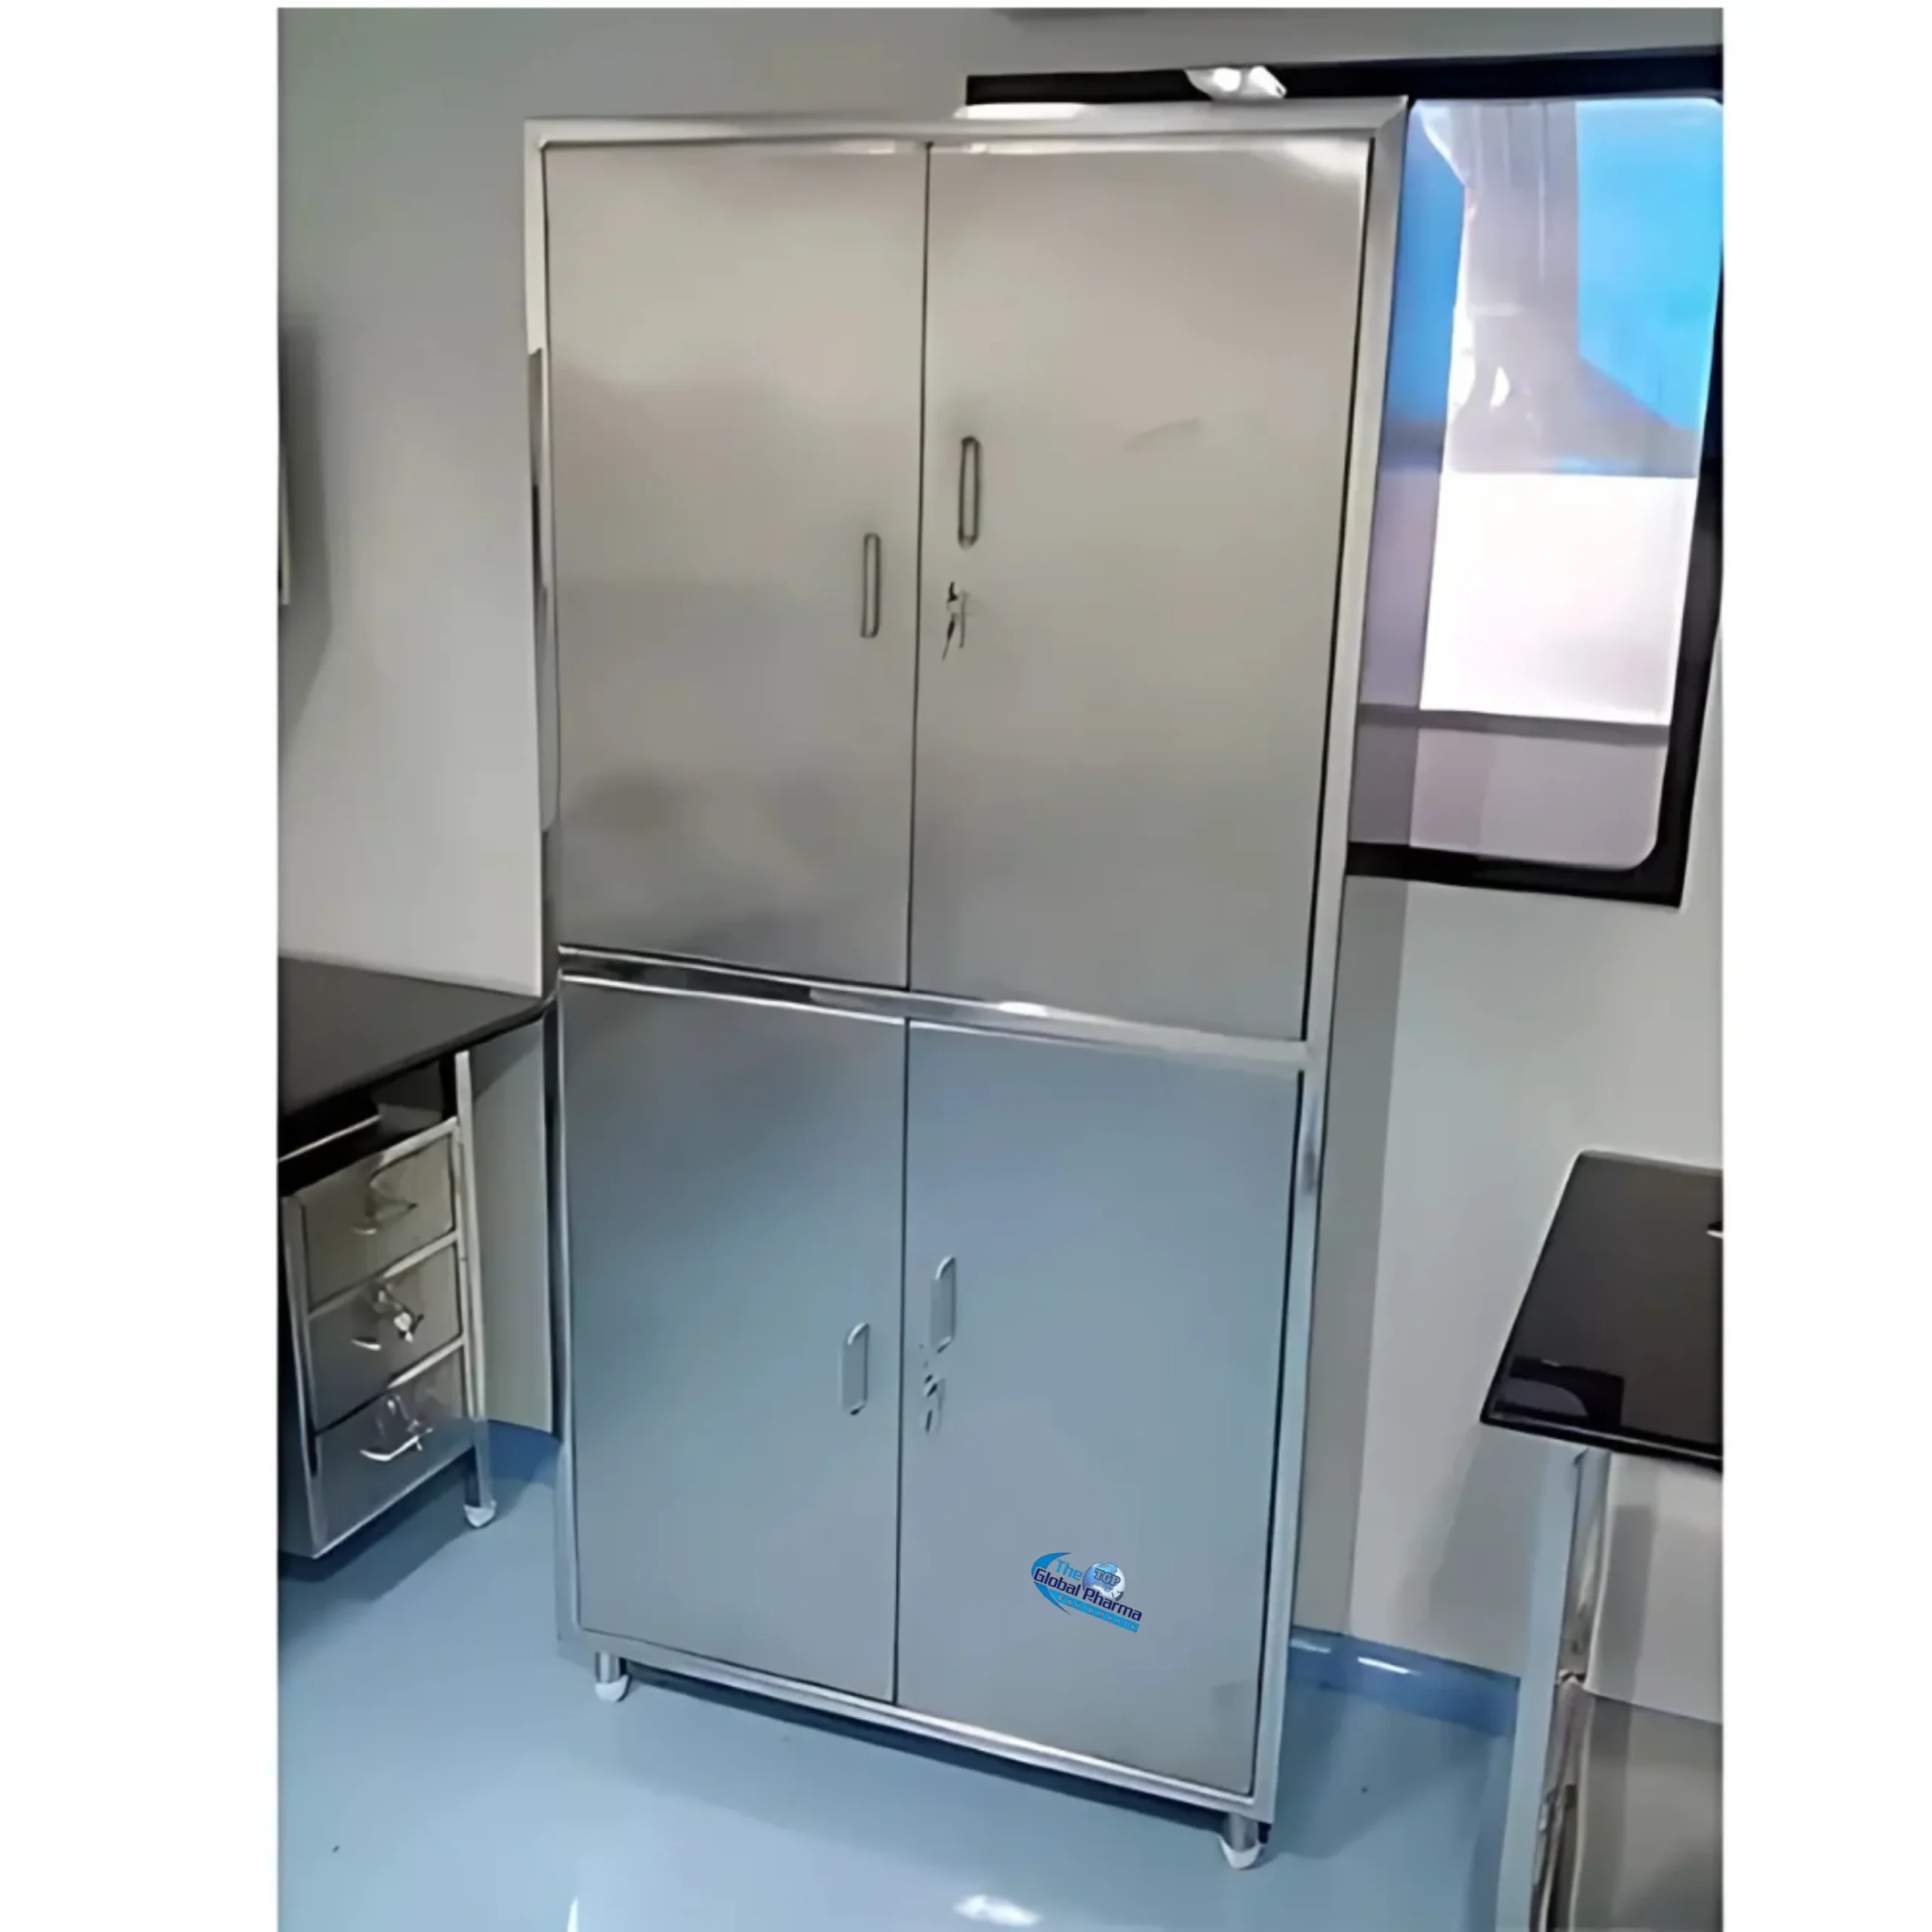
Stainless Steel Storage Cabinets are essential storage solutions designed to saf...
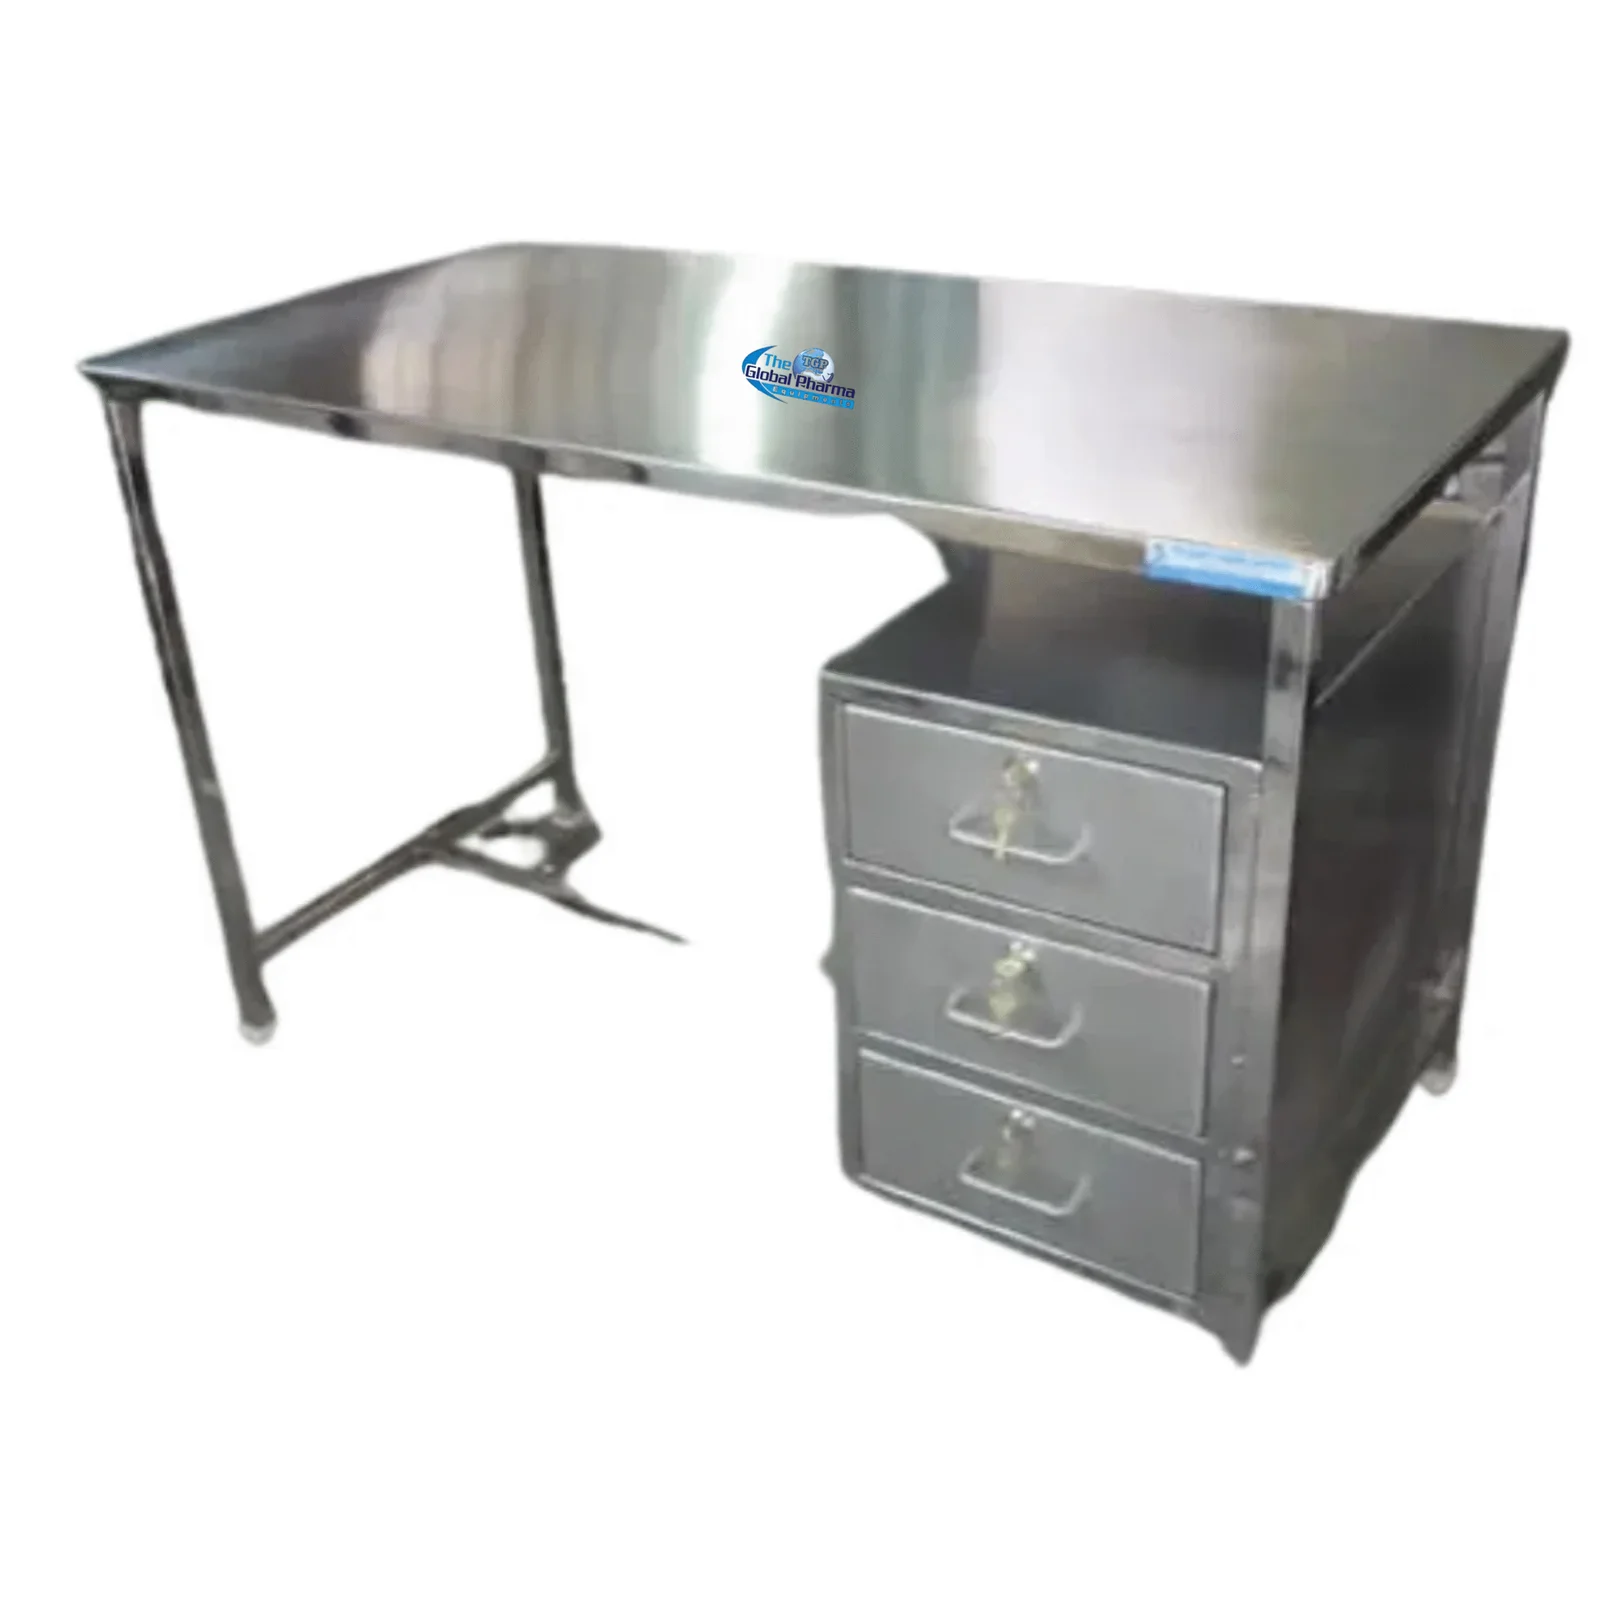
Stainless Steel Tables are essential work surfaces designed for pharmaceutical m...
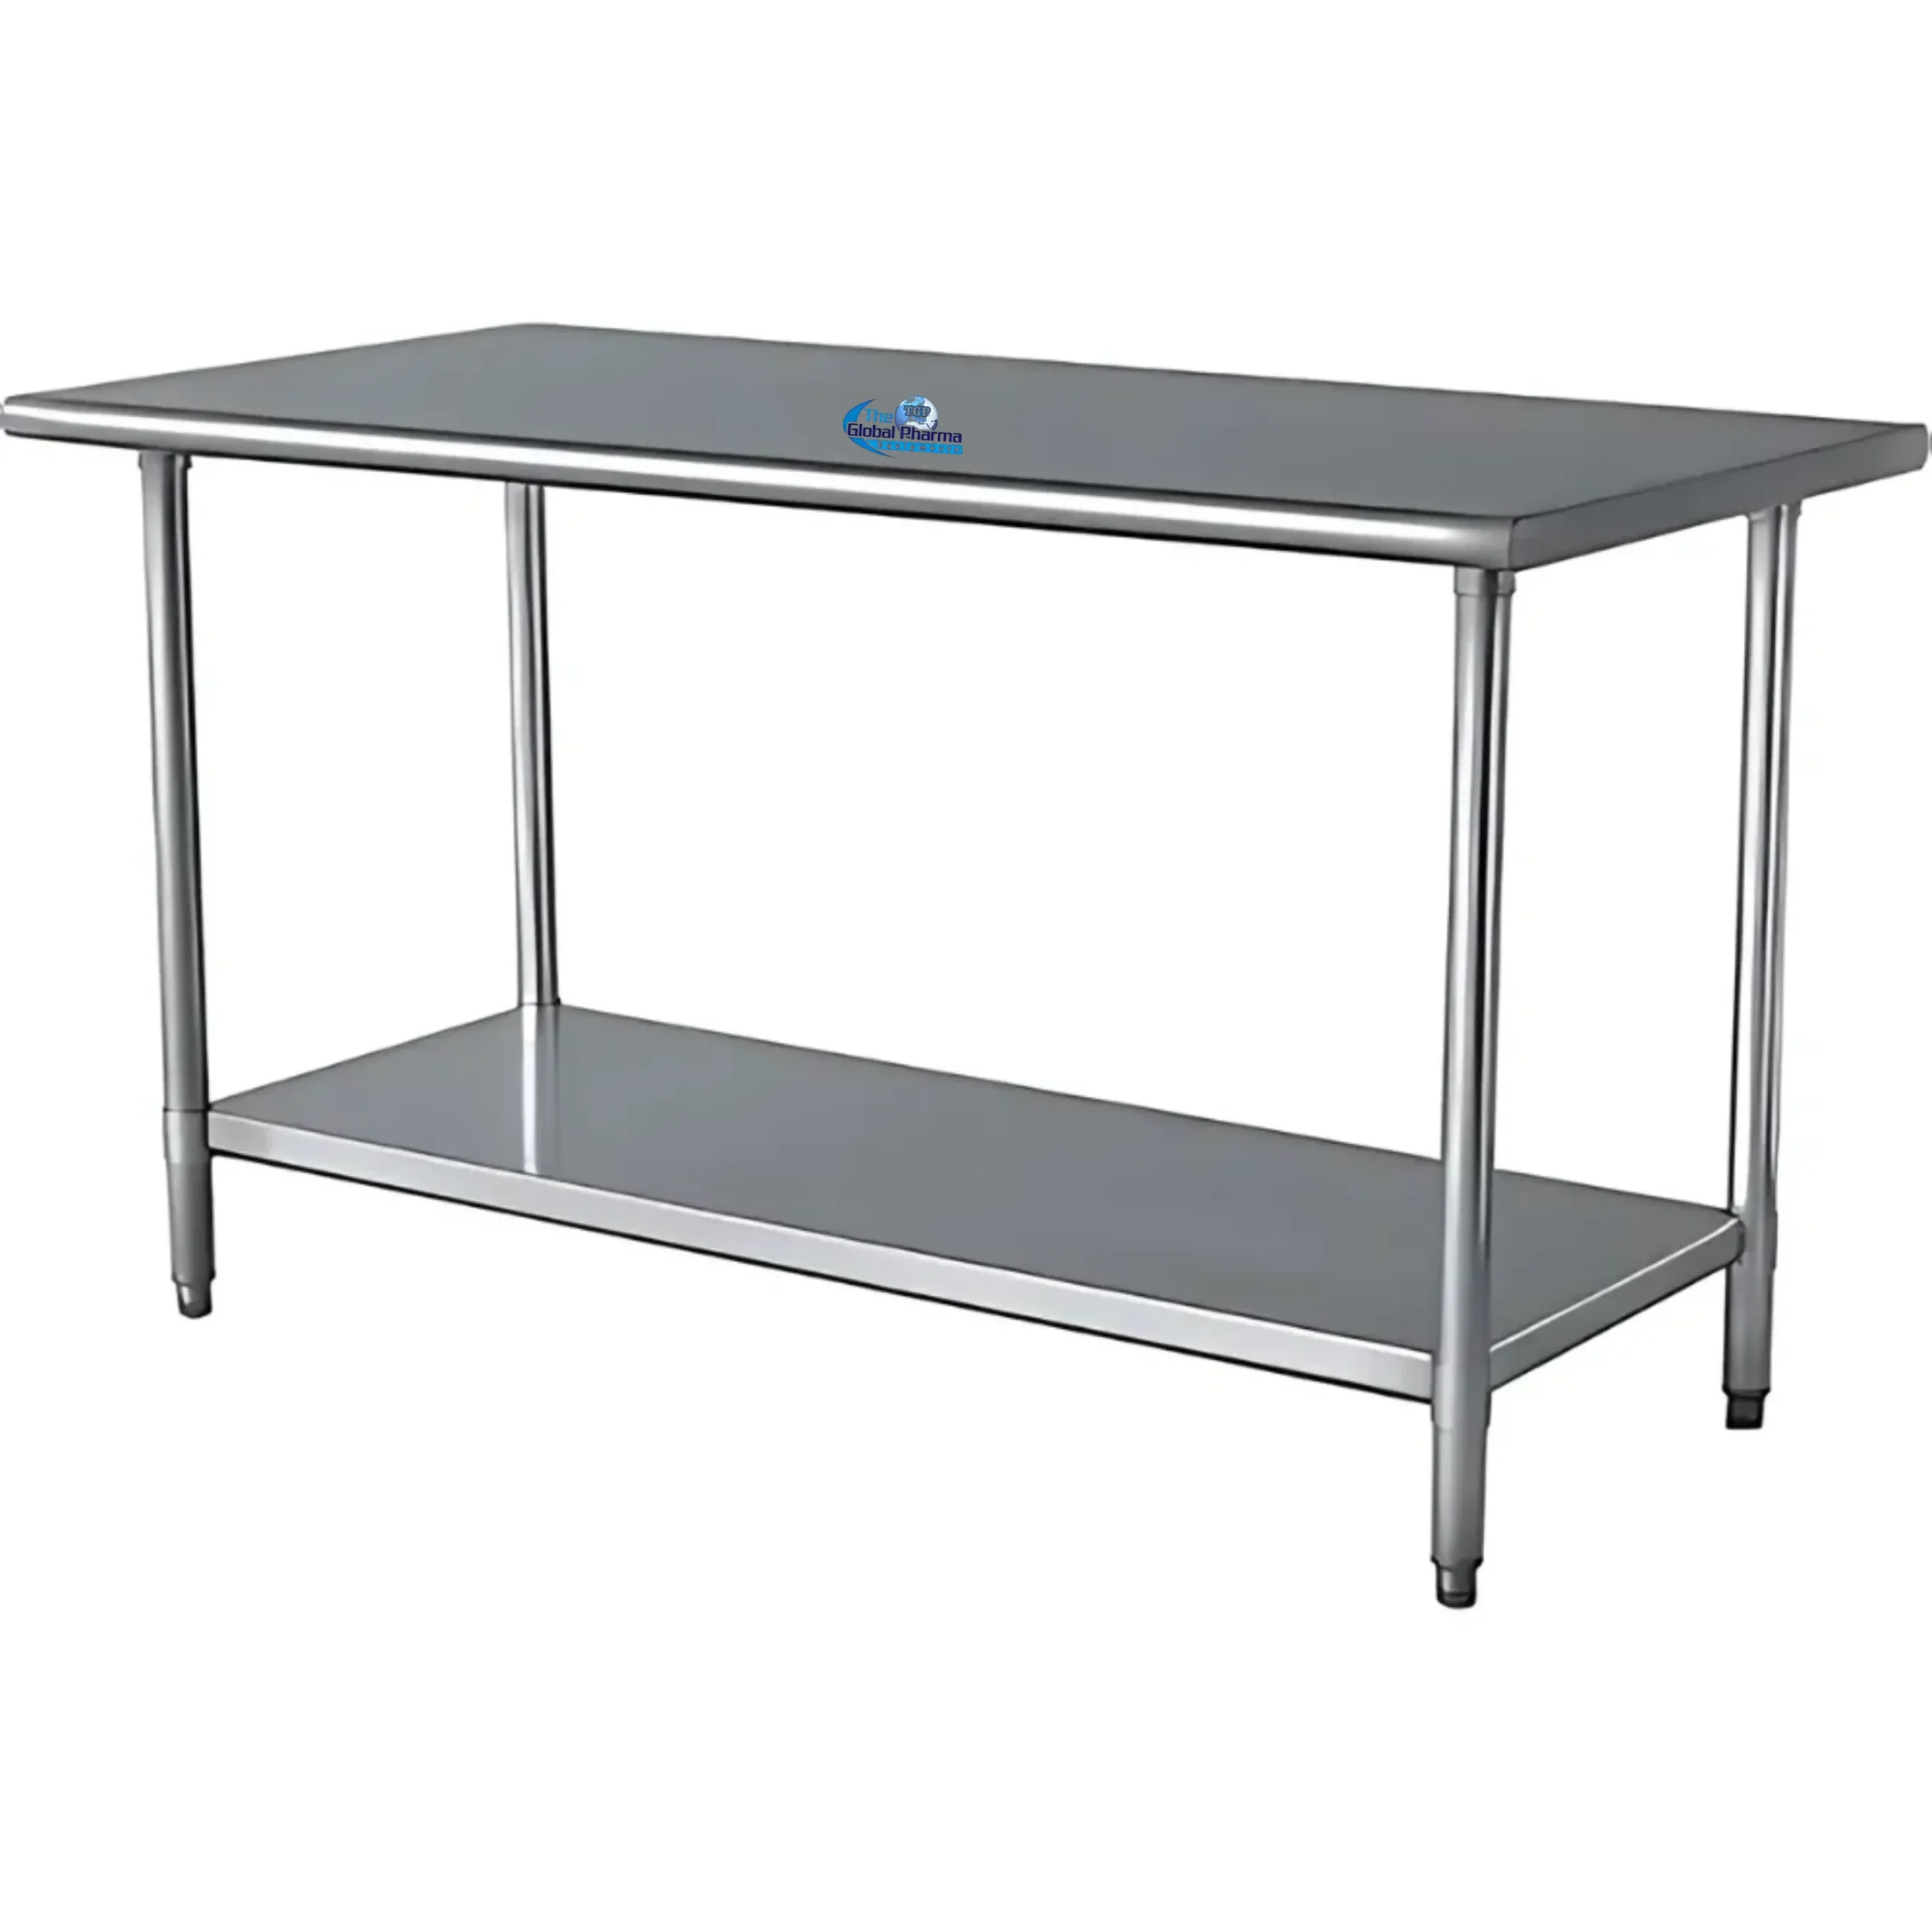
Stainless Steel Work Tables Under Shelf are practical industrial furniture solut...
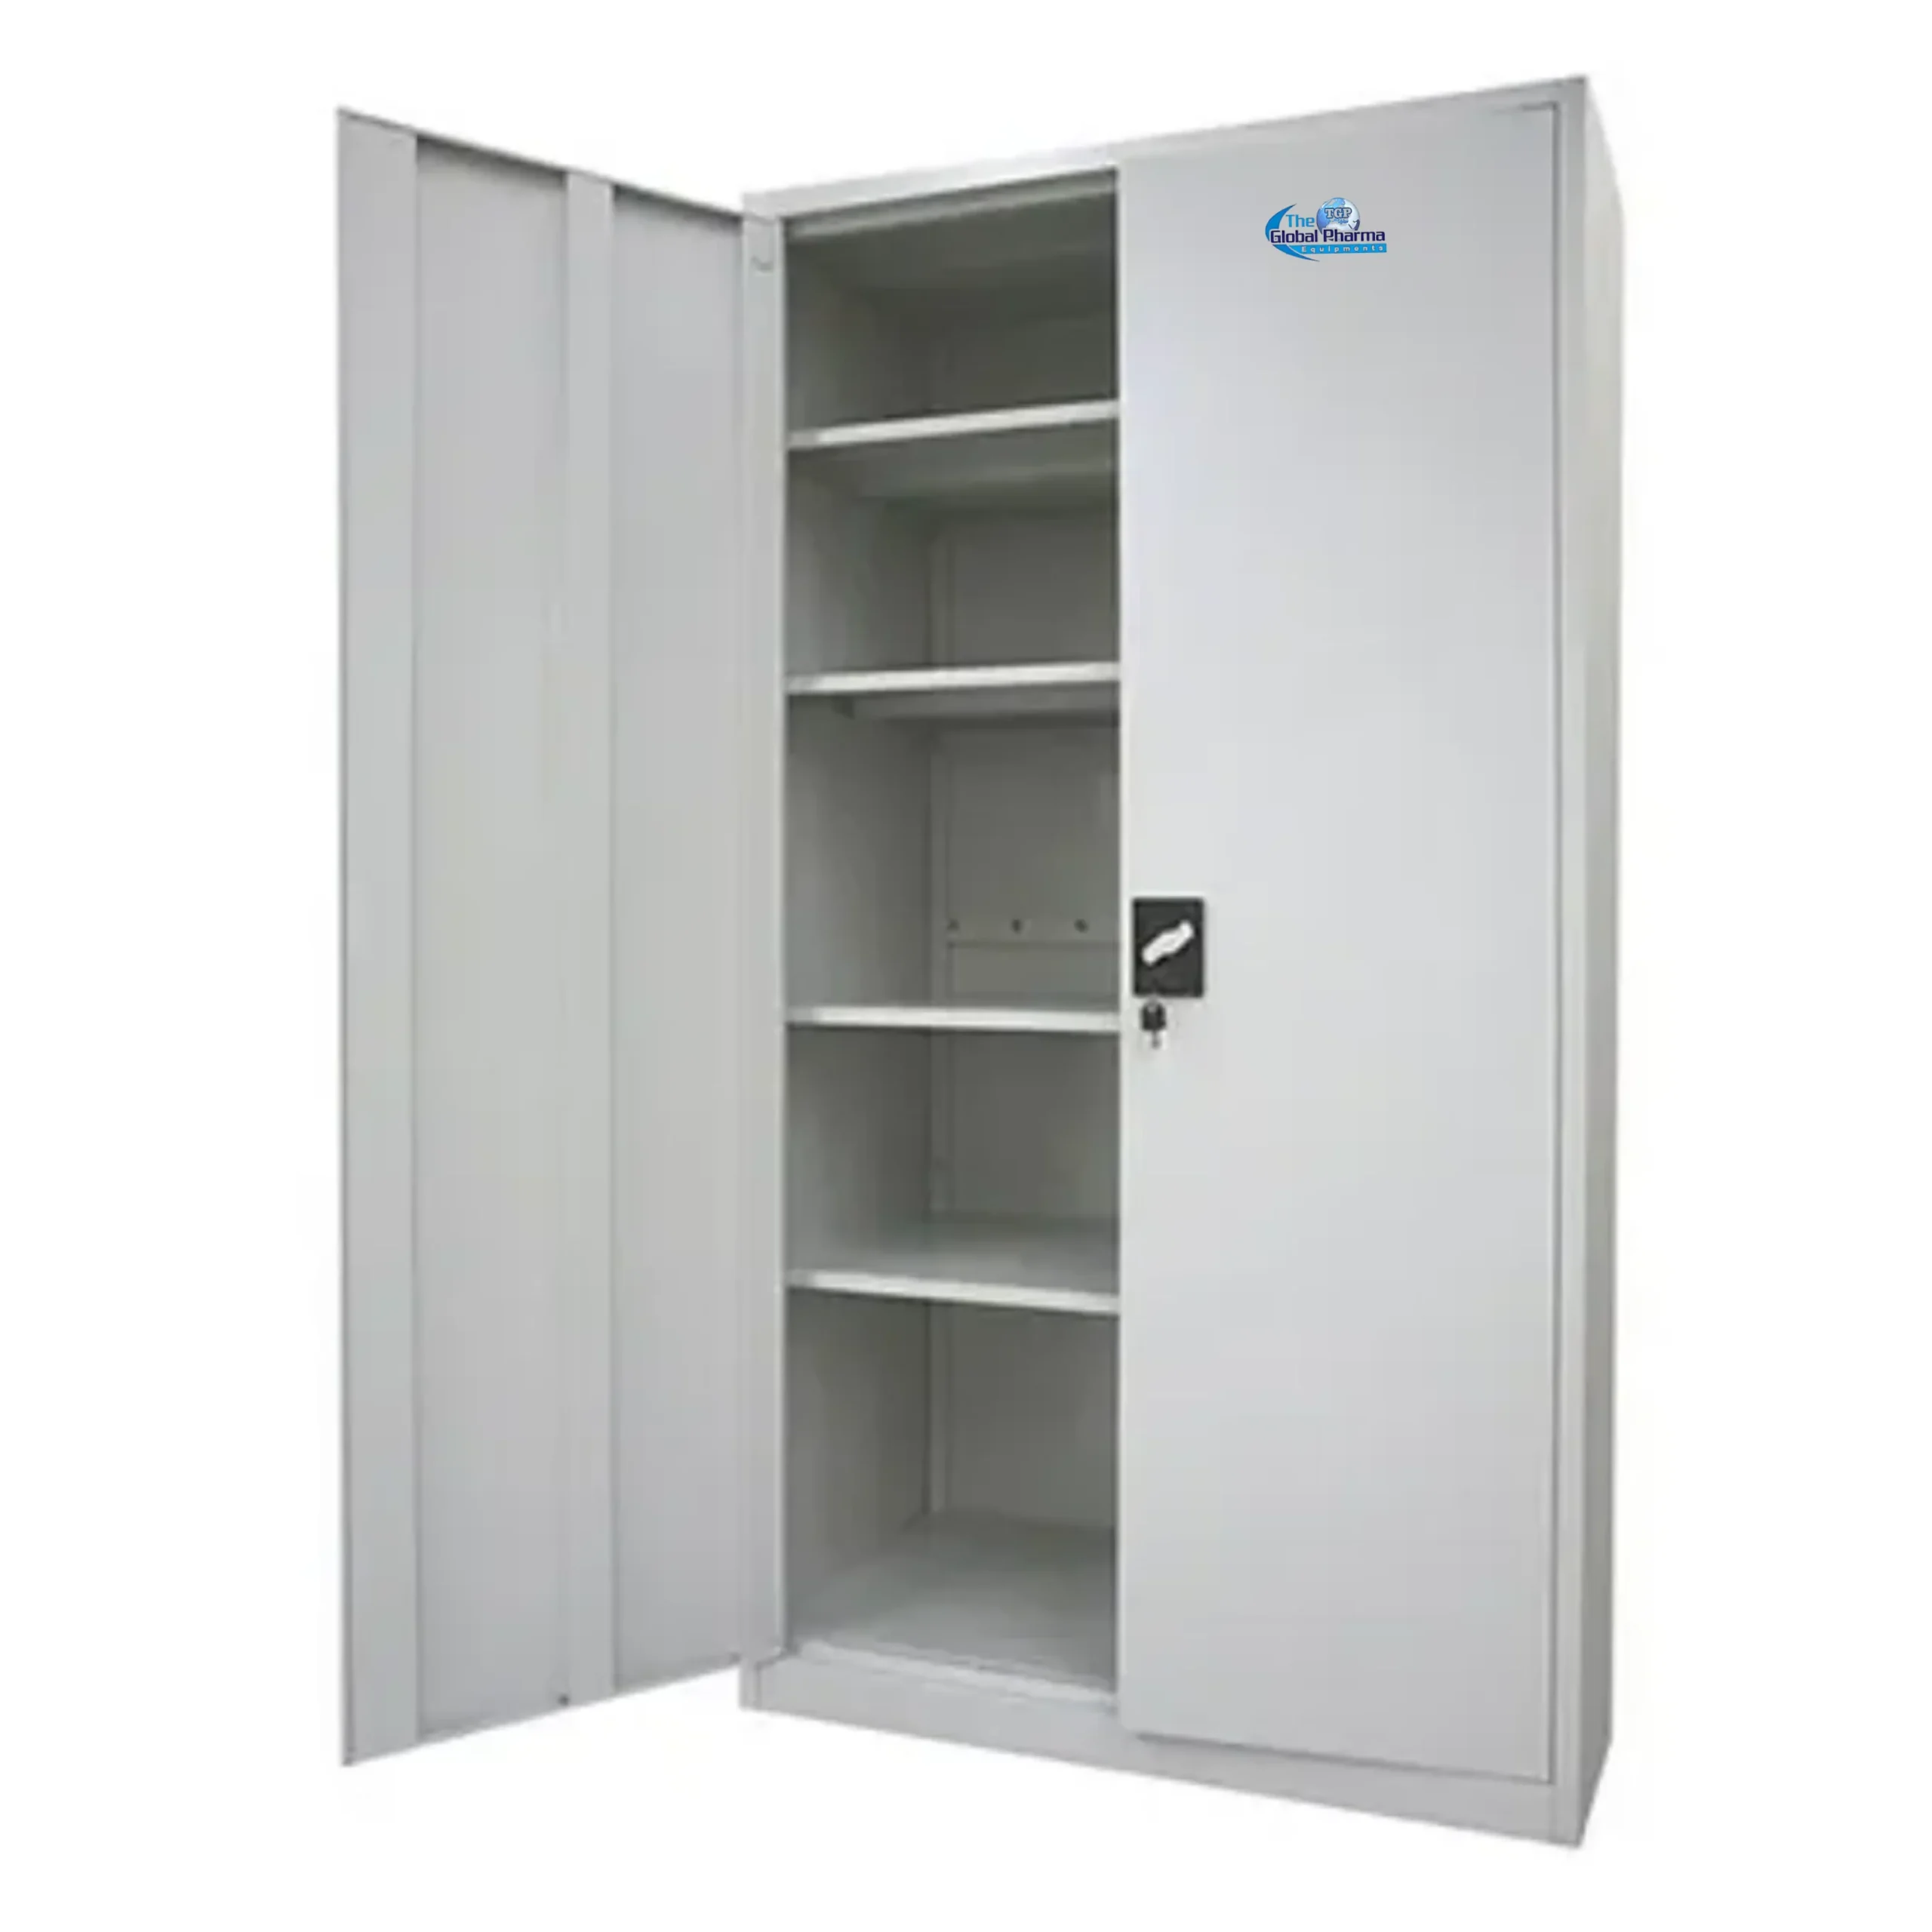
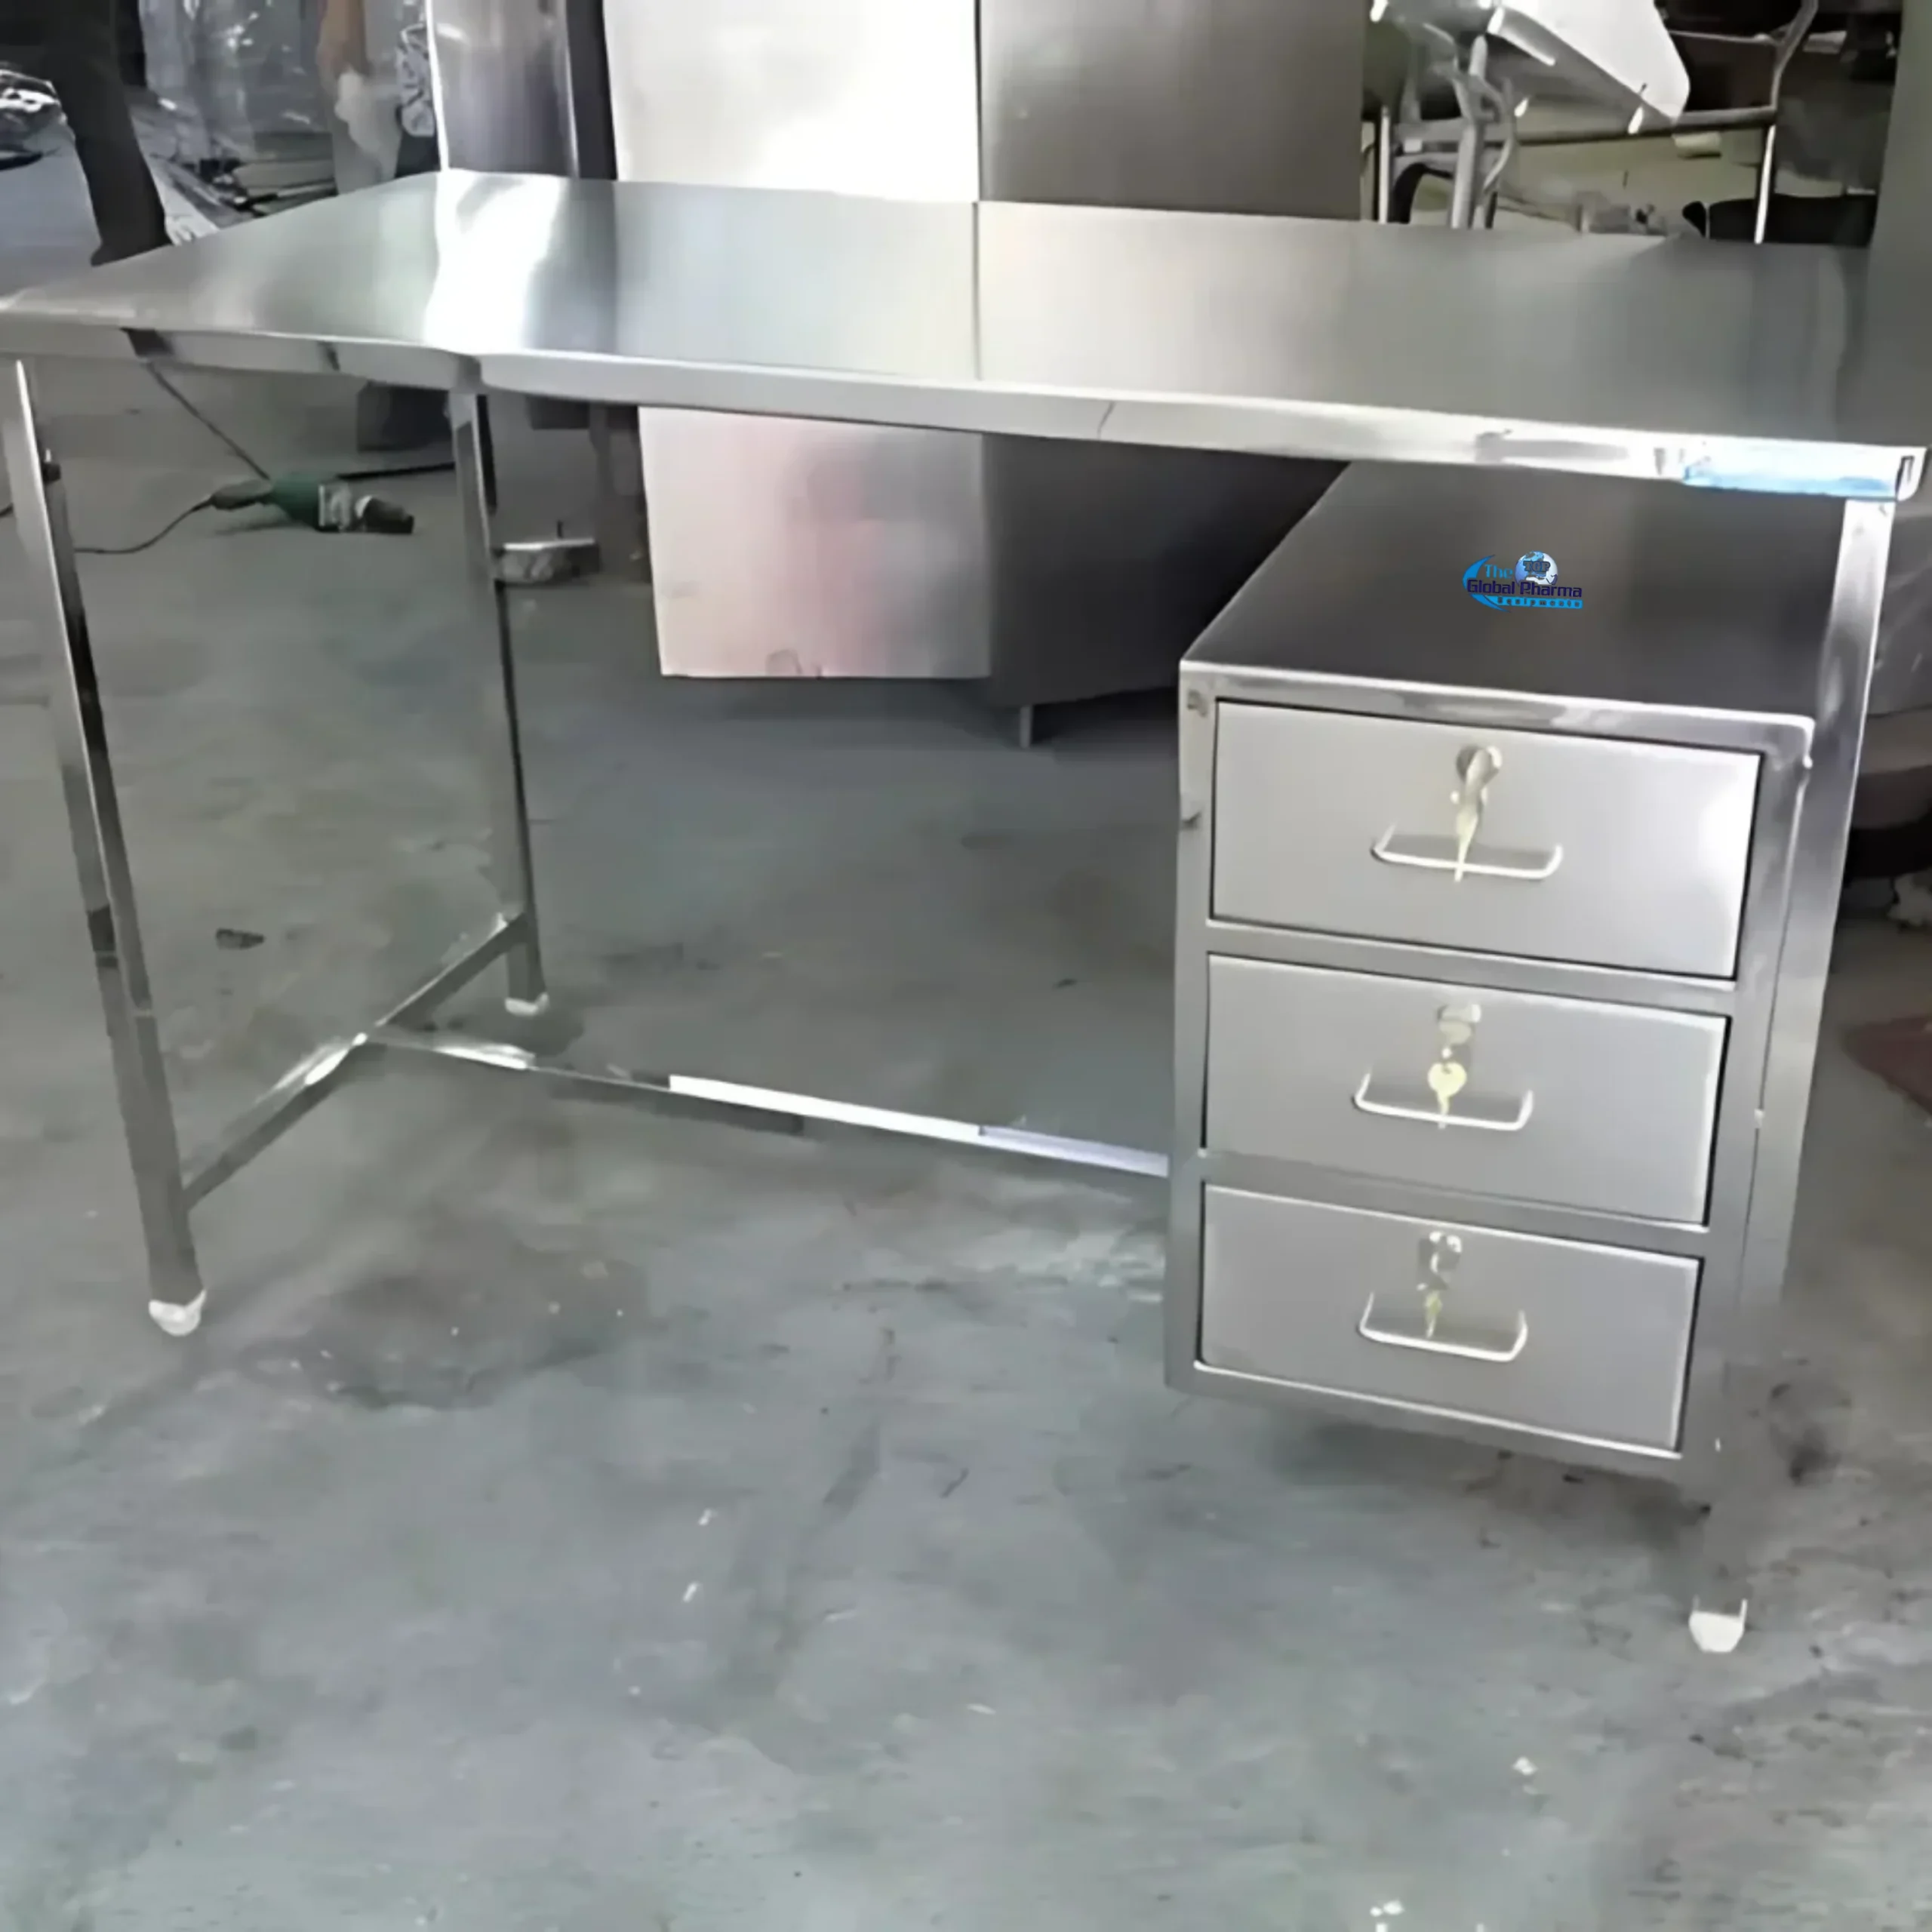
Steel Office Tables are practical workplace furniture solutions designed to prov...

Wall Mount Cabinets are practical storage solutions designed to utilize wall spa...

Warehouse Iron Racks are practical storage systems designed to organize raw mate...
Mild Steel Medicine Cabinets are essential storage equipment designed to keep me...
SS Industrial Trays are versatile stainless steel handling products designed for...
Stainless Steel Medicine Trolleys are essential hospital and pharmaceutical equi...
Pharmaceutical Storage Tanks are essential equipment used for the safe storage o...
Stainless Steel Storage Tanks are widely used for the safe storage of water, che...
Nitrile Oil Seals are widely used as sealing components for preventing the leaka...
Stainless Steel Chemical Mechanical Seals are specialized sealing components des...
Viton Oil Seals are high-performance sealing components designed to prevent lubr...
Pharma Storage Containers are specially designed for the safe storage, handling,...
Stainless steel buckets are widely used for storing, handling, transferring, and...
Stainless steel containers are widely used for the safe storage, handling, and t...

Stainless Steel IPC Trolleys are specialized material handling solutions designe...
Stainless Steel Storage Buckets are widely used for storing, handling, and trans...
Clean Room Pass Boxes are essential cleanroom equipment designed to transfer mat...
SS static pass boxes are important cleanroom equipment used for transferring mat...